Finishing Options

Explore OSH Cut's wide range of metal finishing services.
Bead Blasting

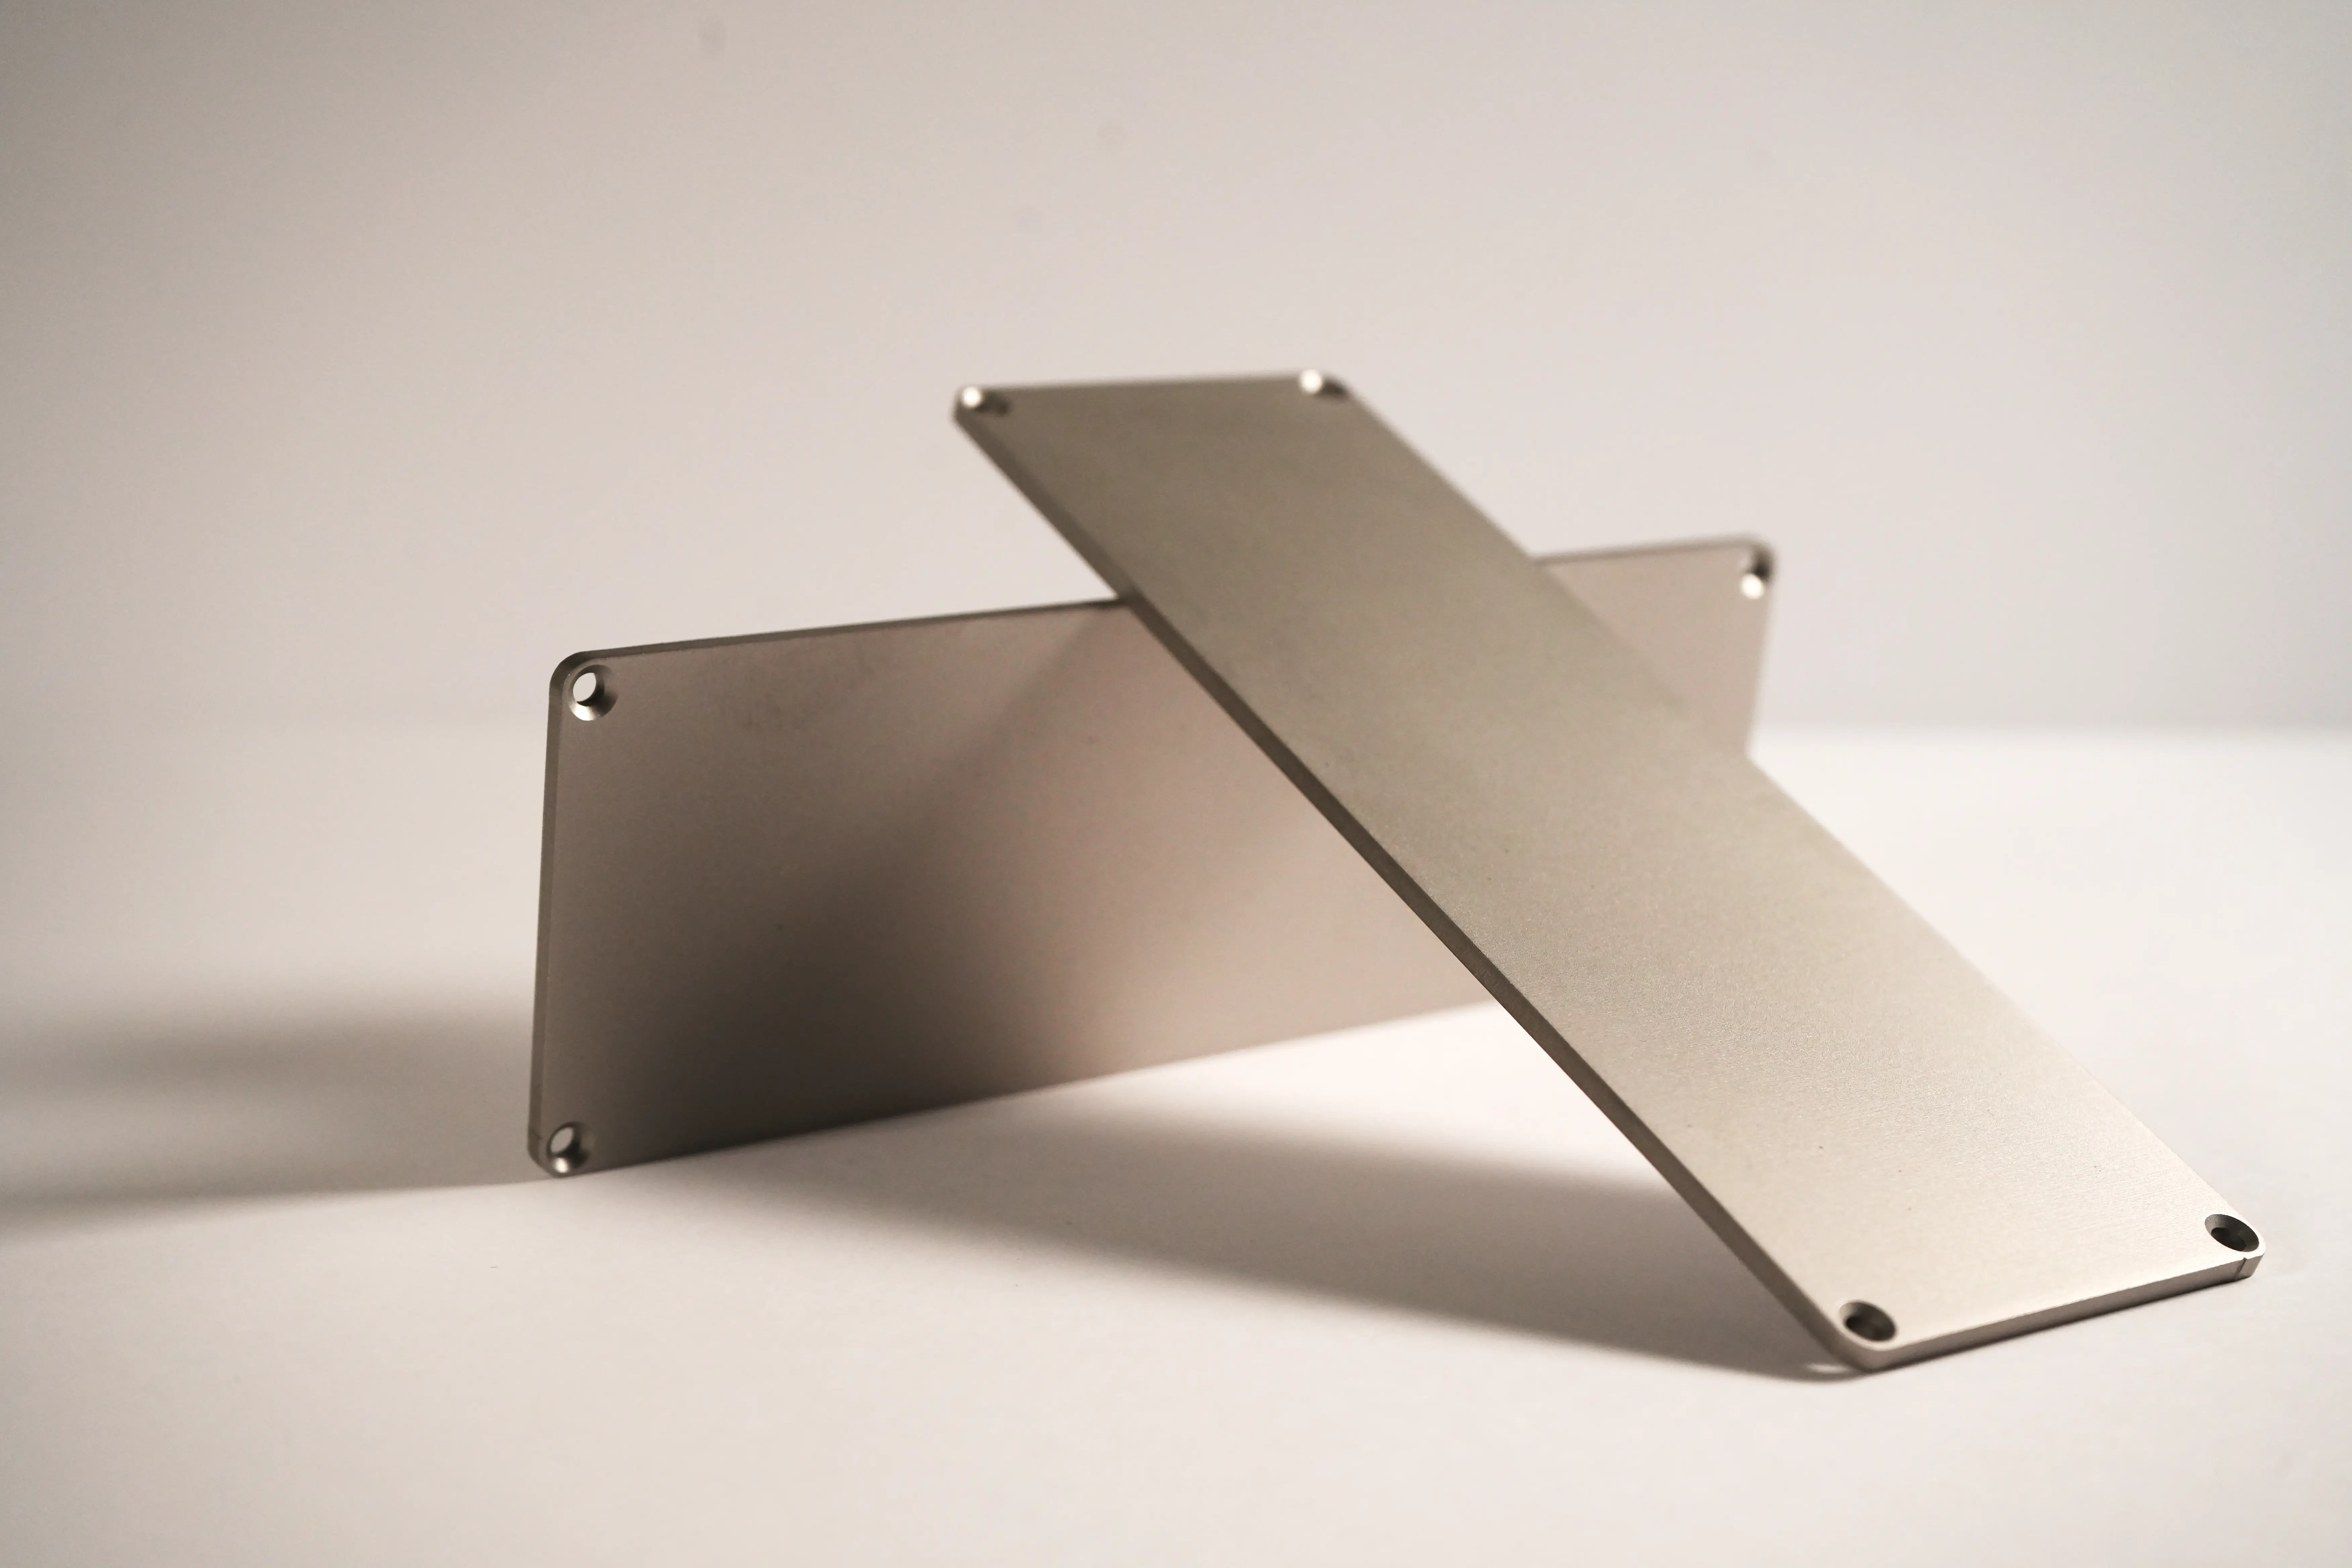
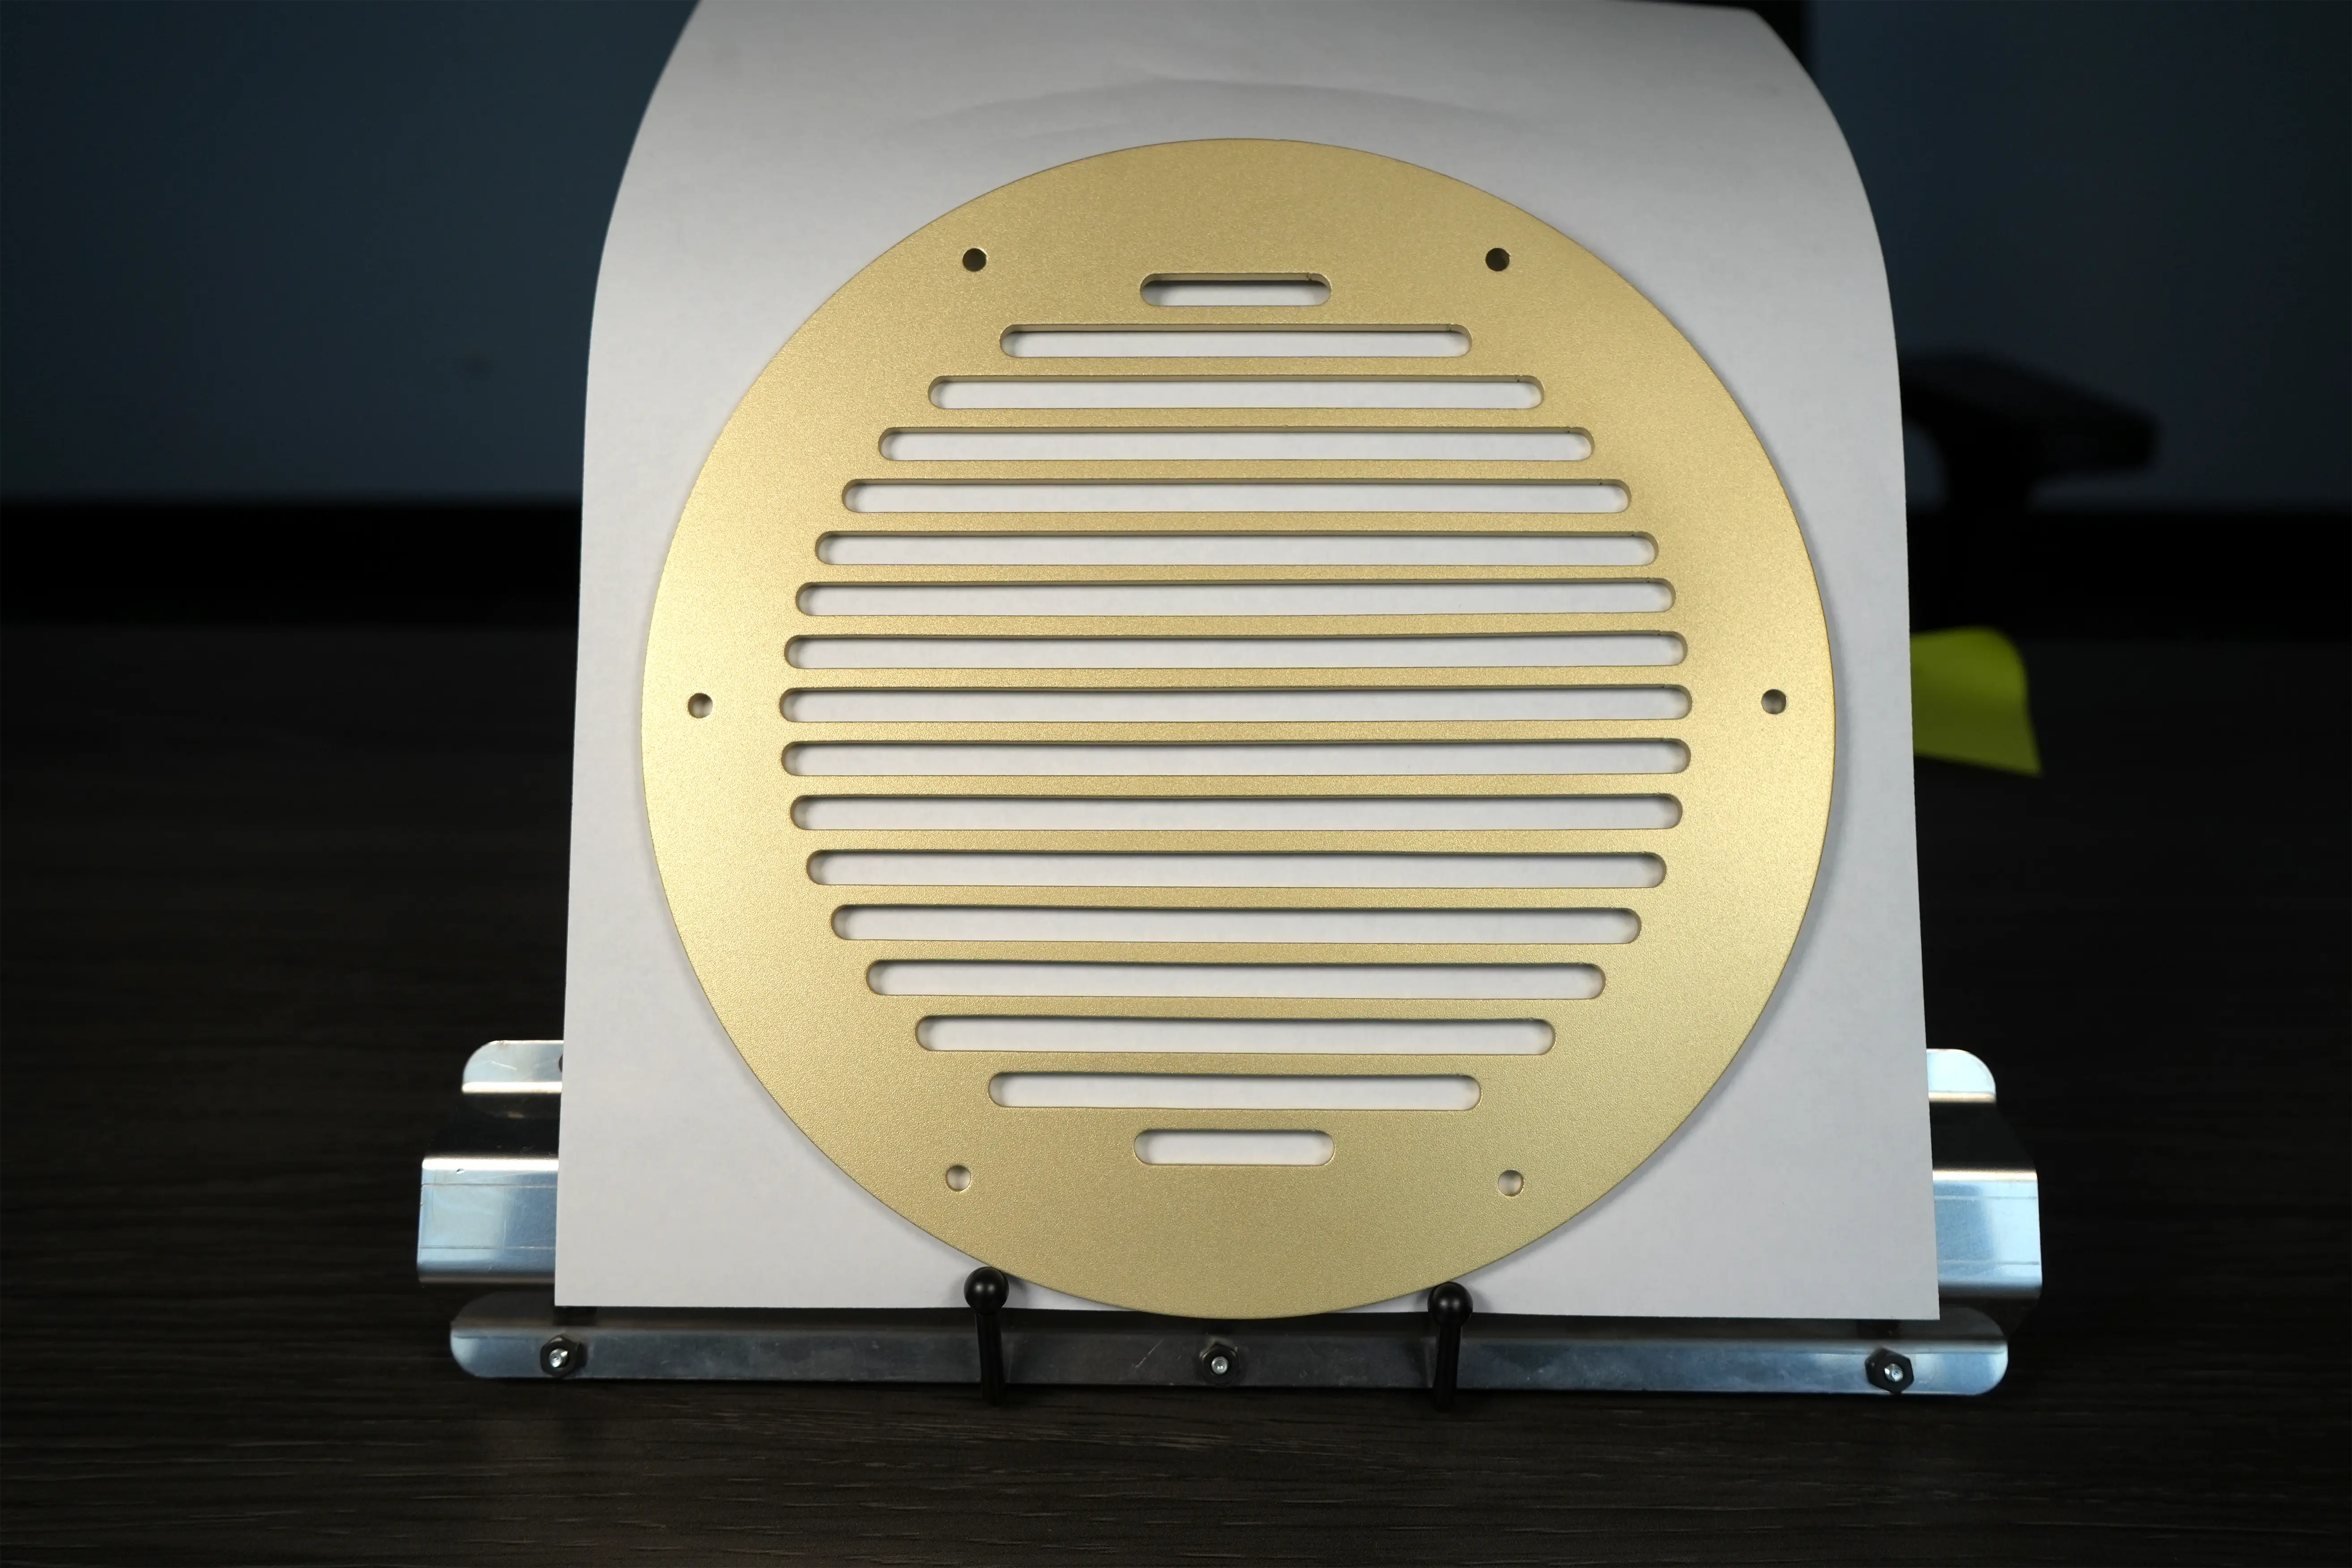
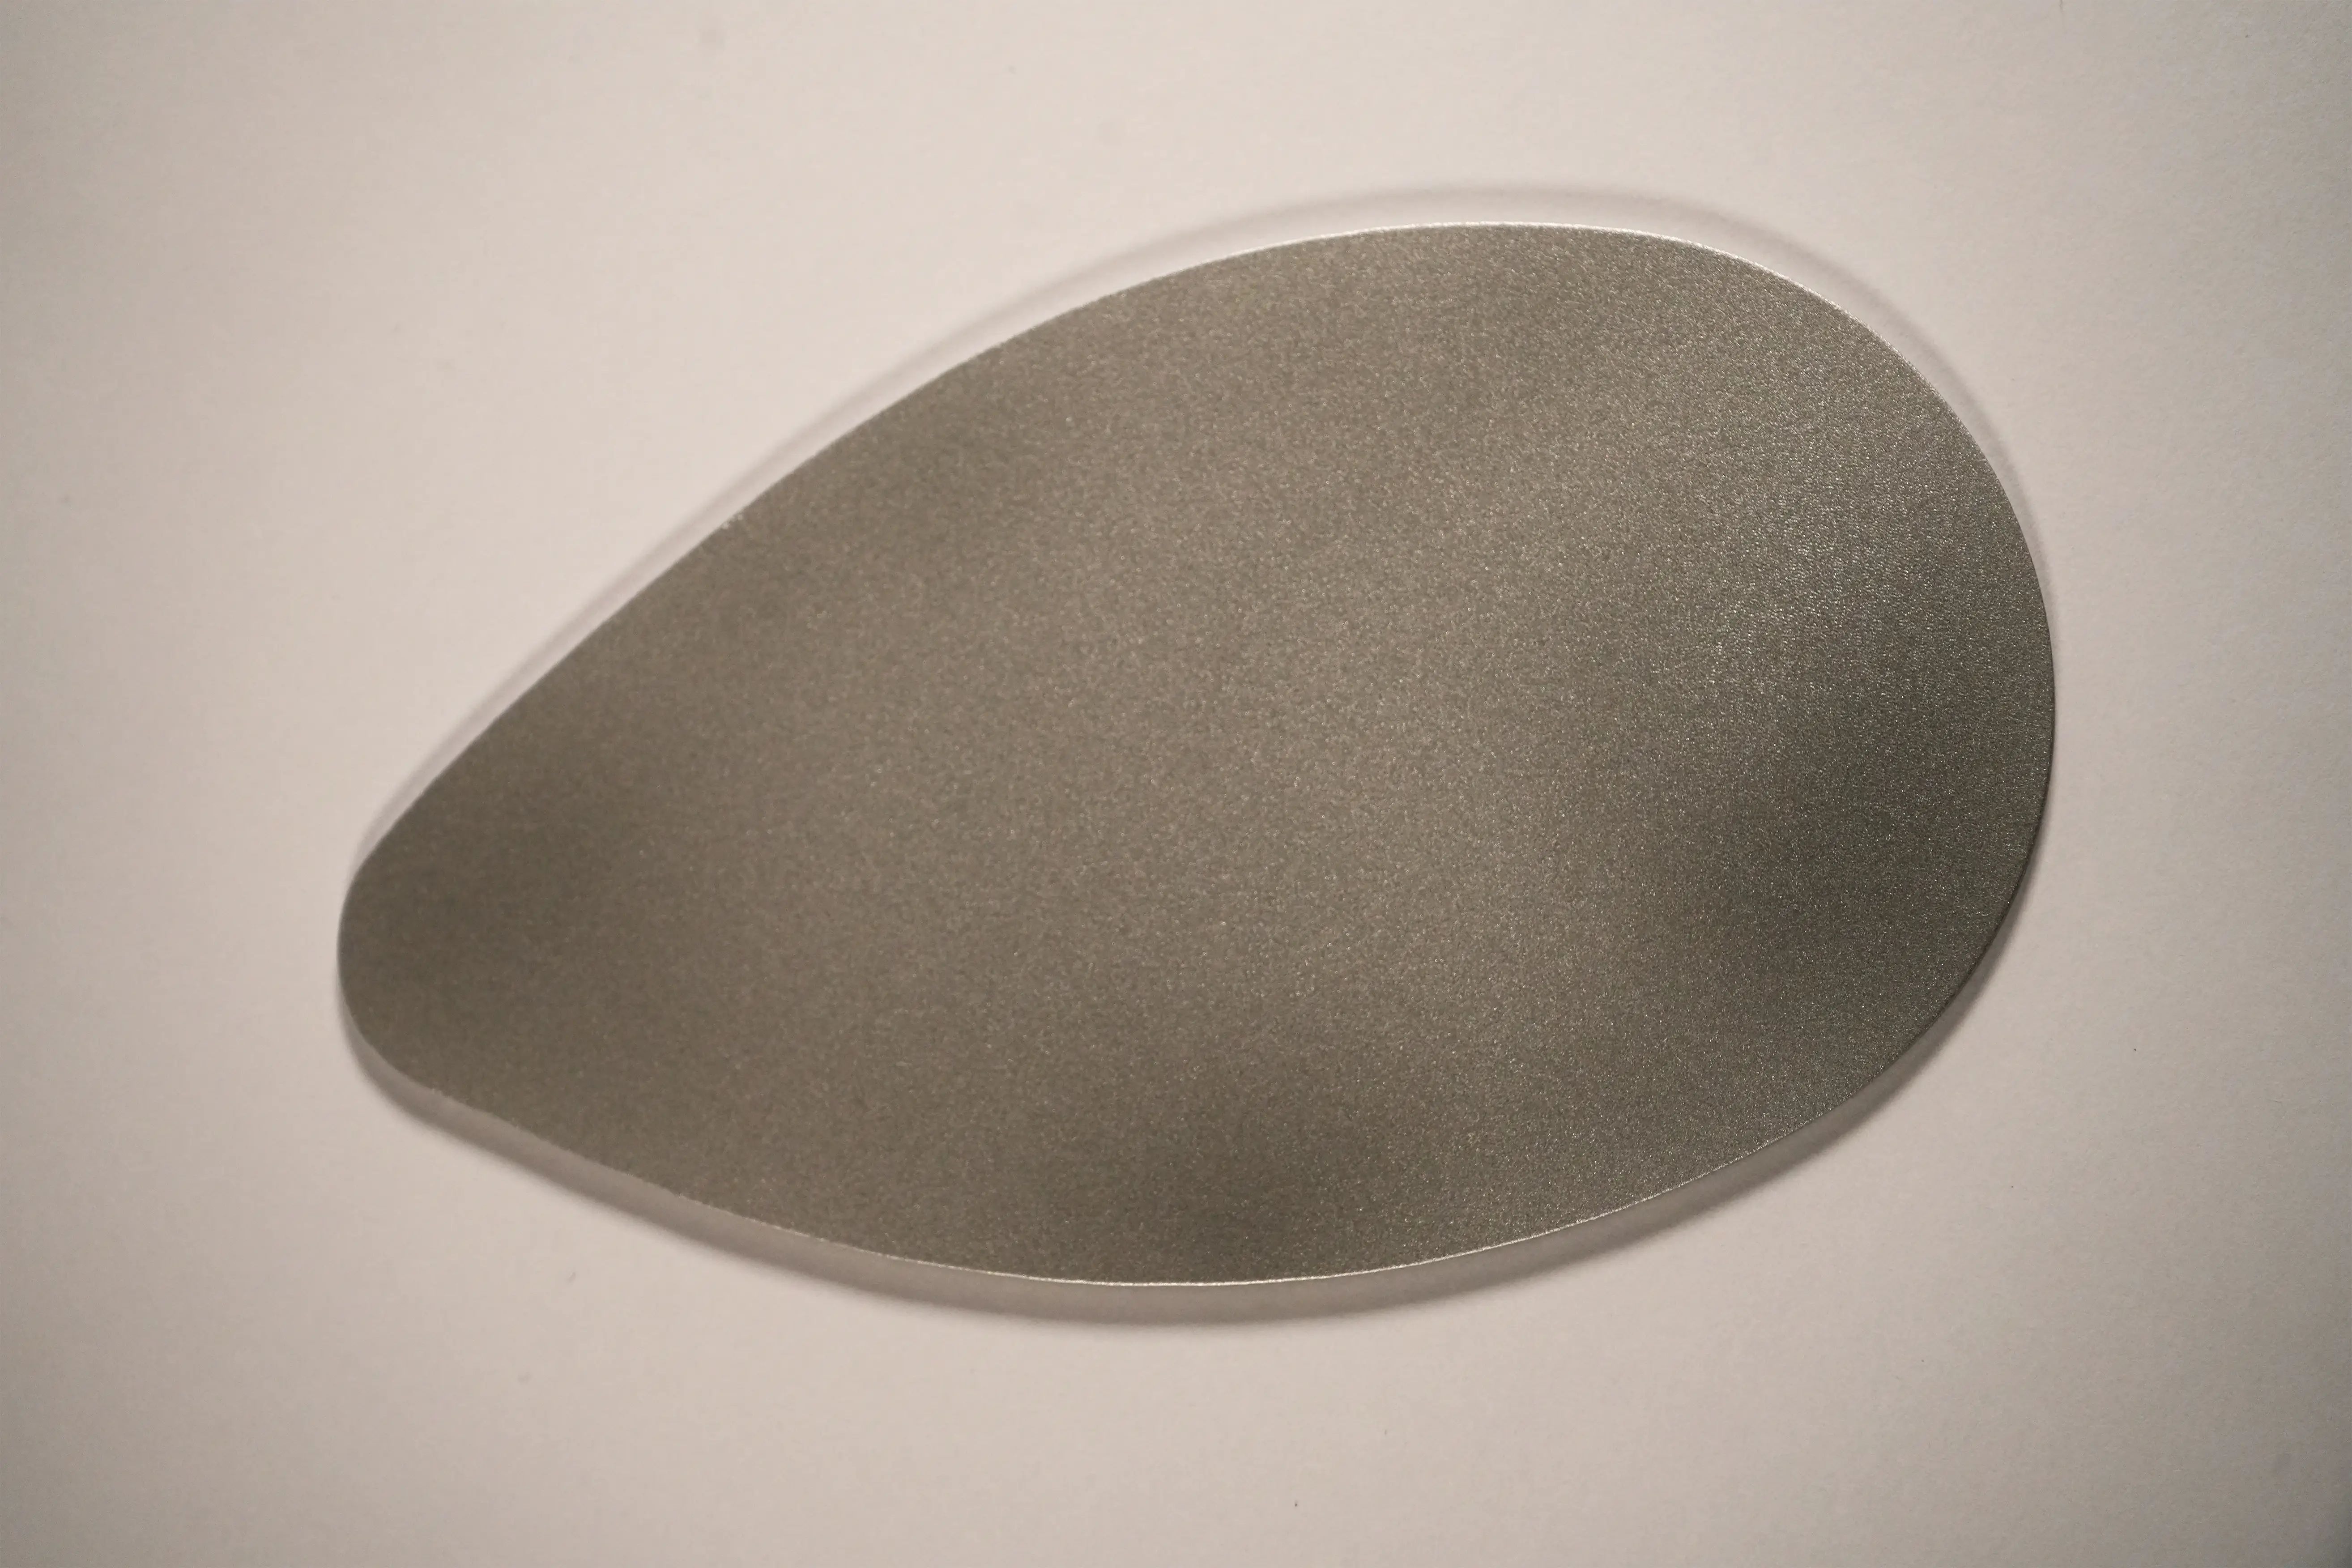
Bead blasting propels fine glass beads at high pressure to clean and texture the surface of a metal part. This process removes laser cutting discoloration and produces a smooth matte appearance.
Bead blasting is a surface finishing process that uses compressed air to propel fine glass beads against the surface of a part. The beads gently impact the material, removing discoloration, oxidation, and minor surface imperfections left from the cutting process. This creates a smooth, consistent matte finish that improves the cosmetic appearance of the part without significantly affecting its dimensions. Bead blasting is commonly used on aluminum and stainless steel parts where a clean and professional appearance is desired.
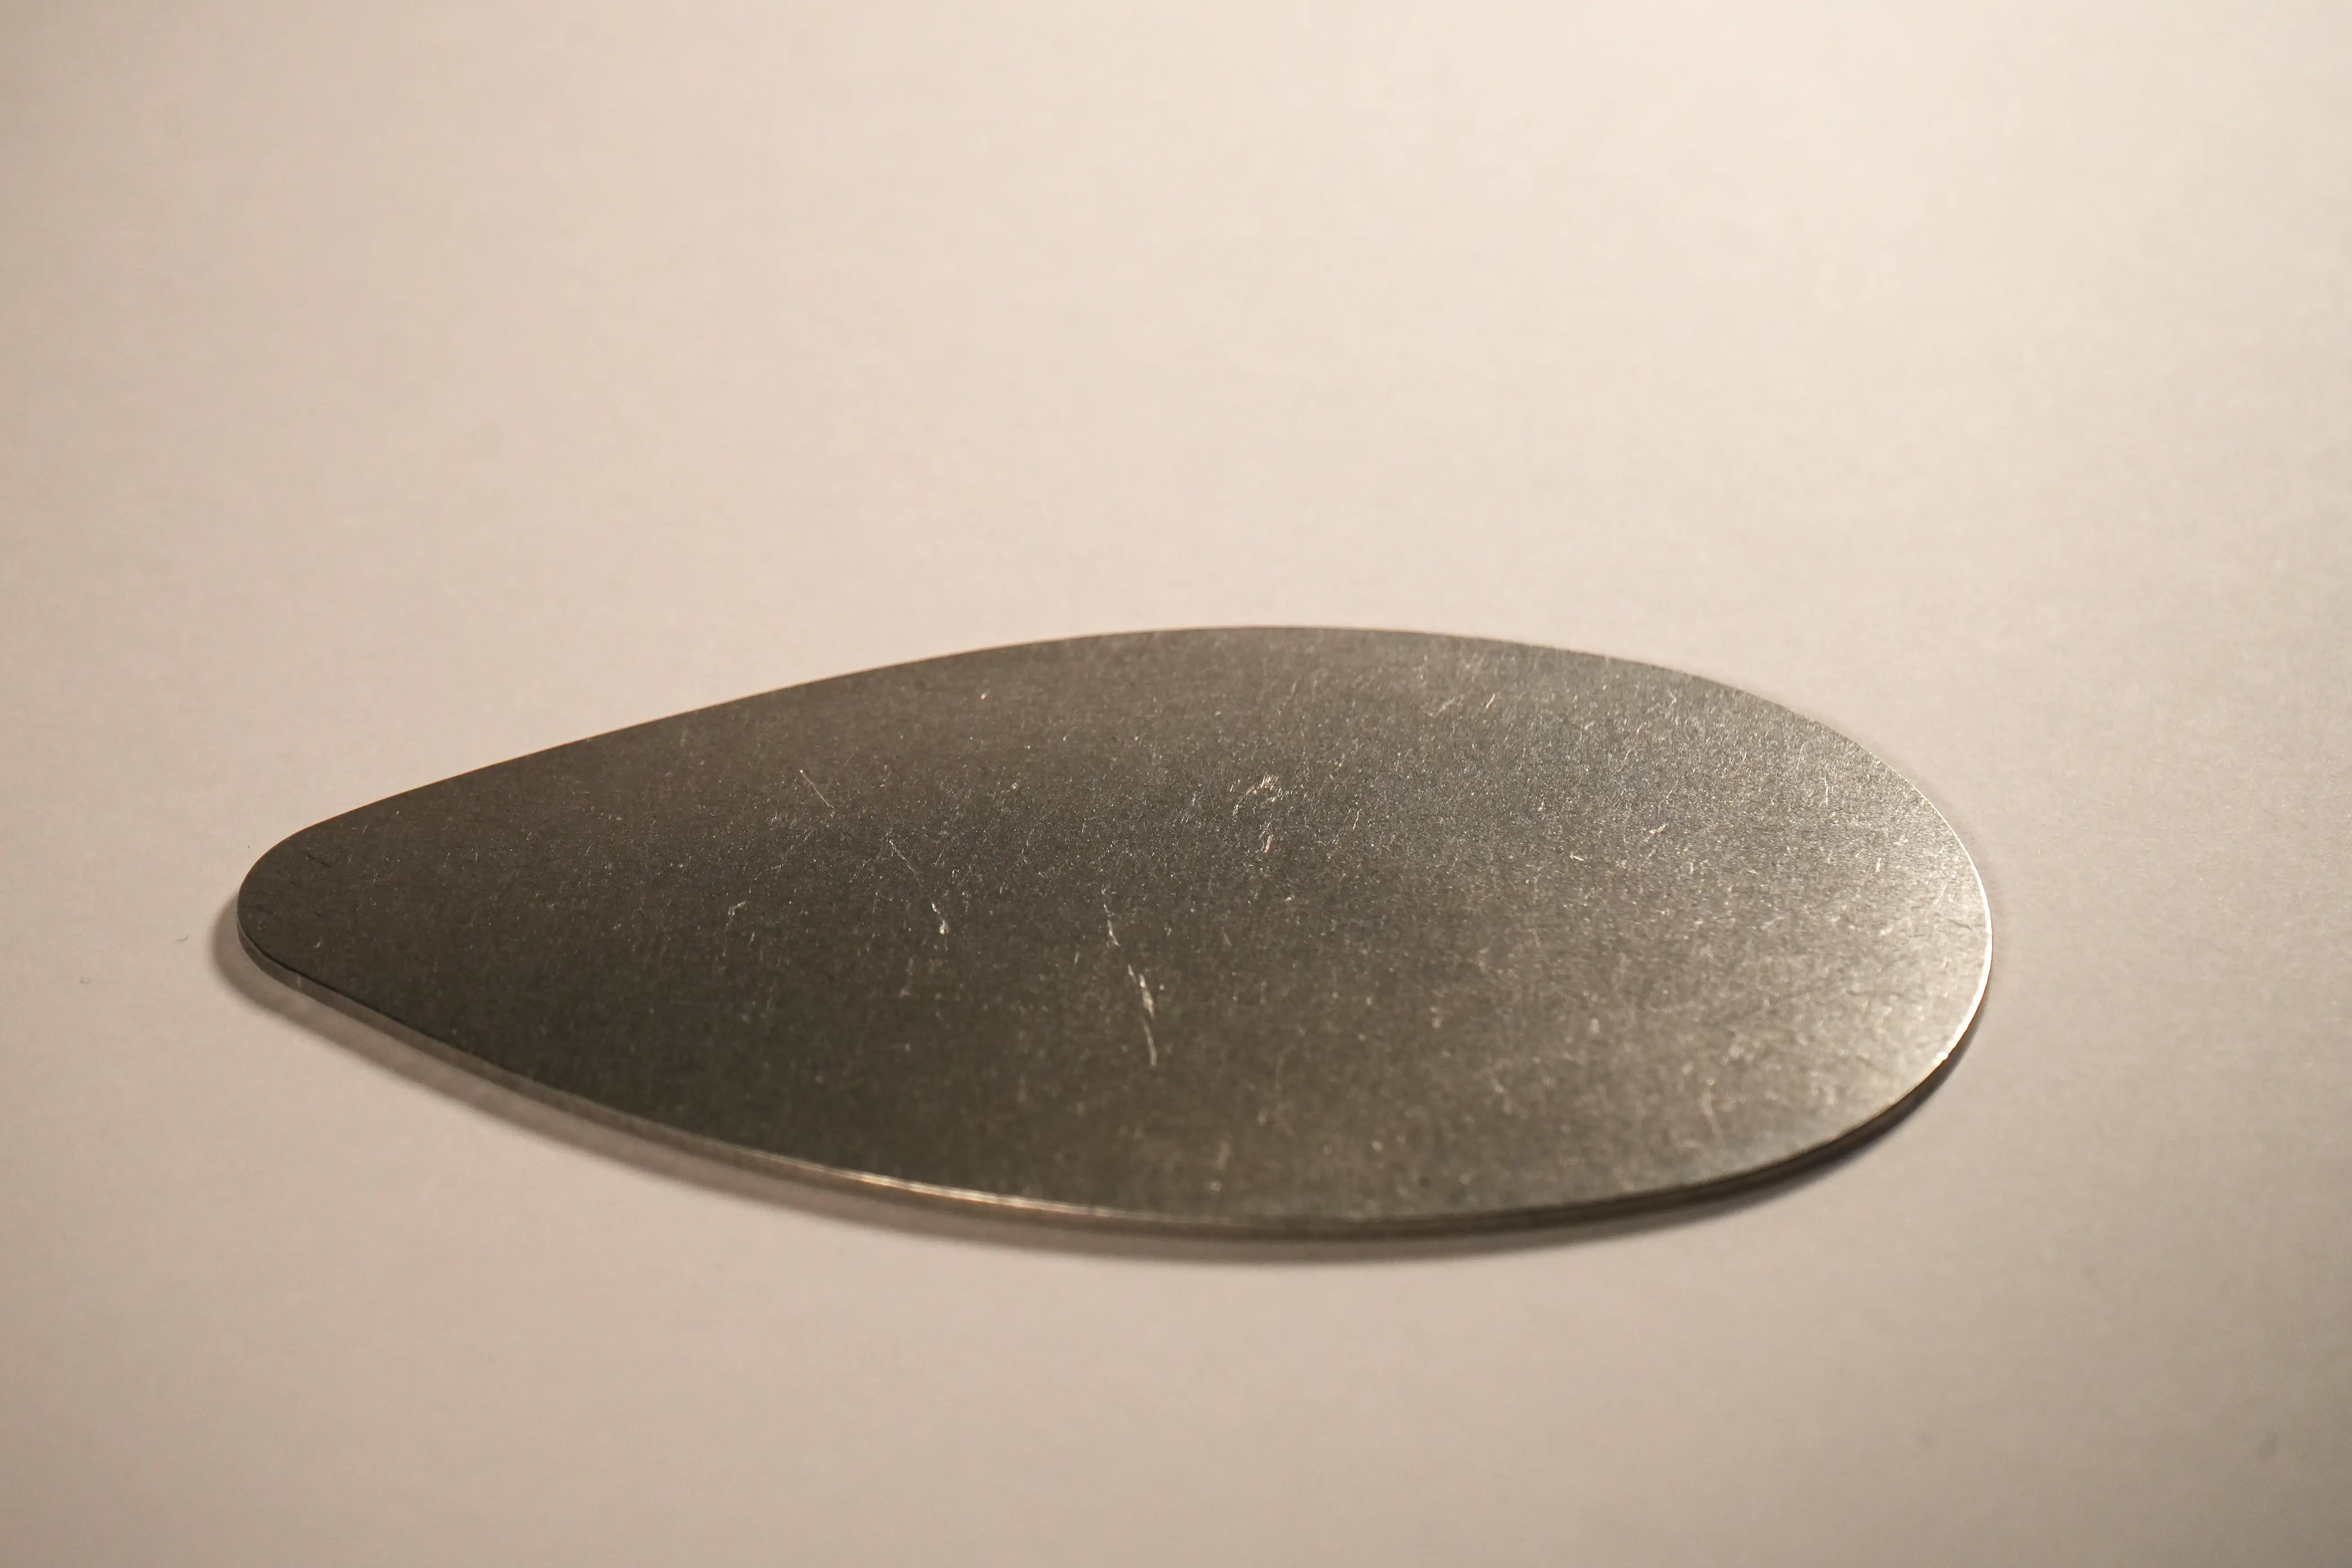
Two bead blasted rectangular metal plates leaning against each otherBead blasted brass grille plate with rows of slotsTeardrop-shaped metal part with a bead blasted matte finish

Before and After

Before bead blasting, metal parts may show visible cutting marks, oxidation, or discoloration caused by the laser cutting process. The surface can appear uneven or reflective depending on the material. After bead blasting, the surface becomes a consistent matte texture with a smooth, uniform appearance. The process evens out the visual finish and removes most cutting marks and discoloration.

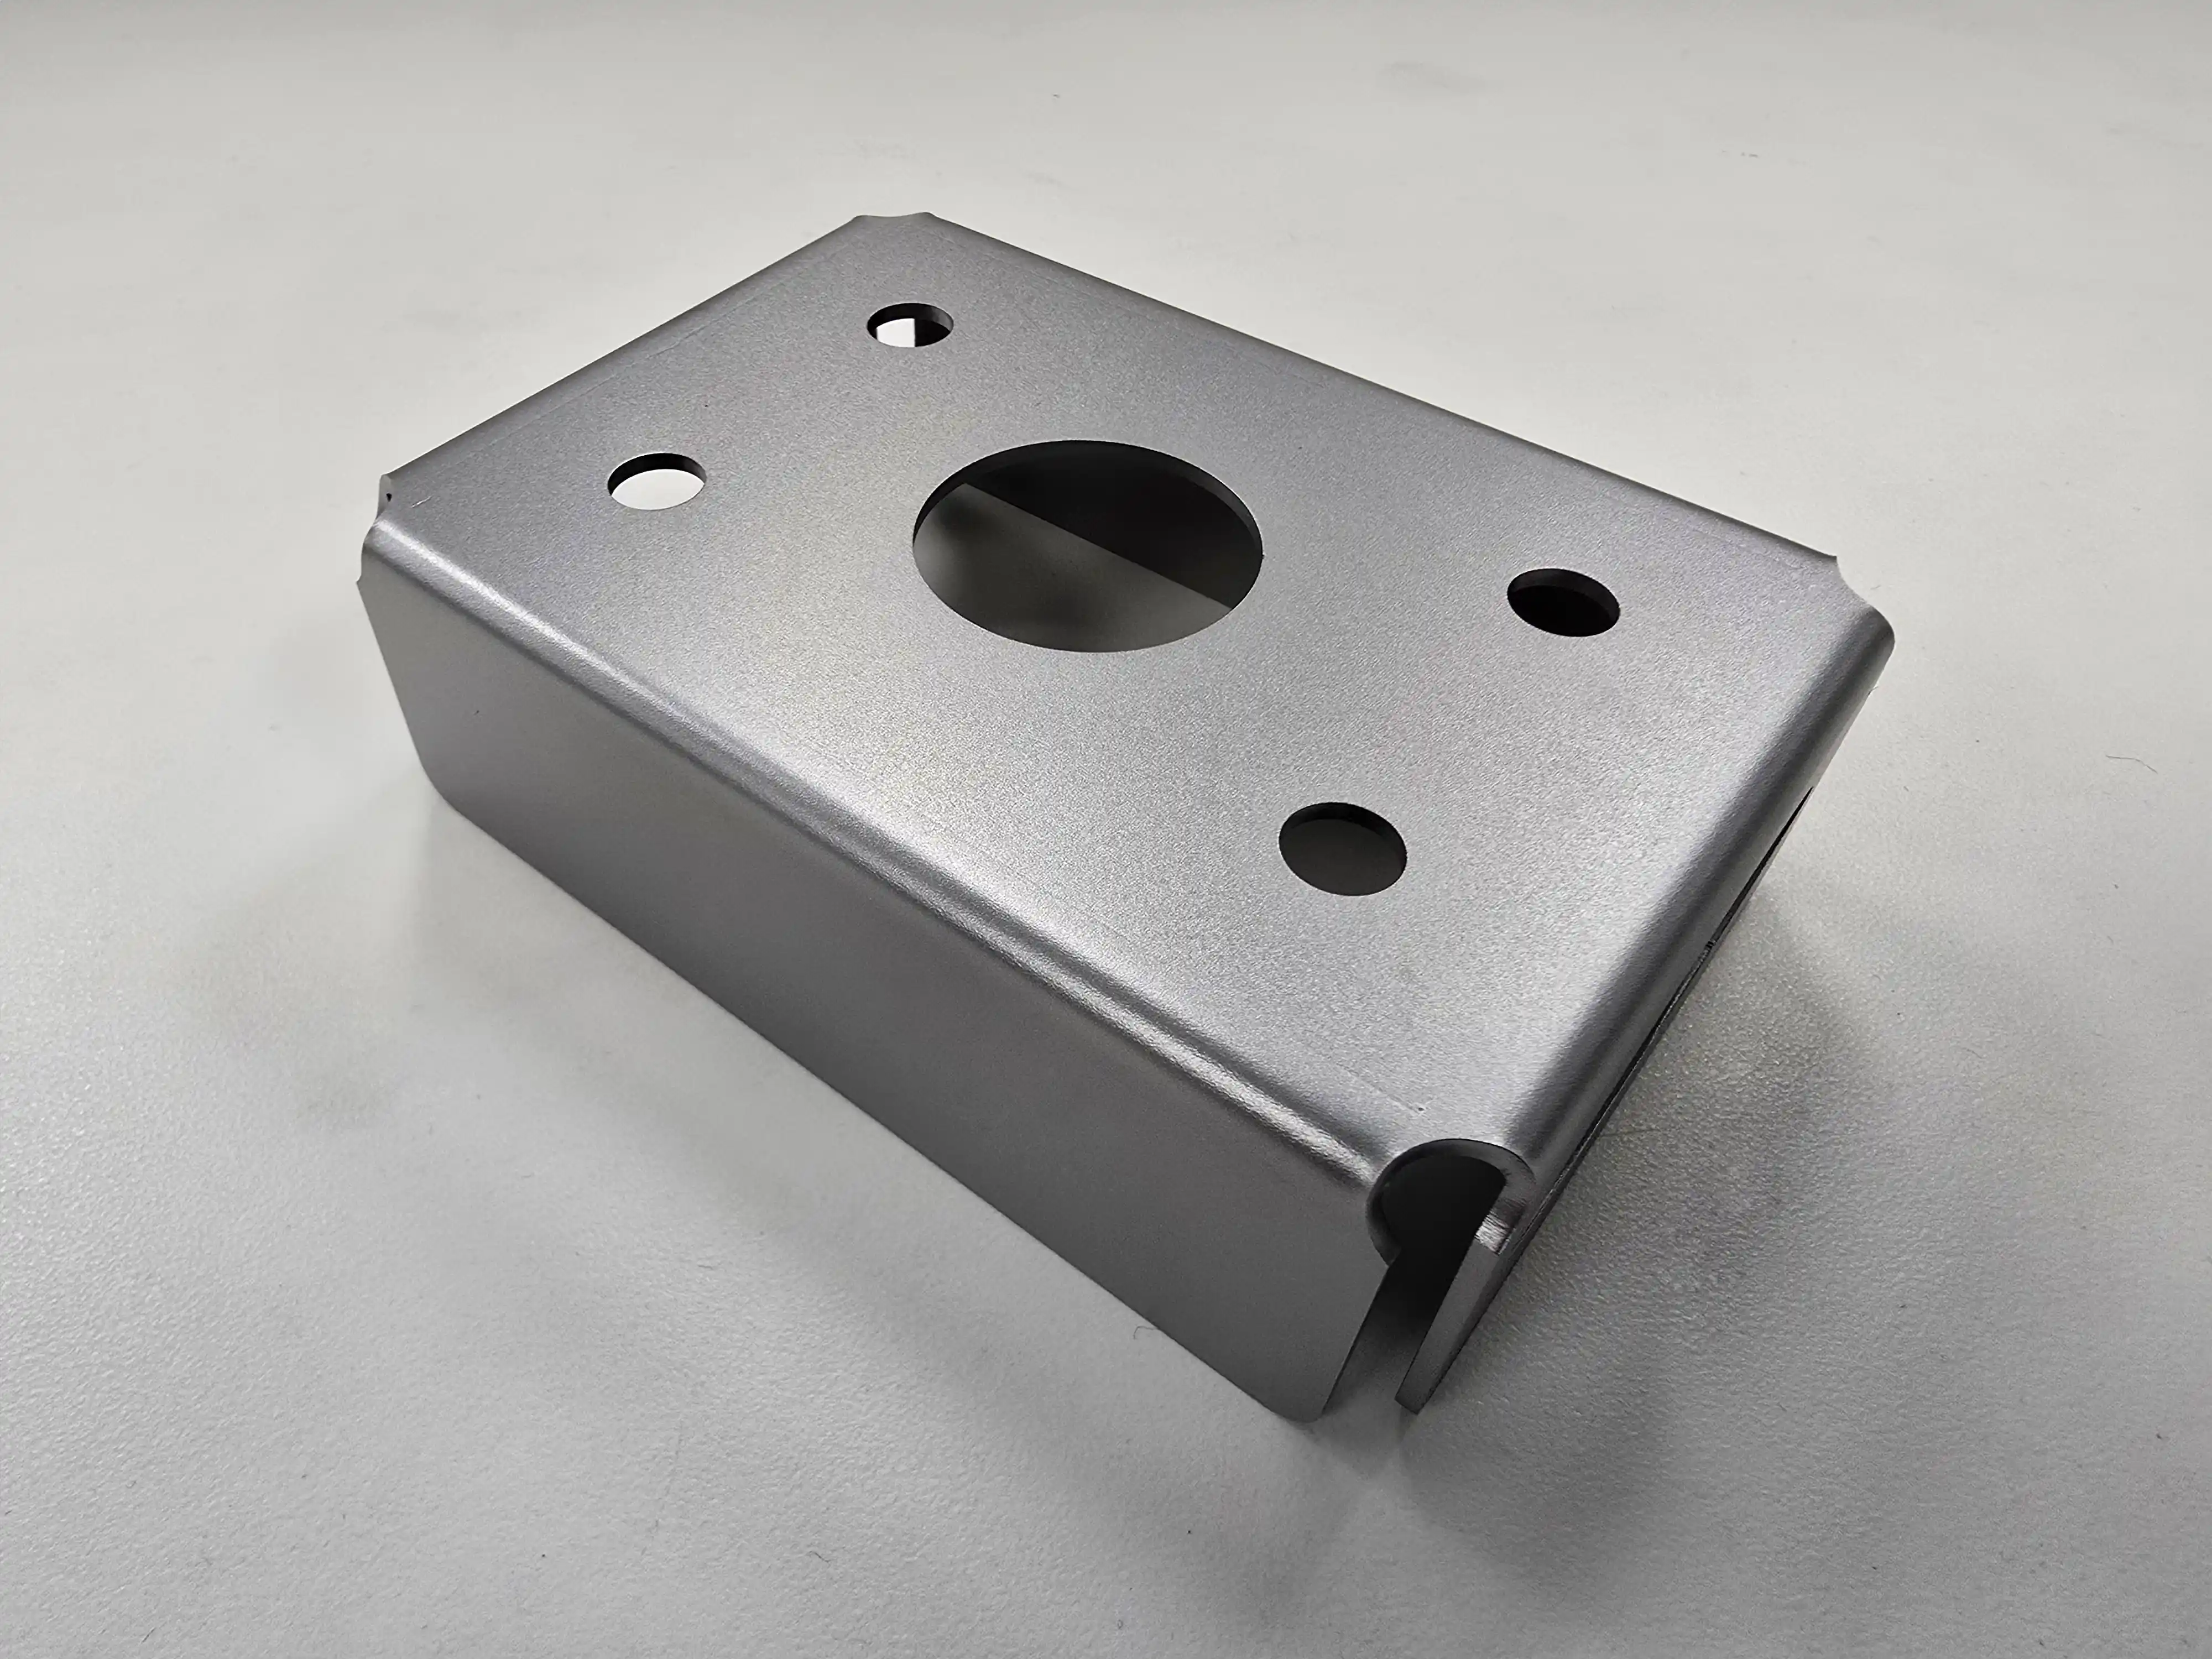
Bent steel bracket before bead blastingThe same bracket after bead blasting, with an even matte finish

Best Practices for Success

Bead blasting can be applied to most metals and part geometries. However, tight internal corners, deep pockets, and small recessed features may not receive the same level of finishing because the blasting media cannot reach them directly. Masking may be required for areas where the original surface finish must be preserved.
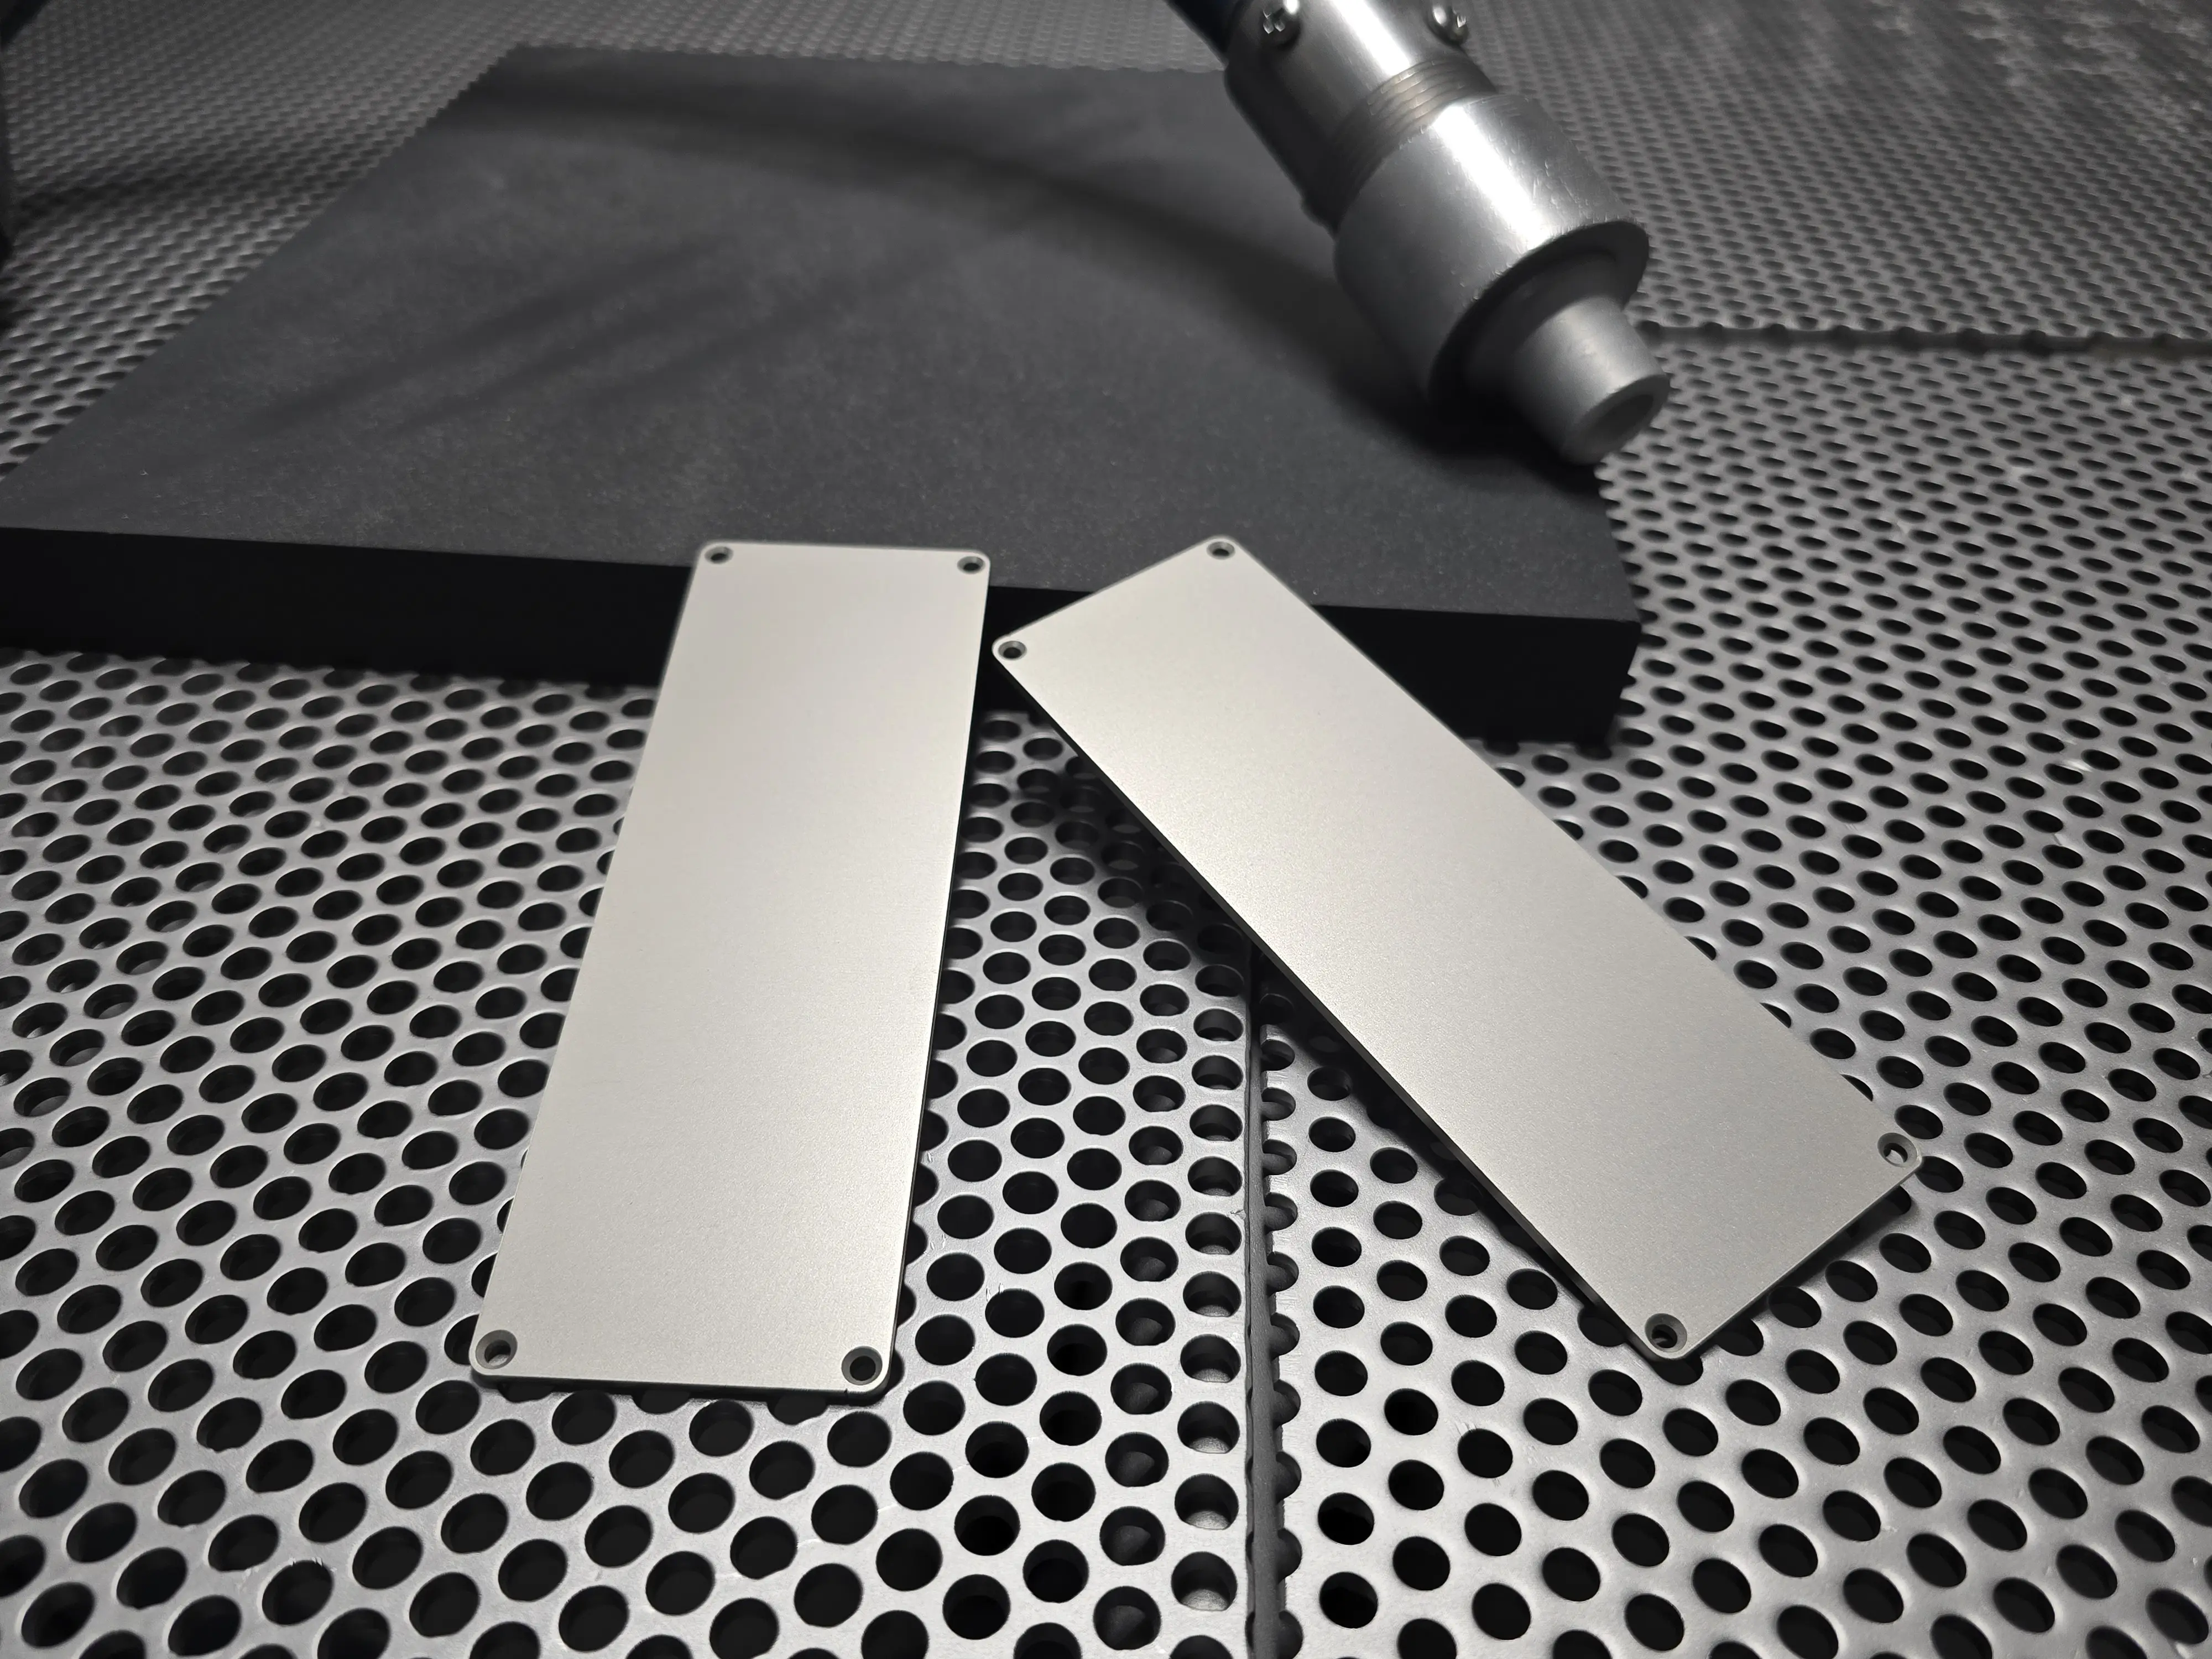
Bead blasted parts on the grate of a blast cabinet beside the blasting nozzle

Deburring

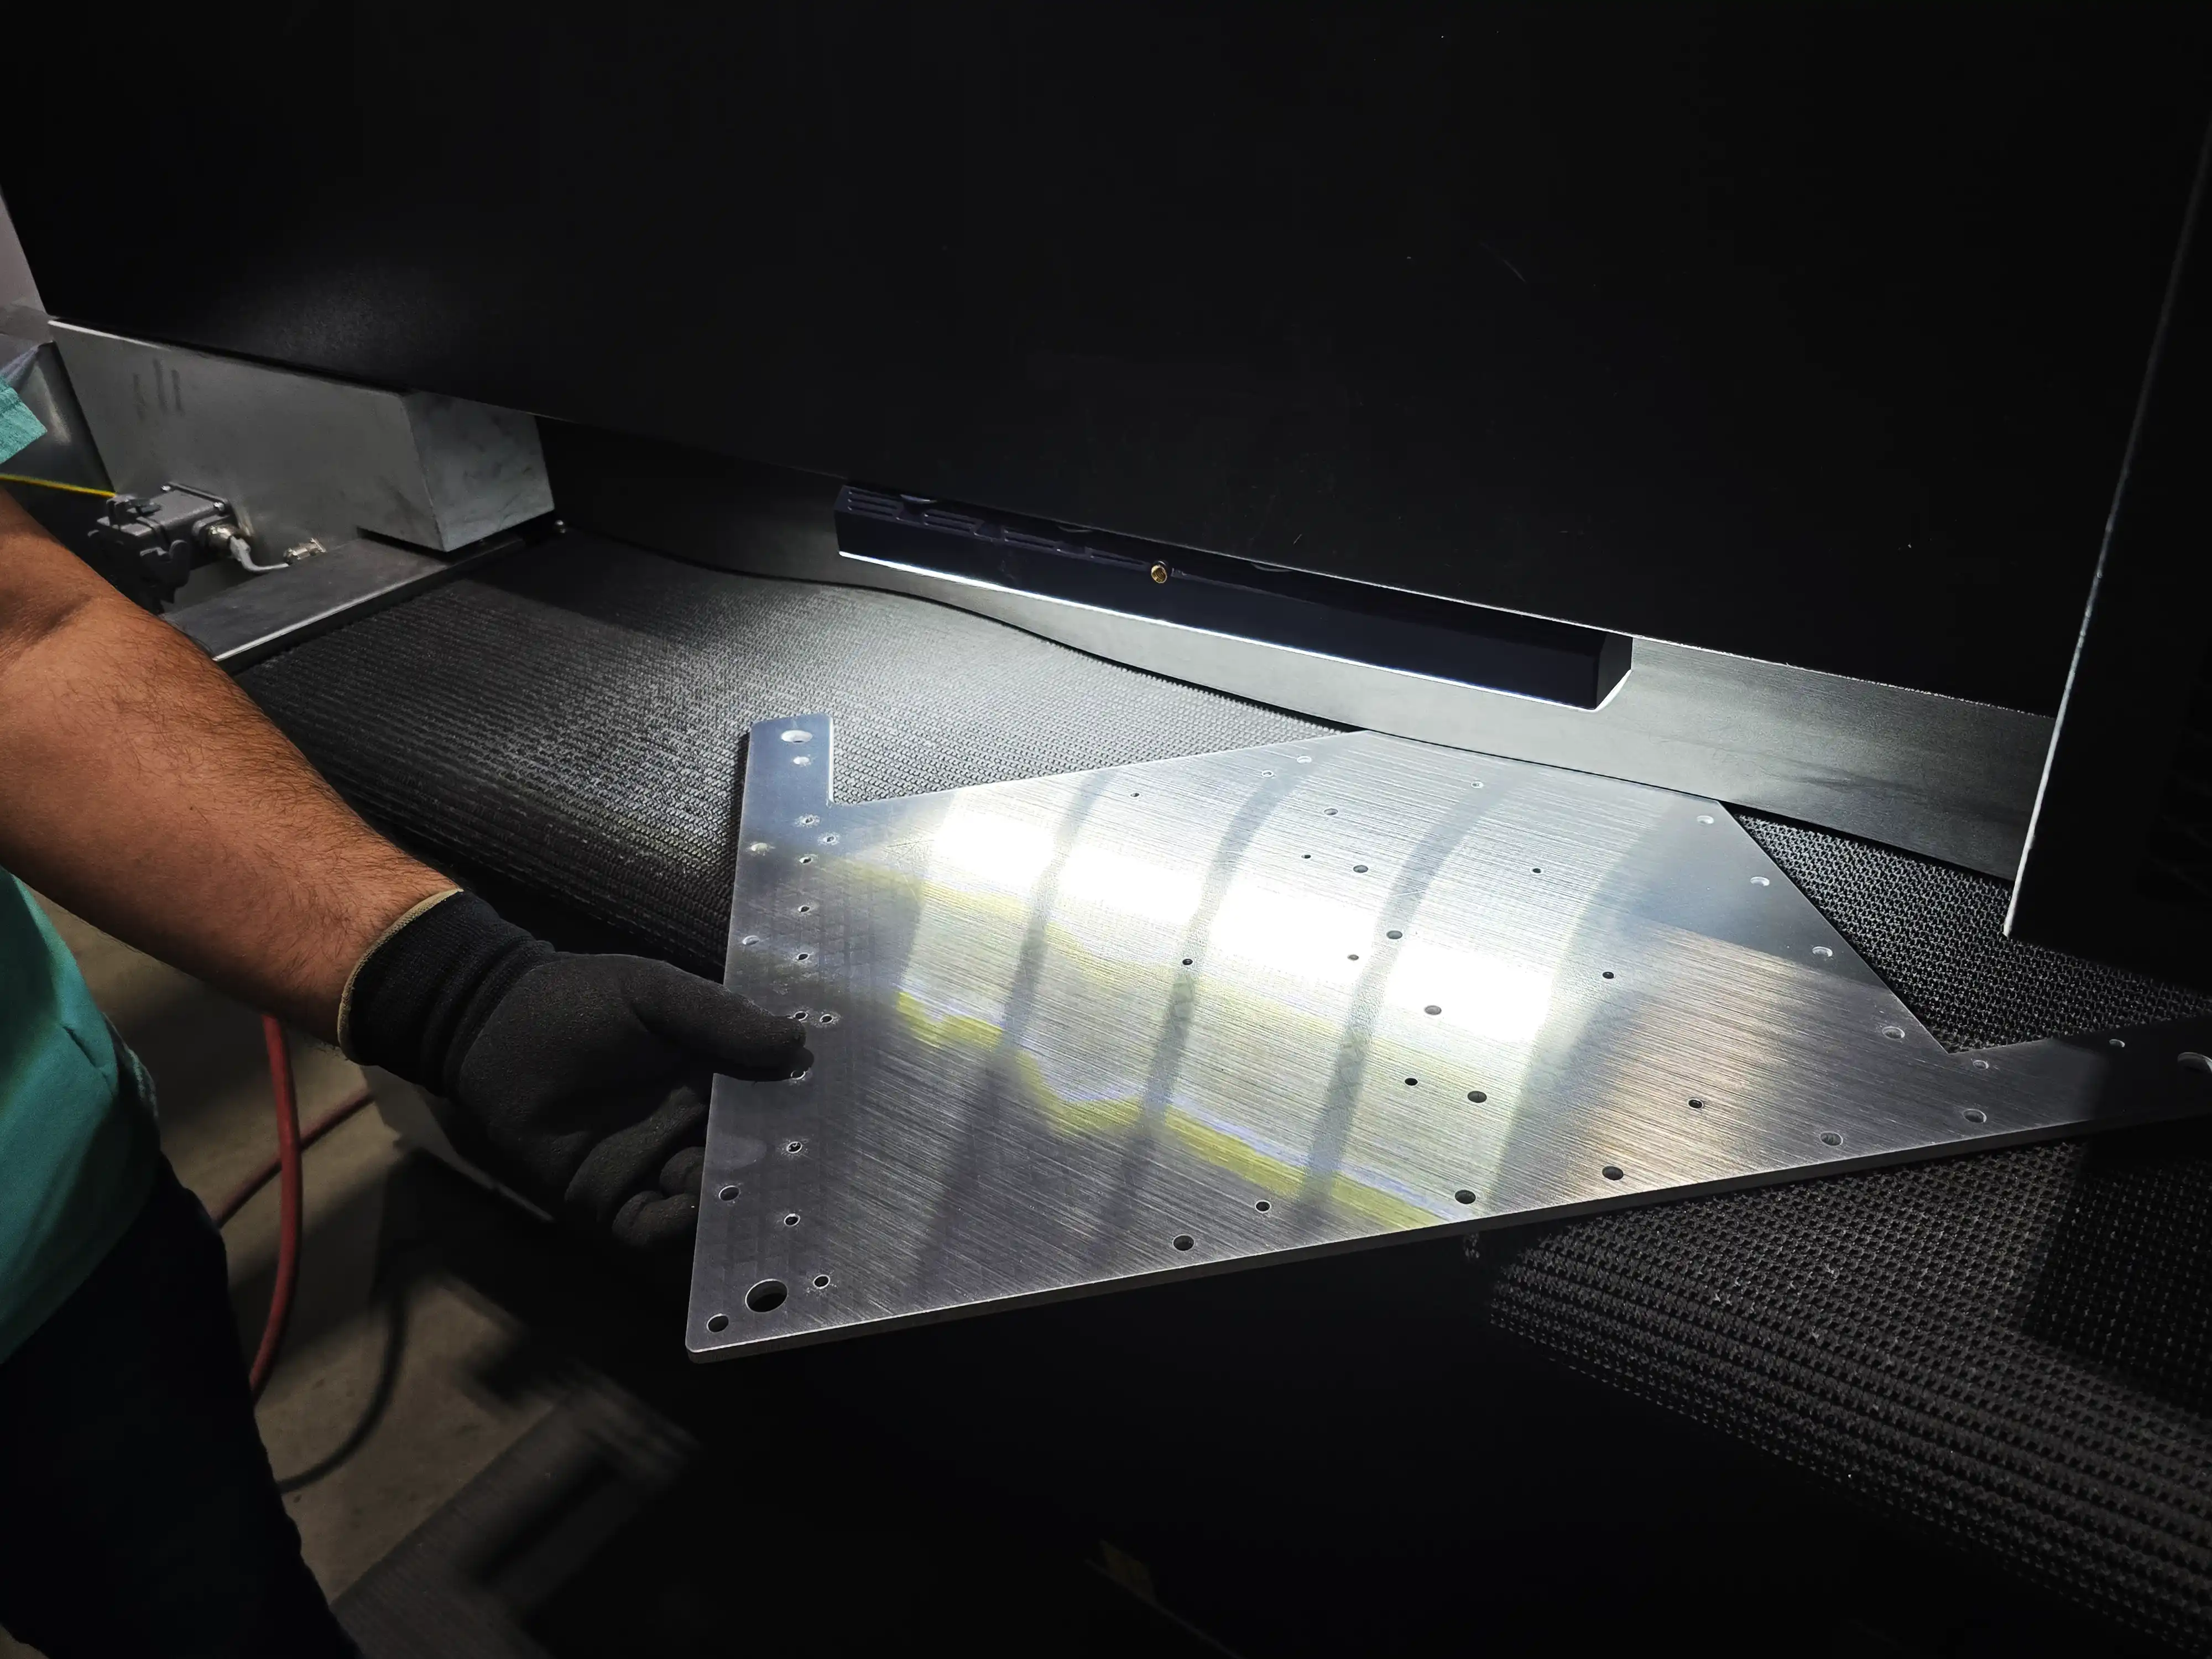
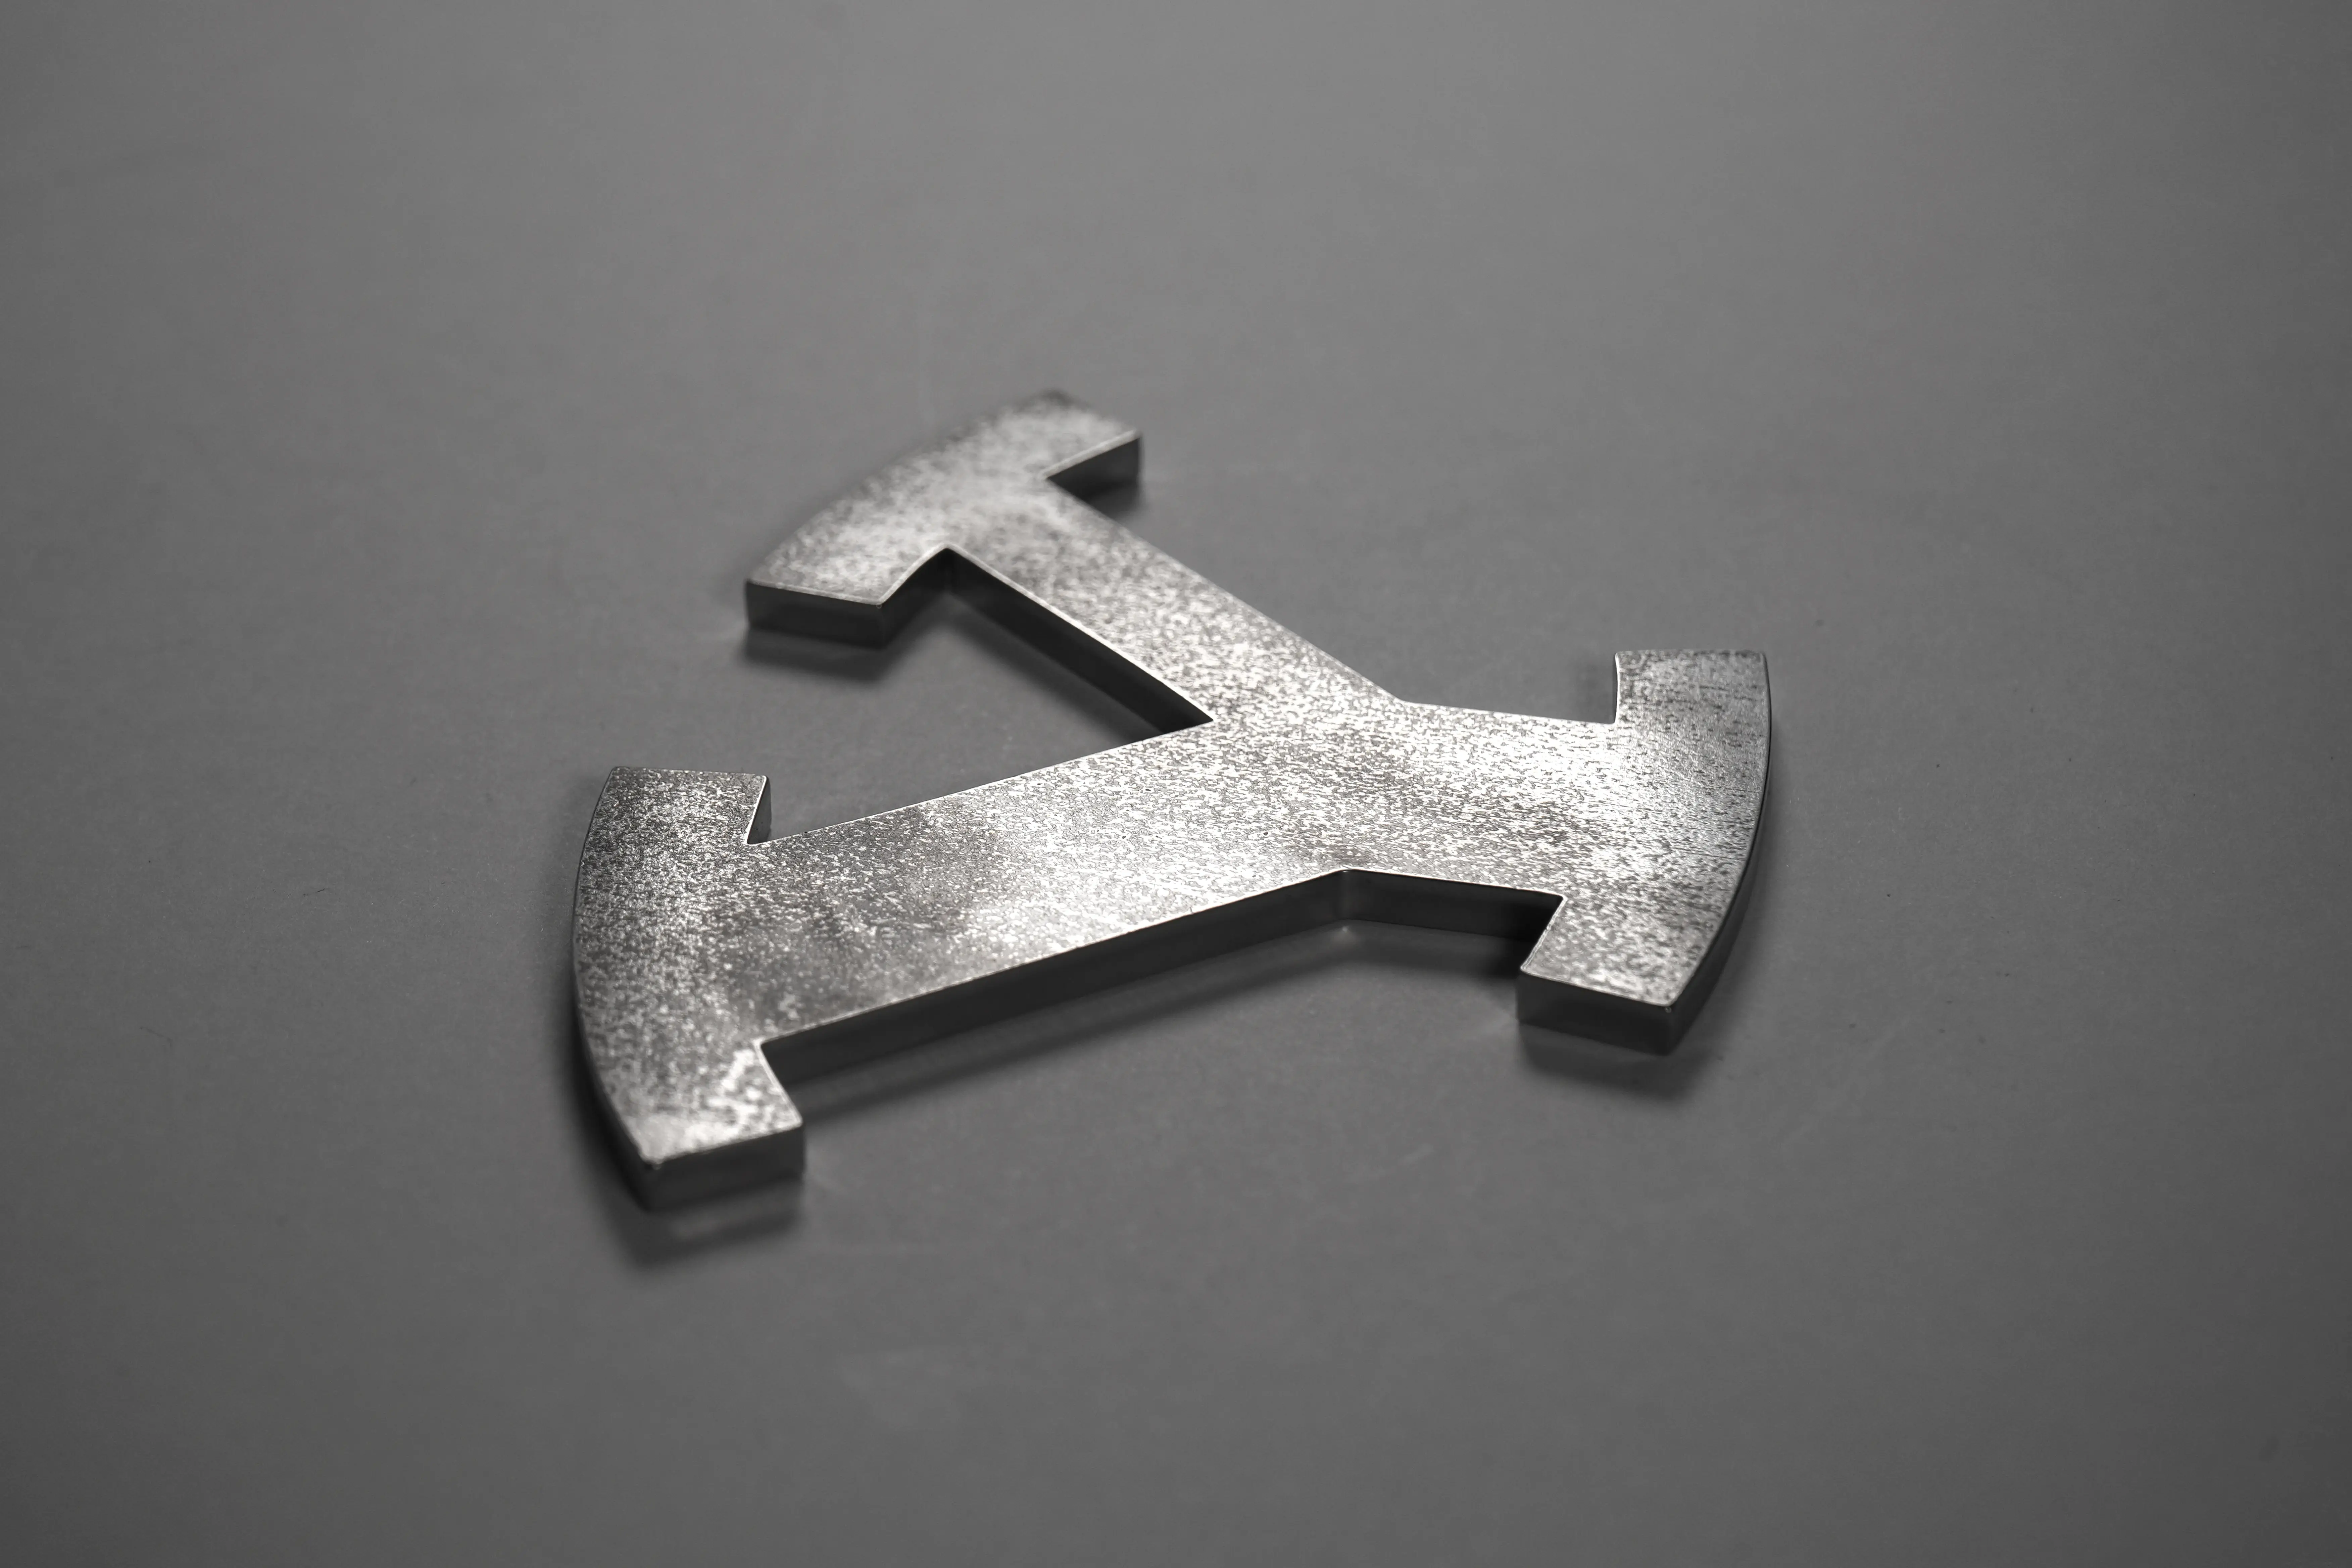
Deburring removes small metal burrs and sharp edges that can remain after laser cutting. This finishing process improves safety, handling, and fit during assembly without significantly changing the overall appearance of the part.
During cutting processes, small fragments of material called burrs can remain along the edges of a part. Deburring removes these imperfections and smooths the edges to improve part quality and usability. This process reduces the risk of cuts during handling and helps parts fit together more reliably during assembly. Deburring is commonly used for functional parts where safety, clean edges, and consistent fit are more important than cosmetic appearance.
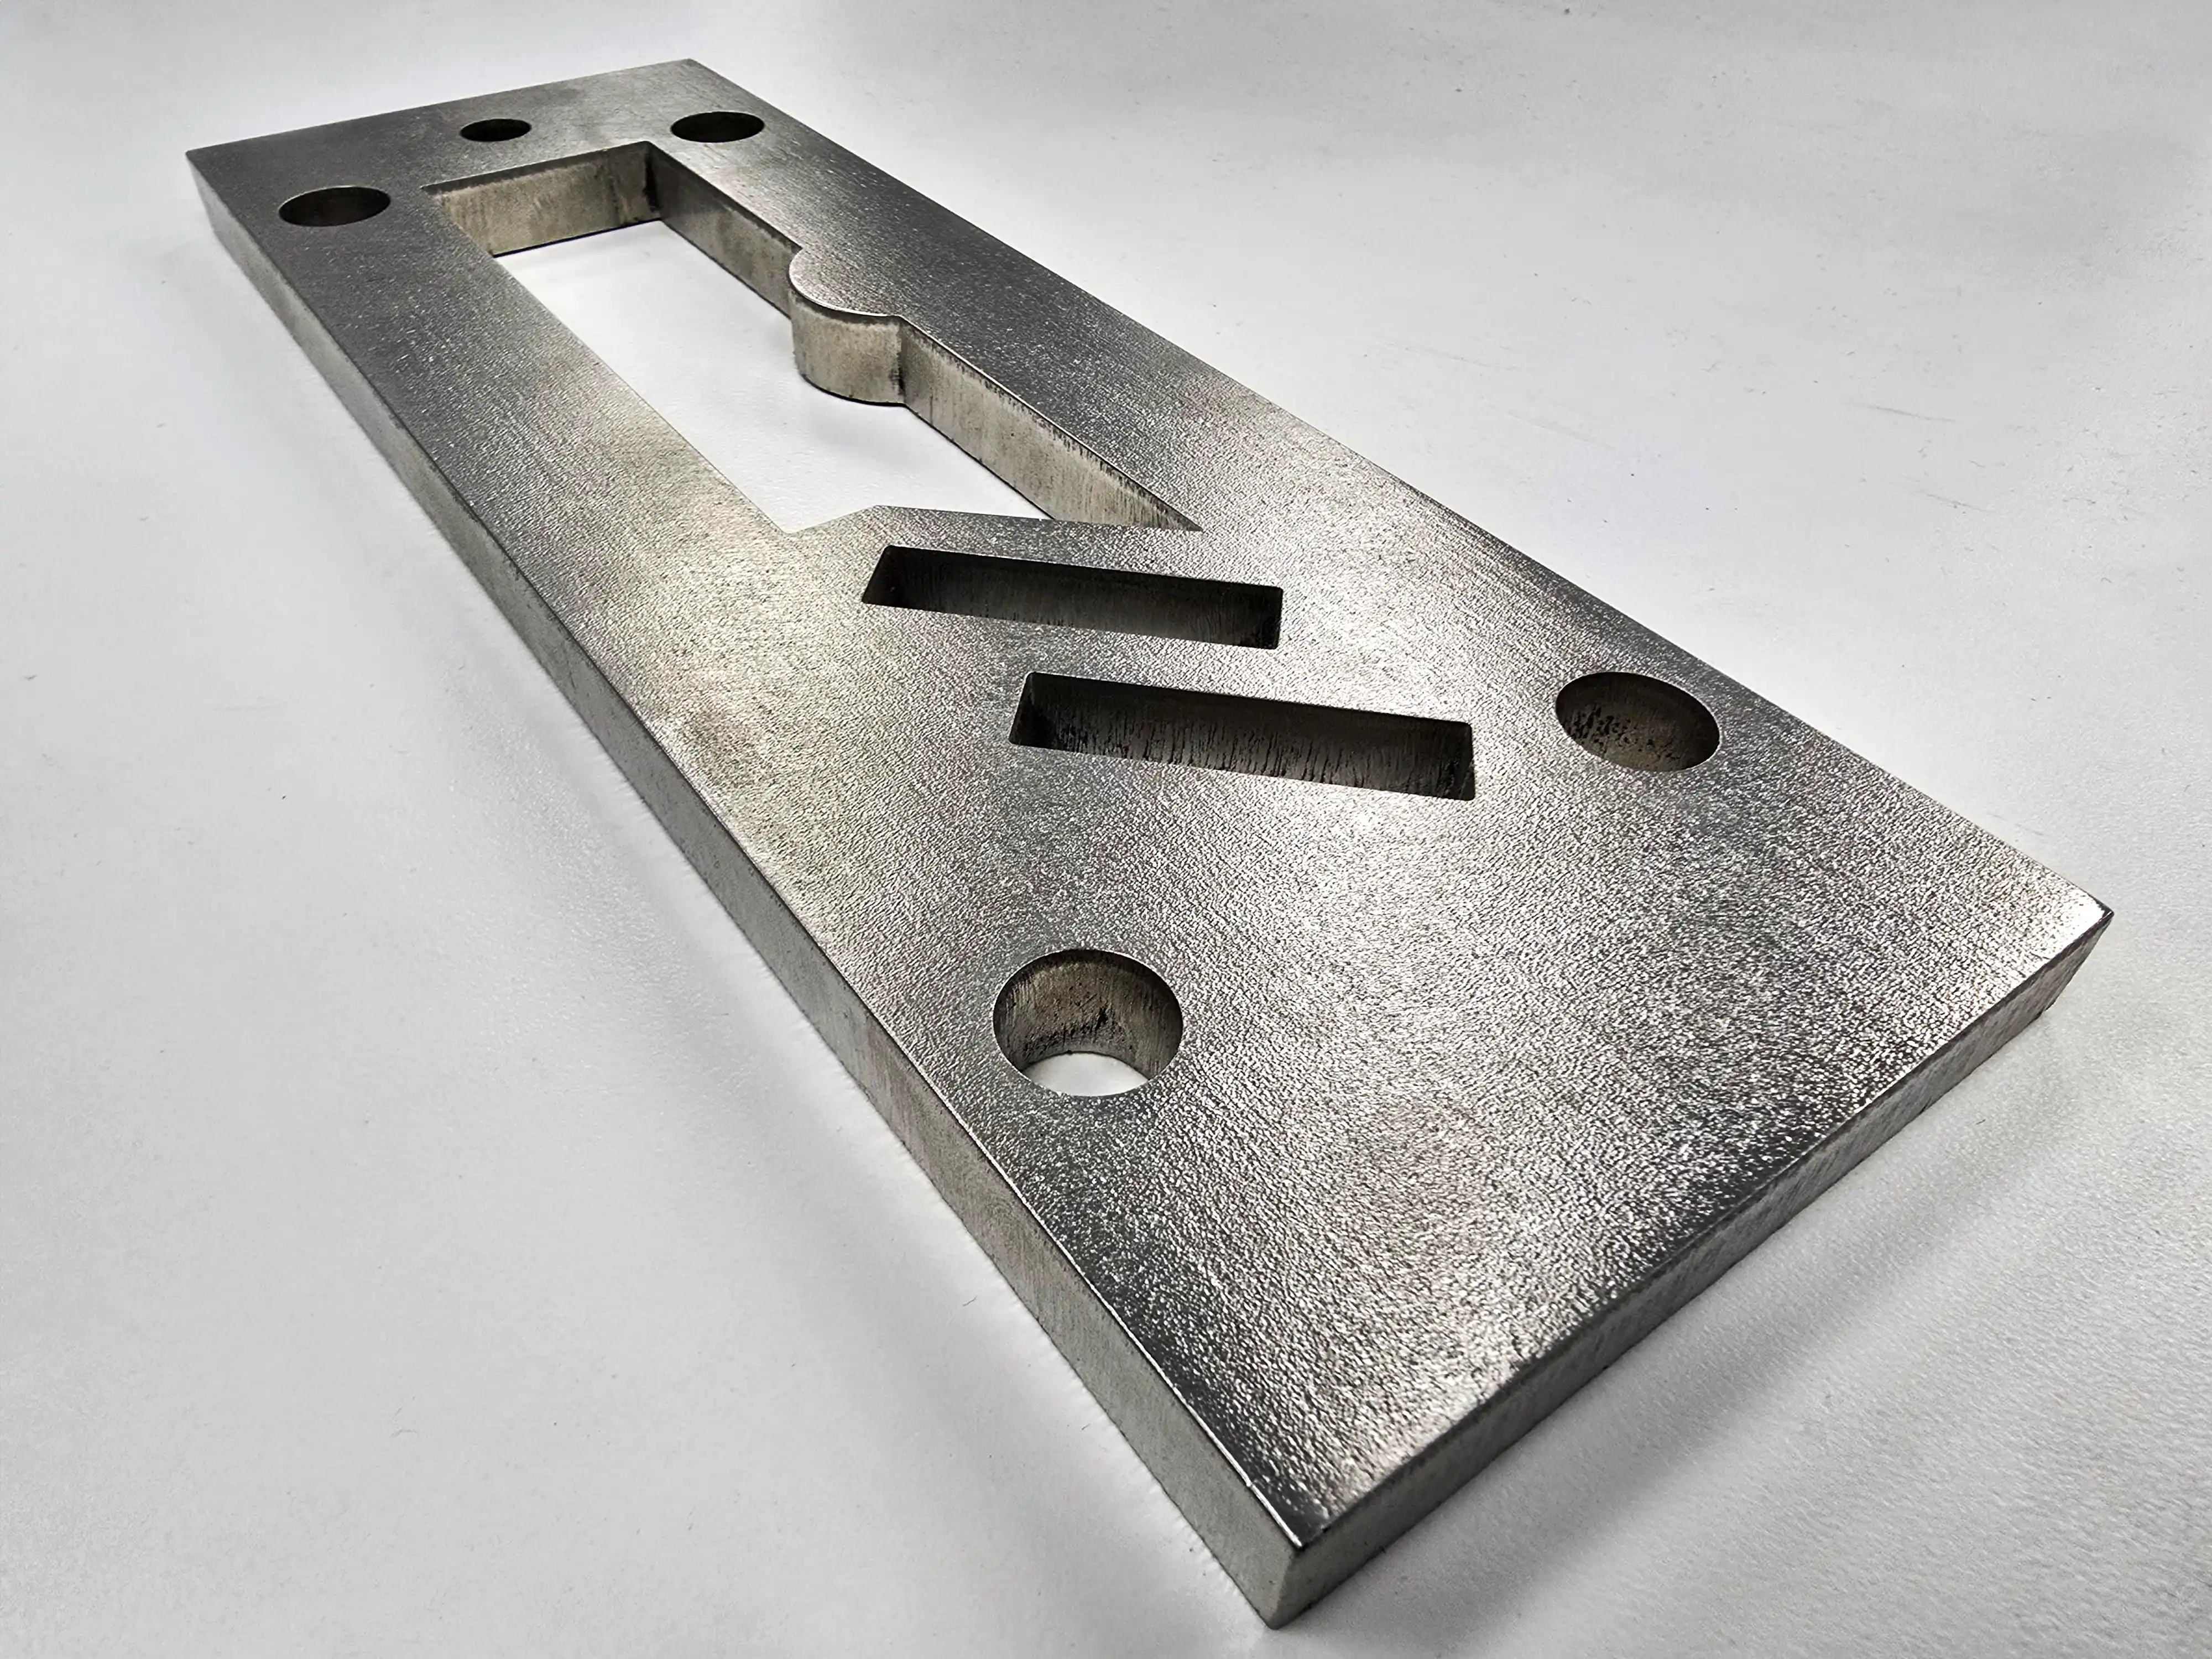
Thick laser cut block letter Y after deburringAluminum plate being fed into a deburring machineDeburred thick stainless steel plate with slots and holes

Before and After

Before deburring, laser cut parts may have sharp edges and small burrs along the cut surfaces. These edges can feel rough to the touch and may interfere with assembly or safe handling. After deburring, edges are smoother and safer while maintaining the original geometry of the part. The process focuses on removing sharpness rather than changing the visible surface finish.
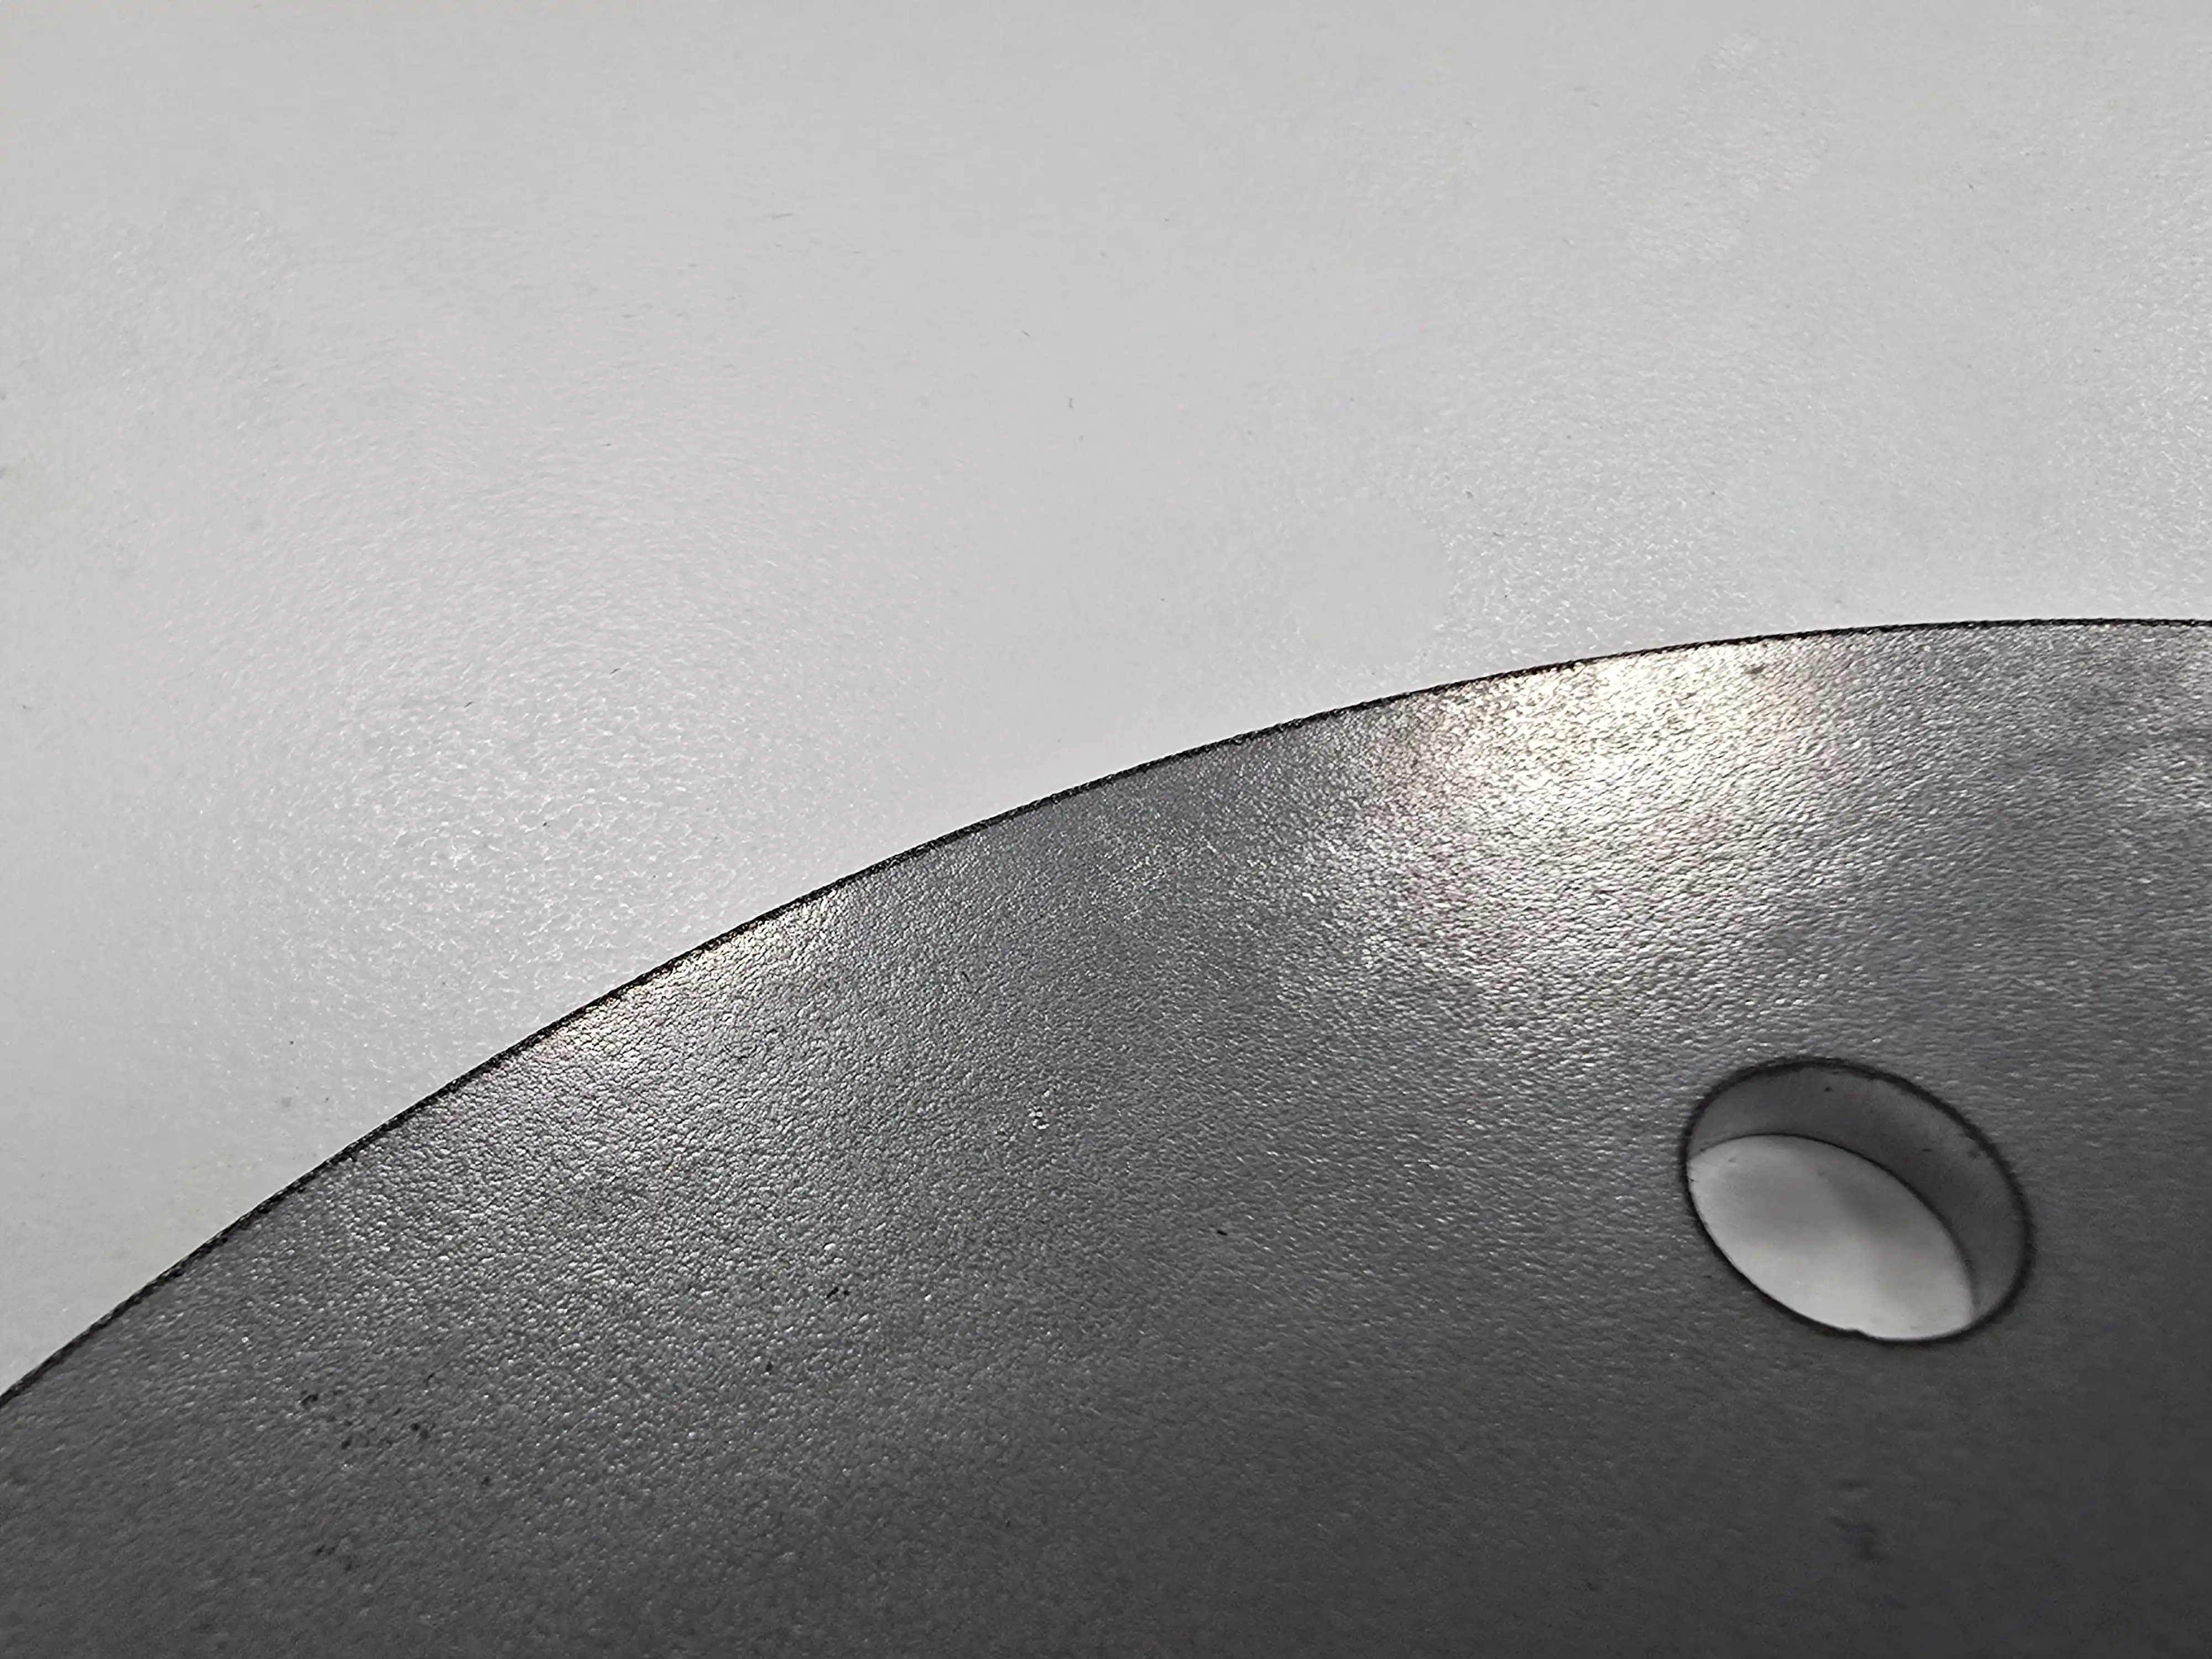
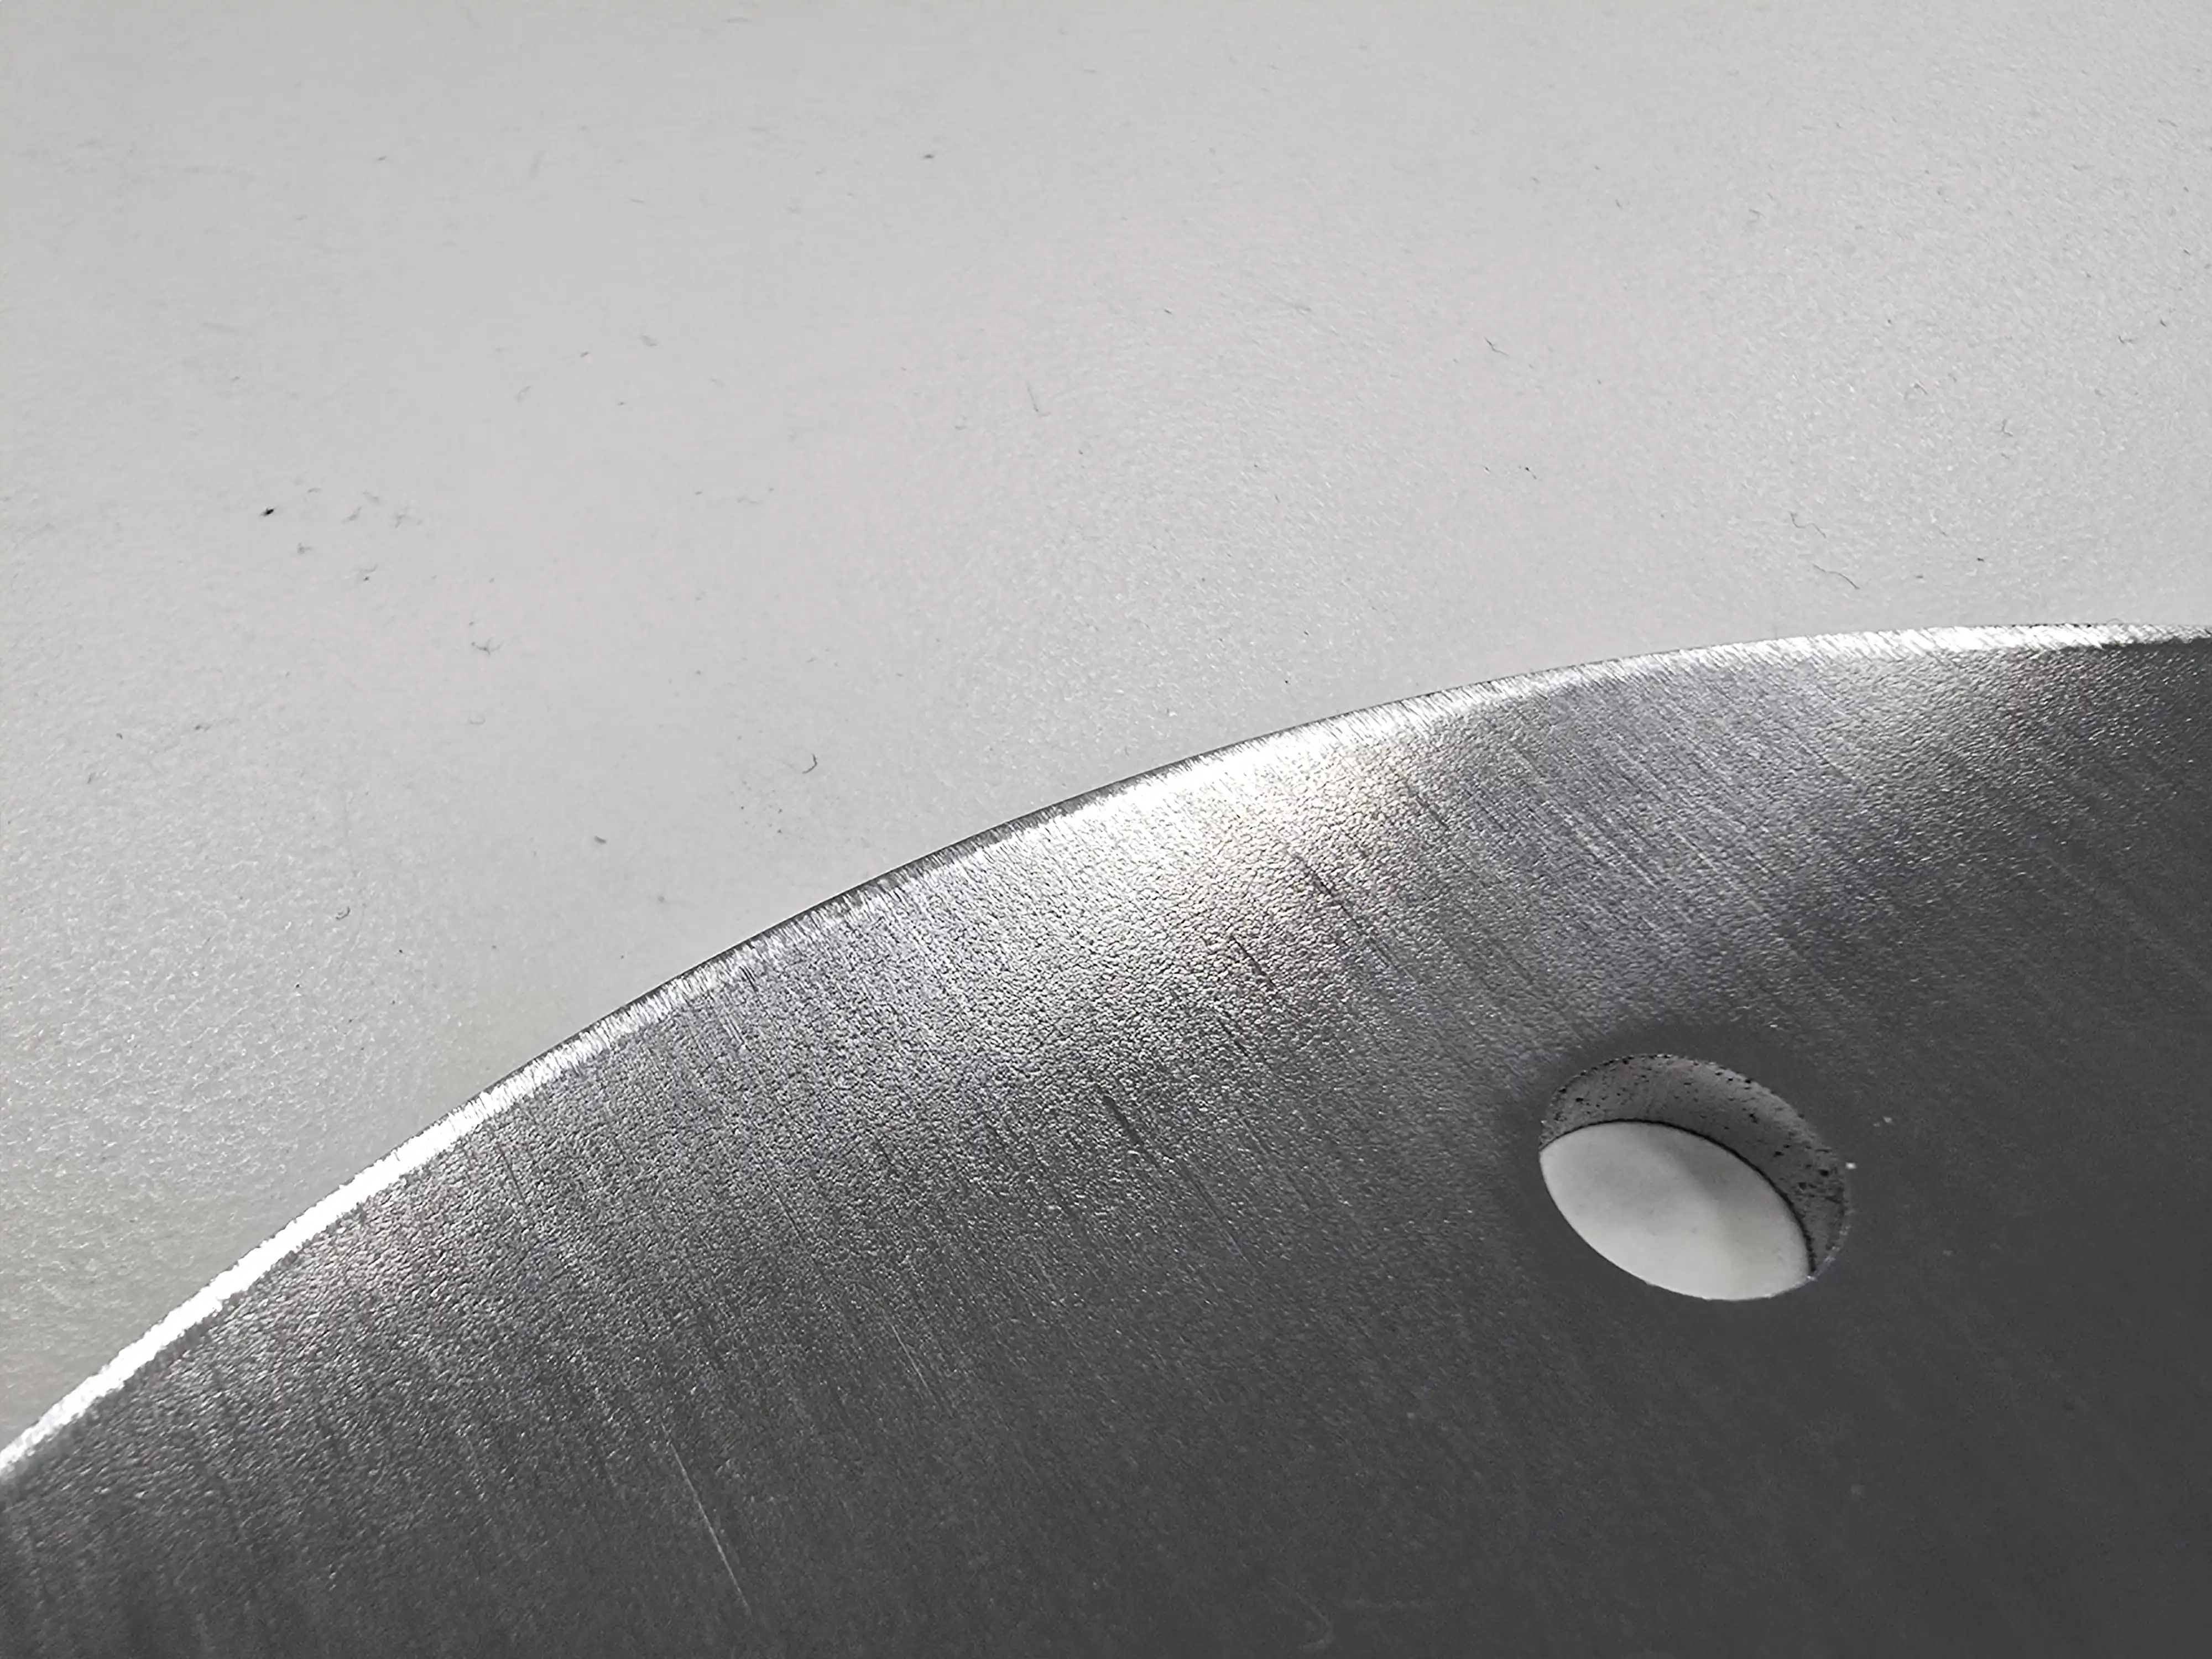
Close-up of a laser cut steel edge and hole before deburringThe same edge and hole after deburring

Best Practices for Success

Deburring works well on most laser cut parts and materials. Extremely small features or tight internal corners may not be fully reachable by the process. Parts should be designed with standard laser cutting tolerances, and thin delicate features should be avoided if they could bend during finishing.
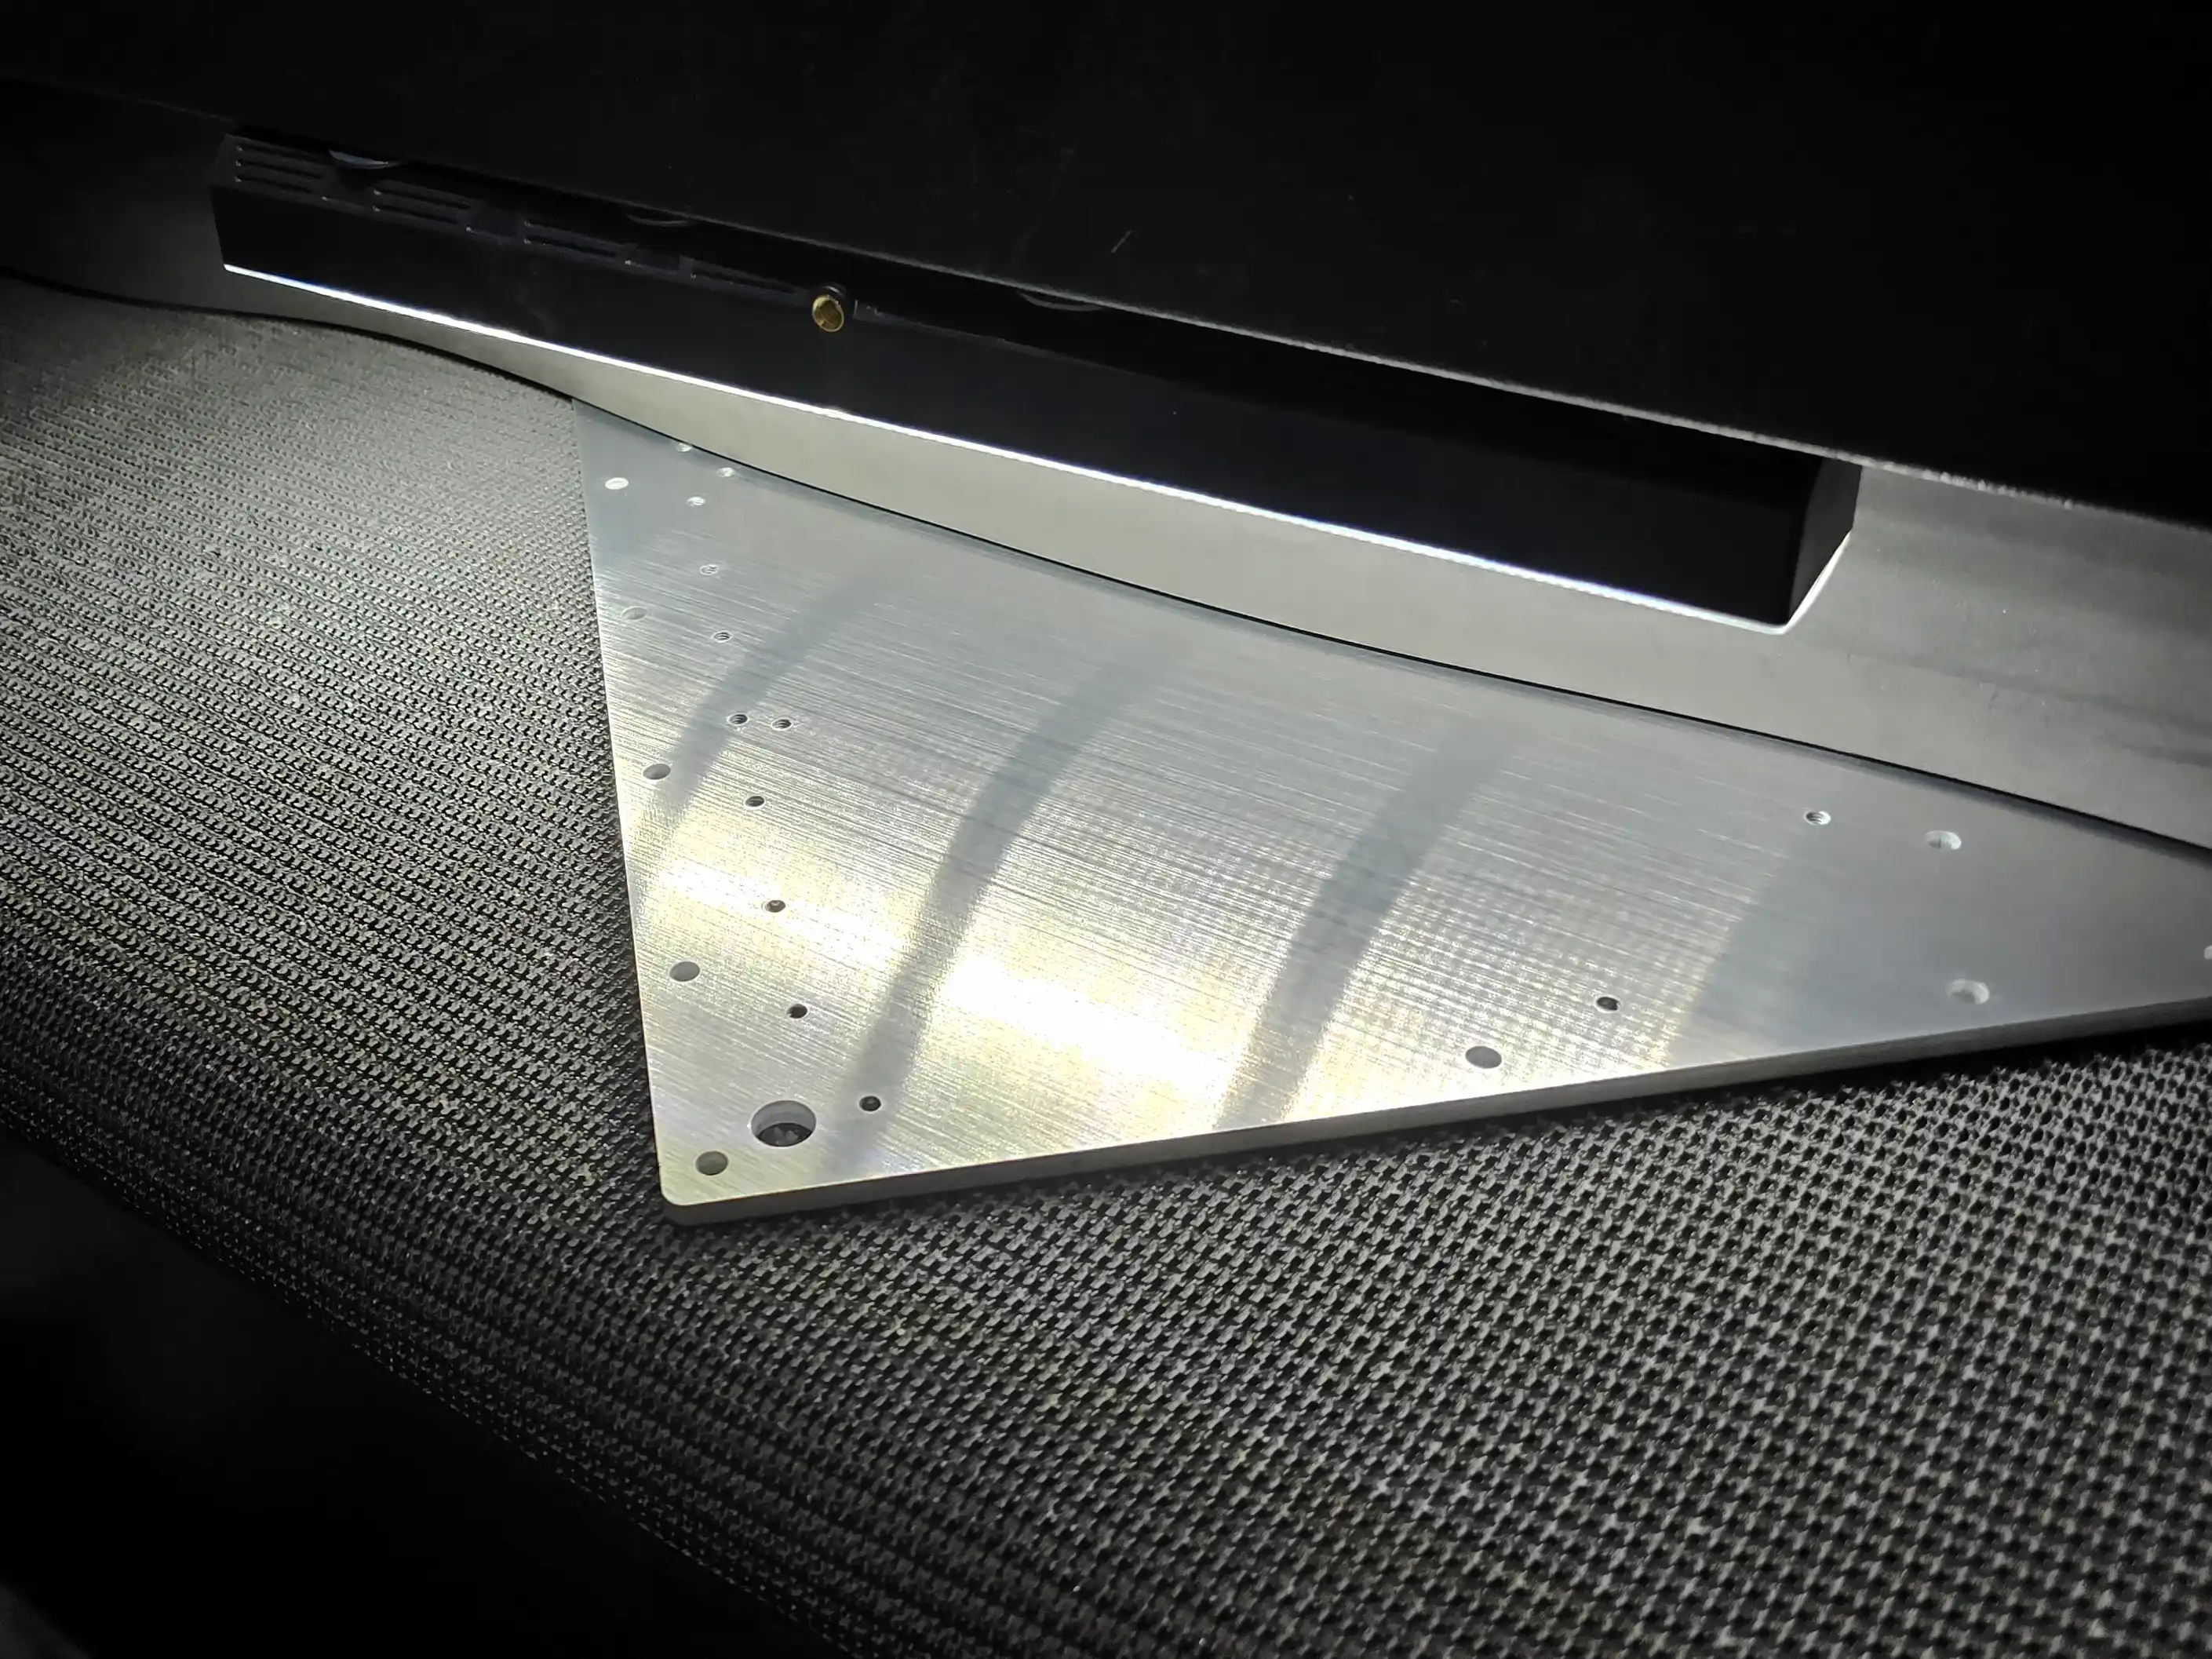
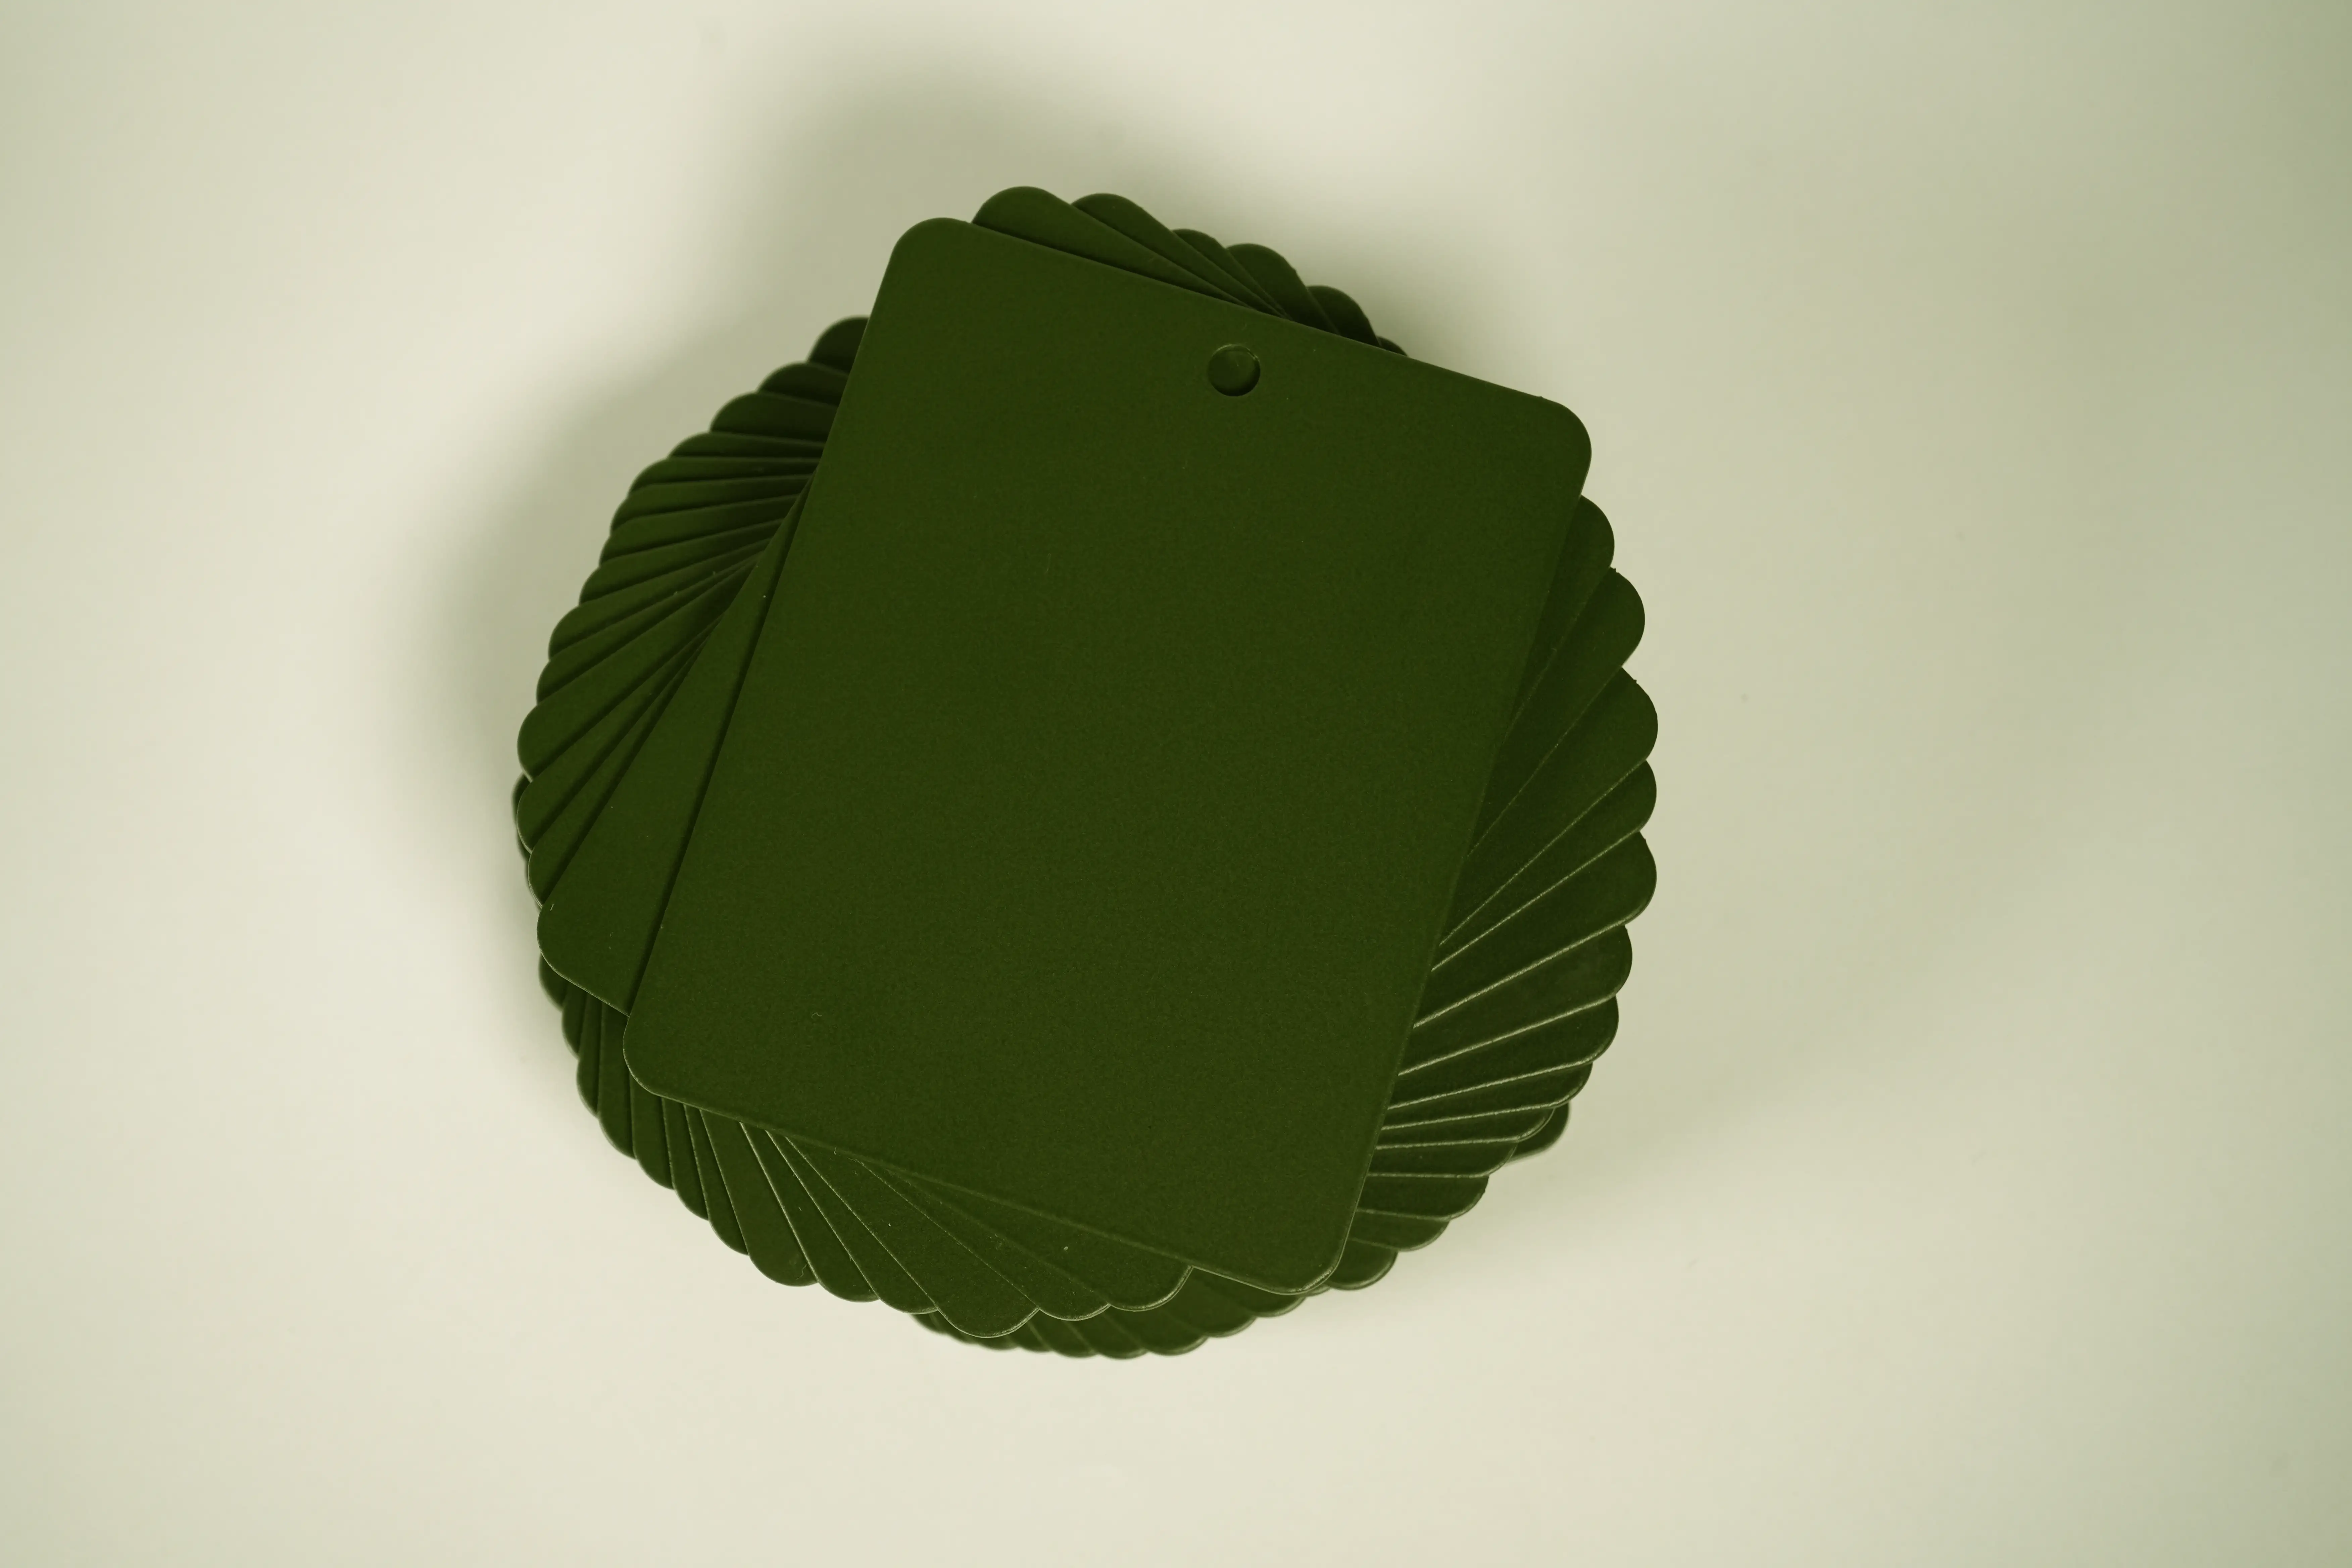
Aluminum plate on the conveyor of a deburring machine

Powder Coating

Powder coating applies a dry powder to the surface of a part and cures it with heat to form a durable protective layer. The result is a smooth, consistent finish available in a wide range of colors.
Powder coating is a finishing process that uses electrostatic charge to apply dry powder to a metal surface. After application, the part is cured in an oven, where the powder melts and forms a durable, continuous coating. This finish provides excellent resistance to corrosion, chemicals, and wear while also enhancing the visual appearance of the part. Powder coating is commonly used for products that require both durability and aesthetic appeal, such as outdoor equipment, enclosures, brackets, and consumer products.
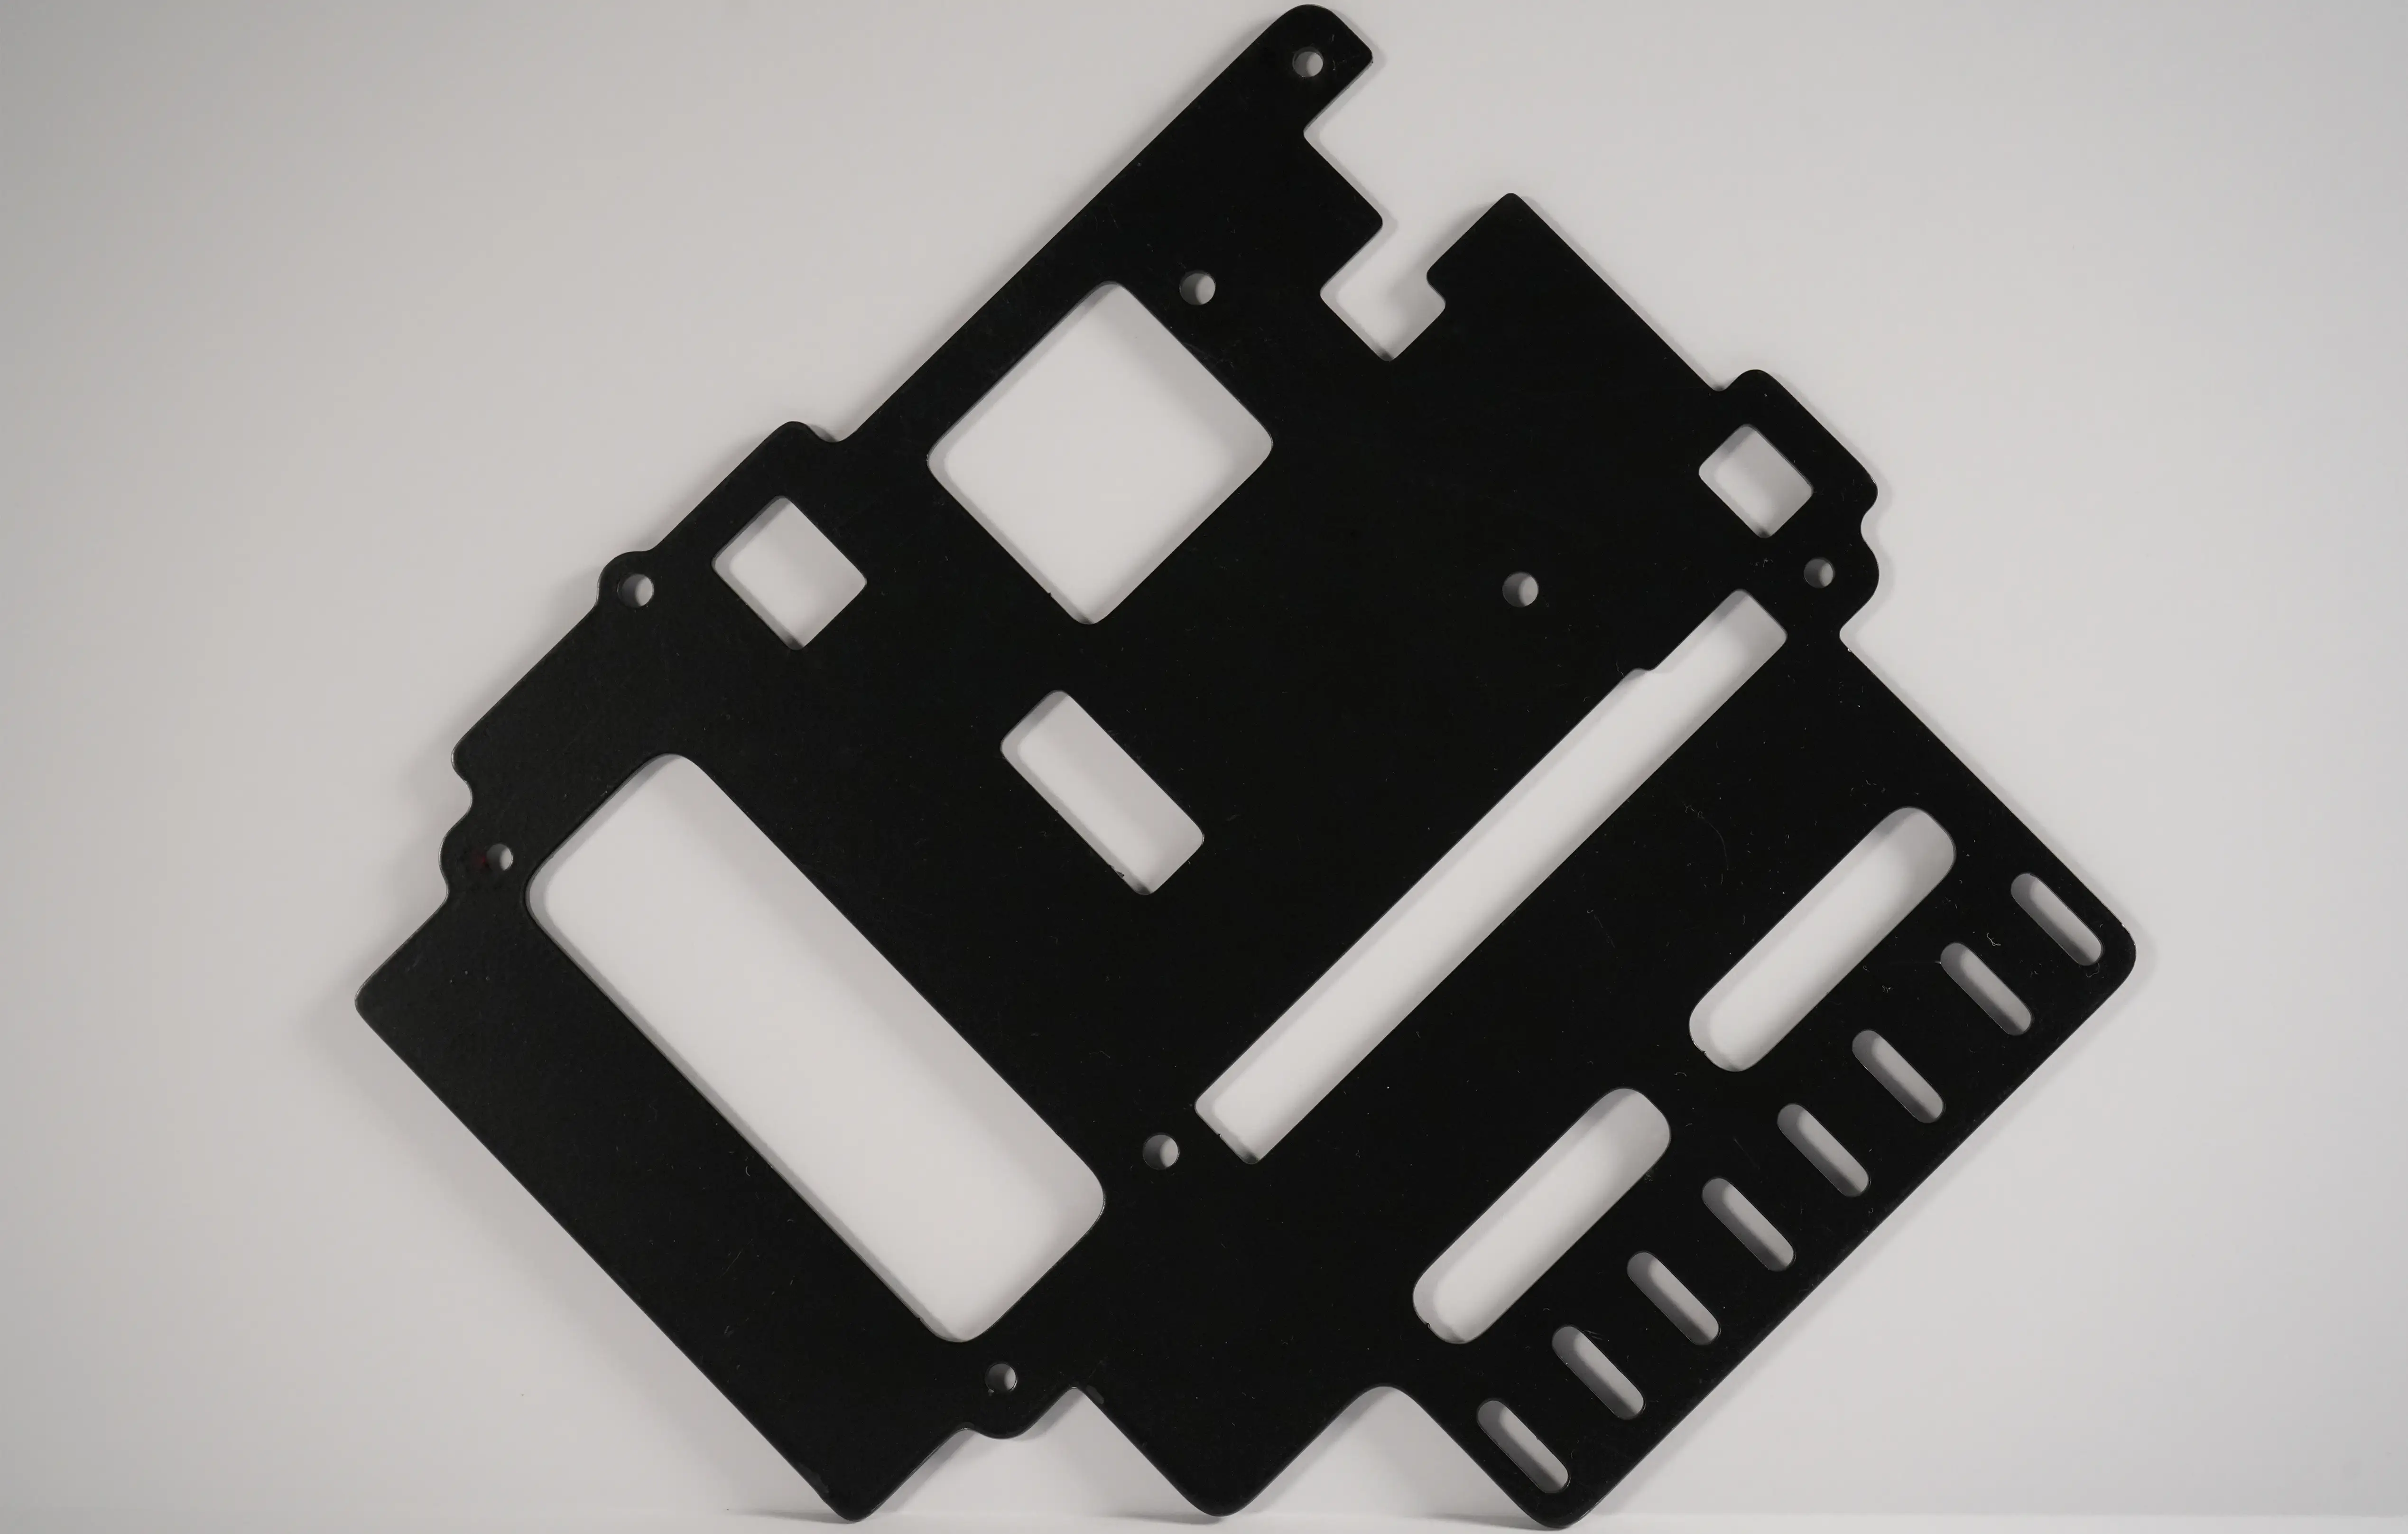
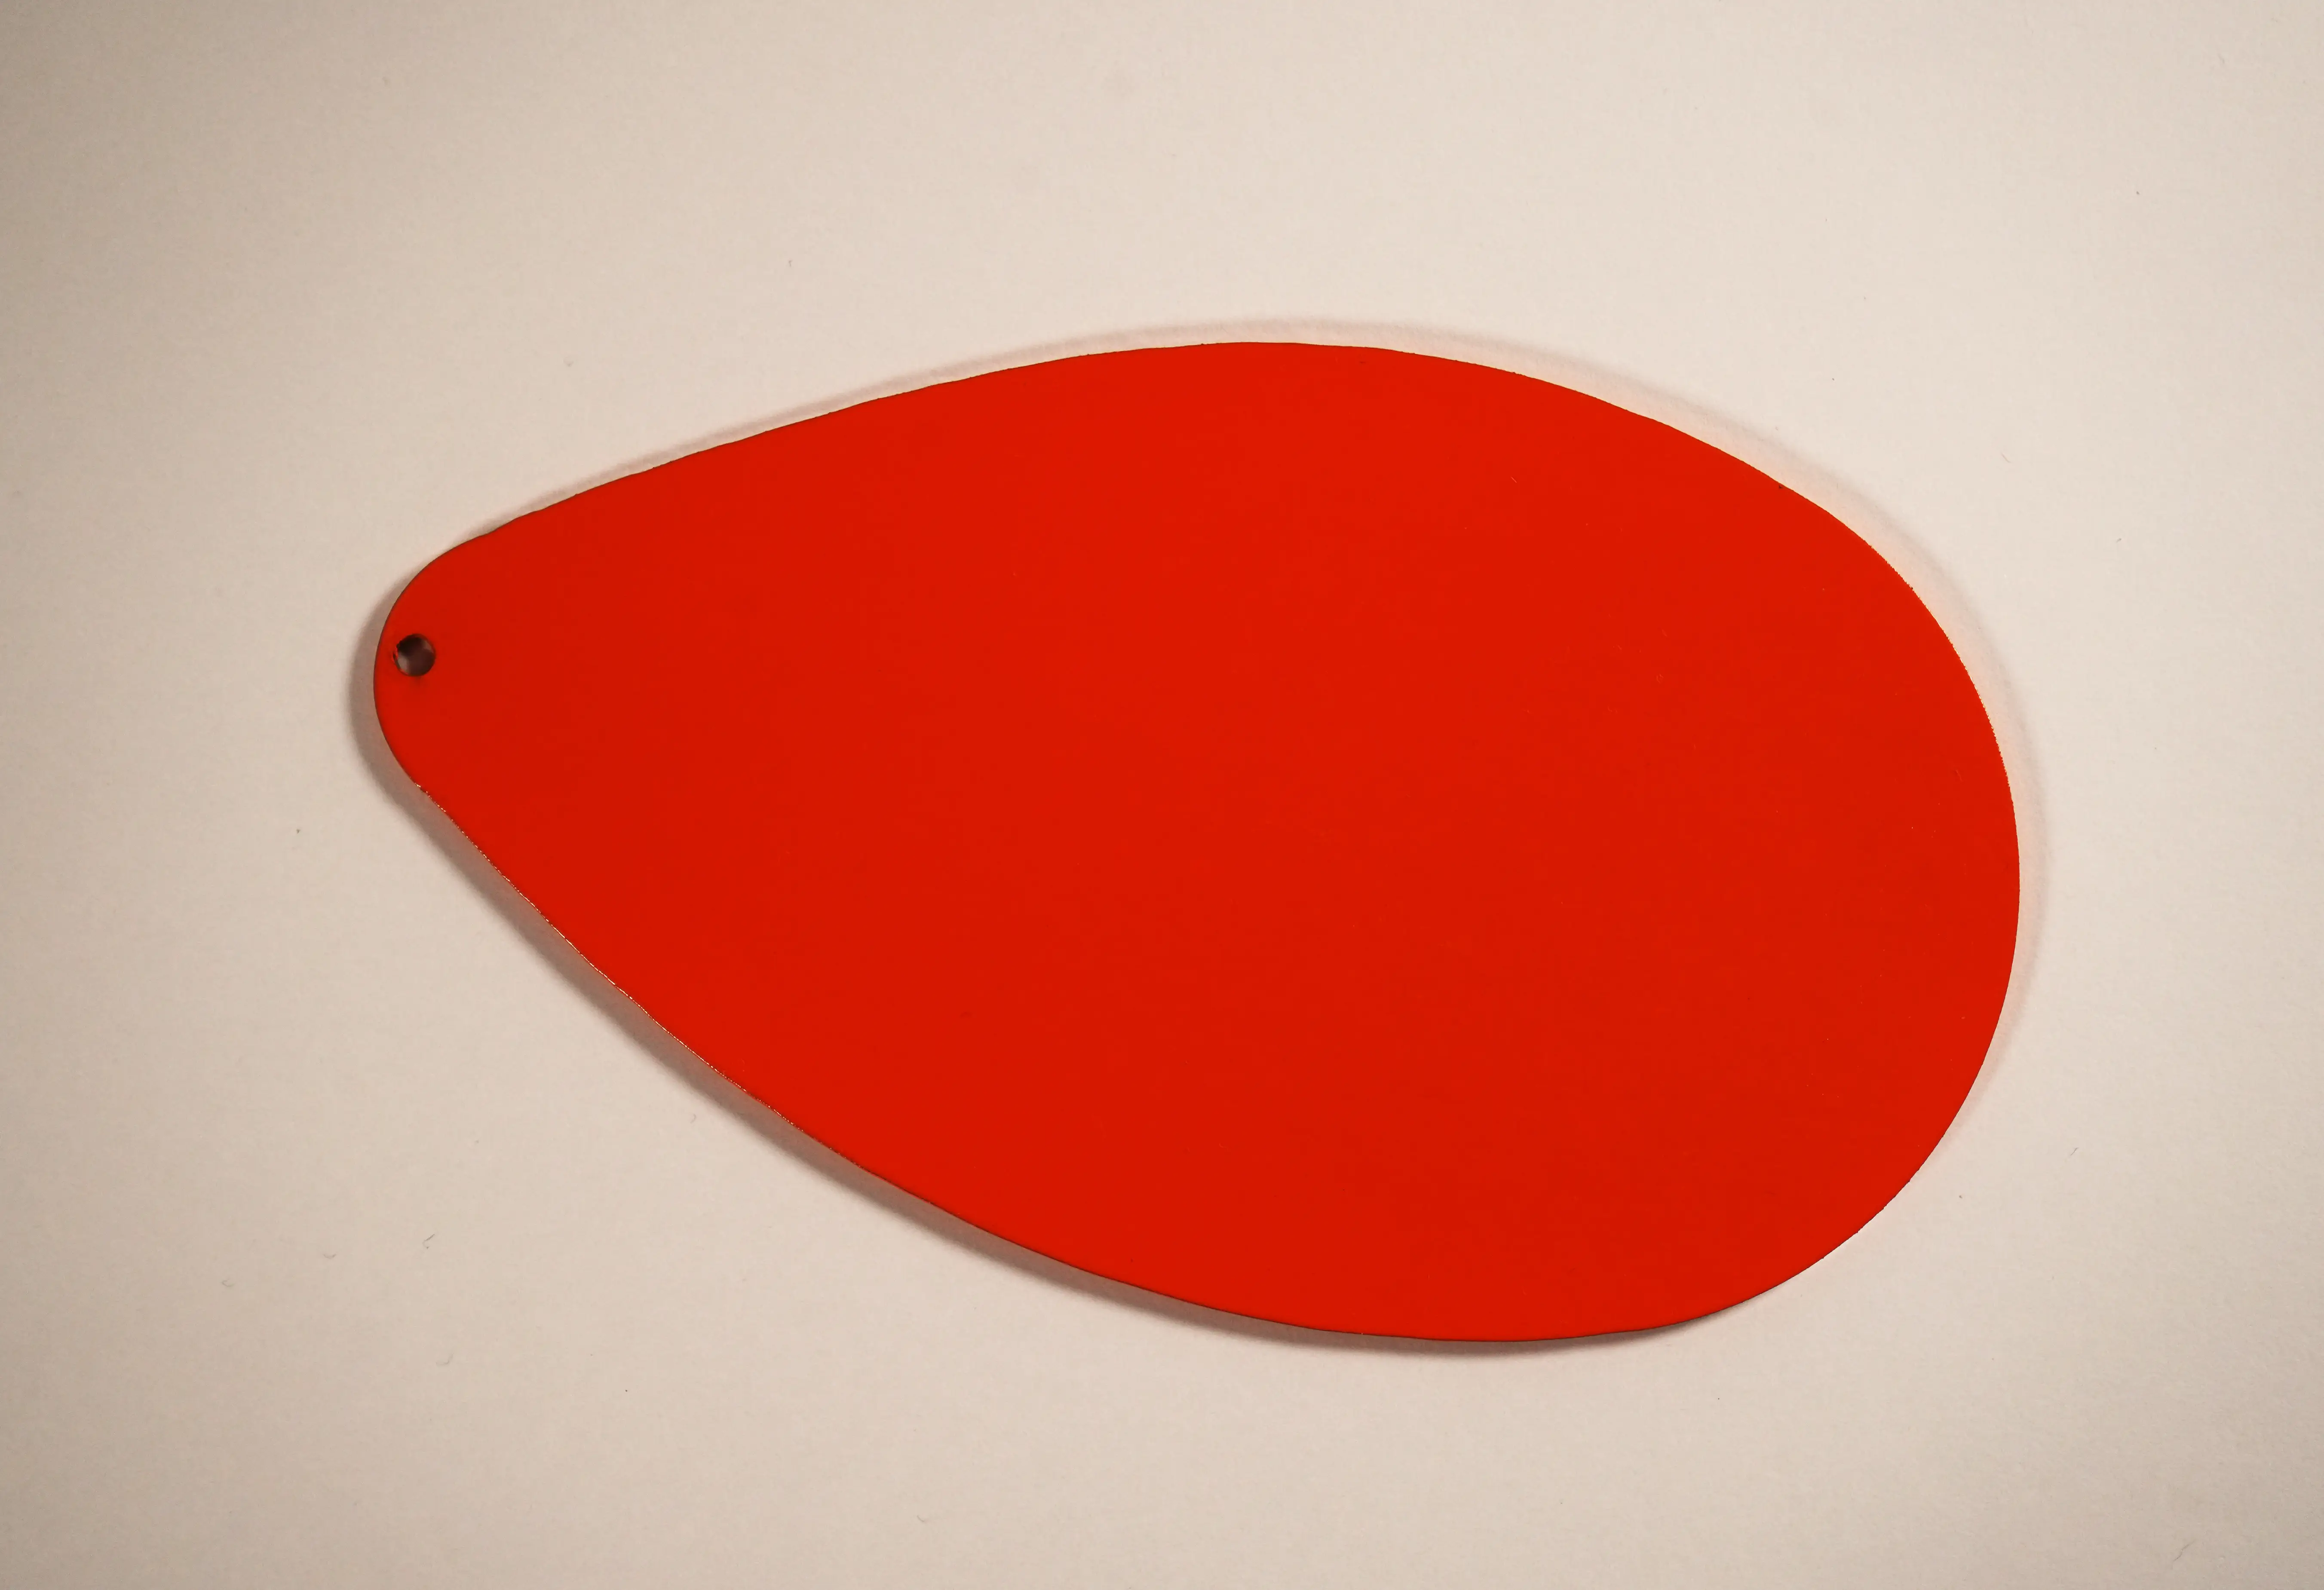
Fanned stack of dark green powder coated platesBlack powder coated laser cut plate with rectangular cutoutsTeardrop-shaped part powder coated in red

Before and After

Before powder coating, metal parts may show natural material variations, surface scratches, or discoloration from cutting. These imperfections can make the part look unfinished. After powder coating, the surface is covered by a uniform colored layer that hides most minor imperfections while protecting the metal underneath. The result is a durable and professional looking finish.
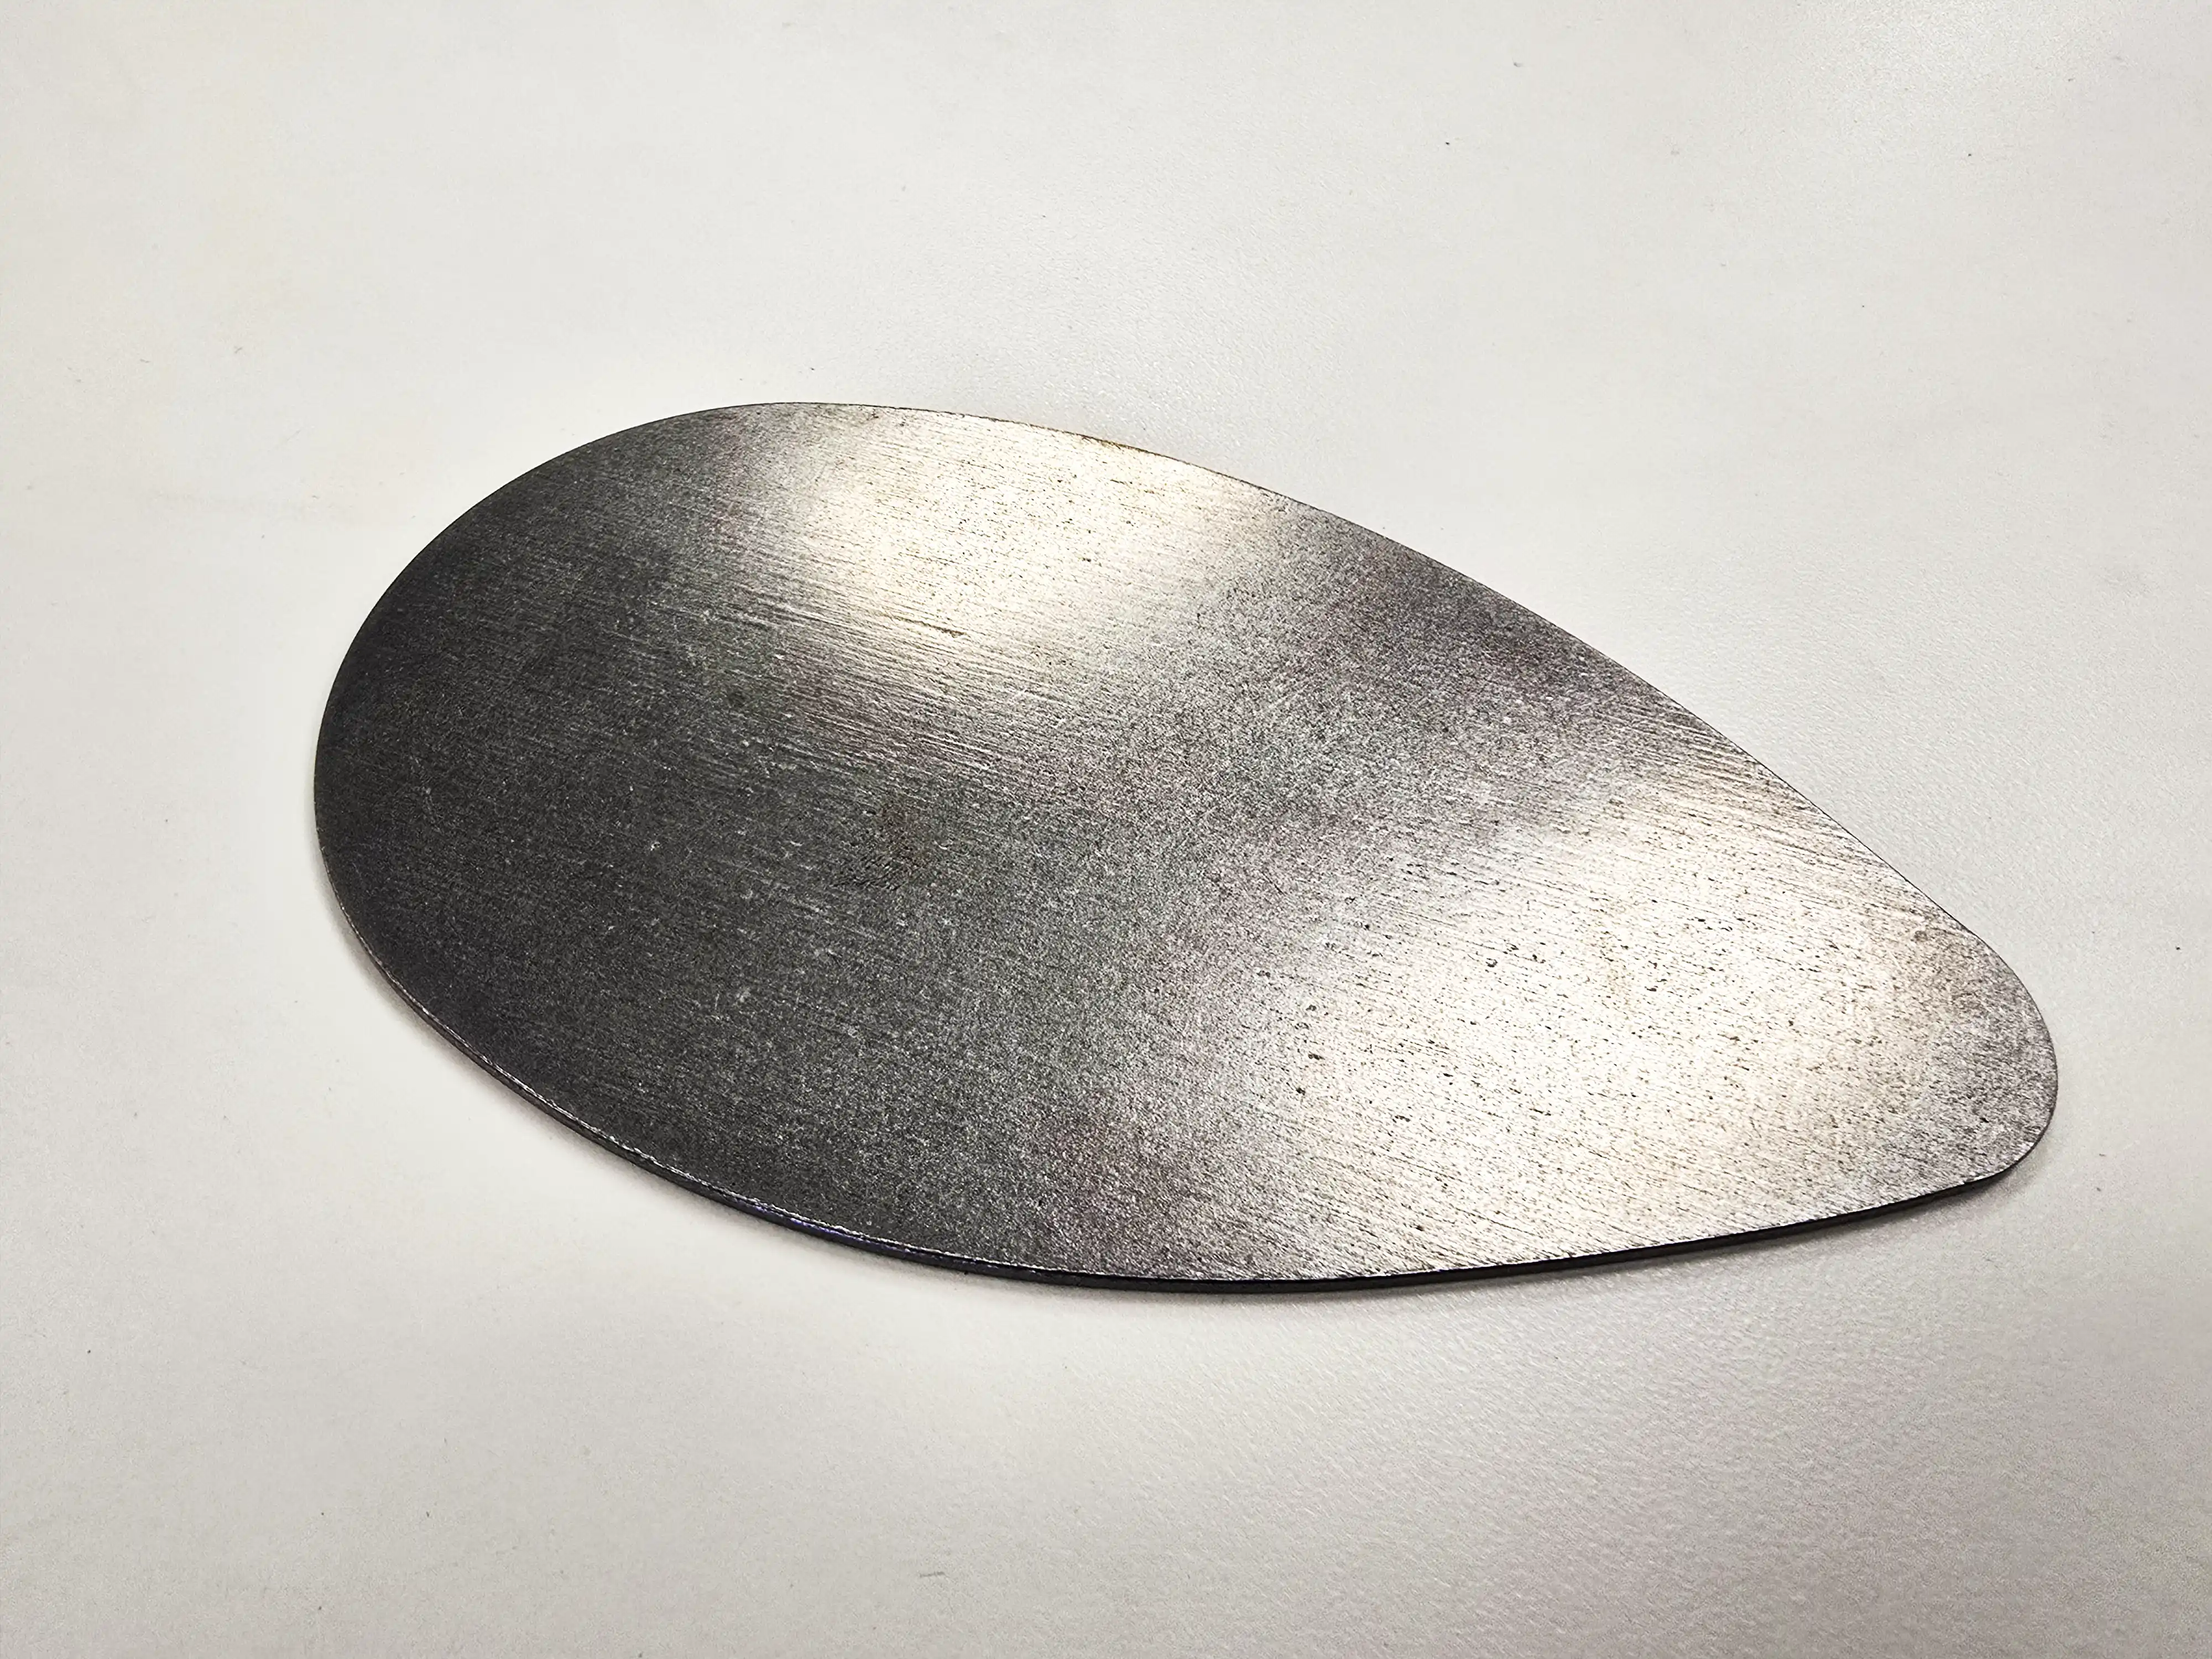
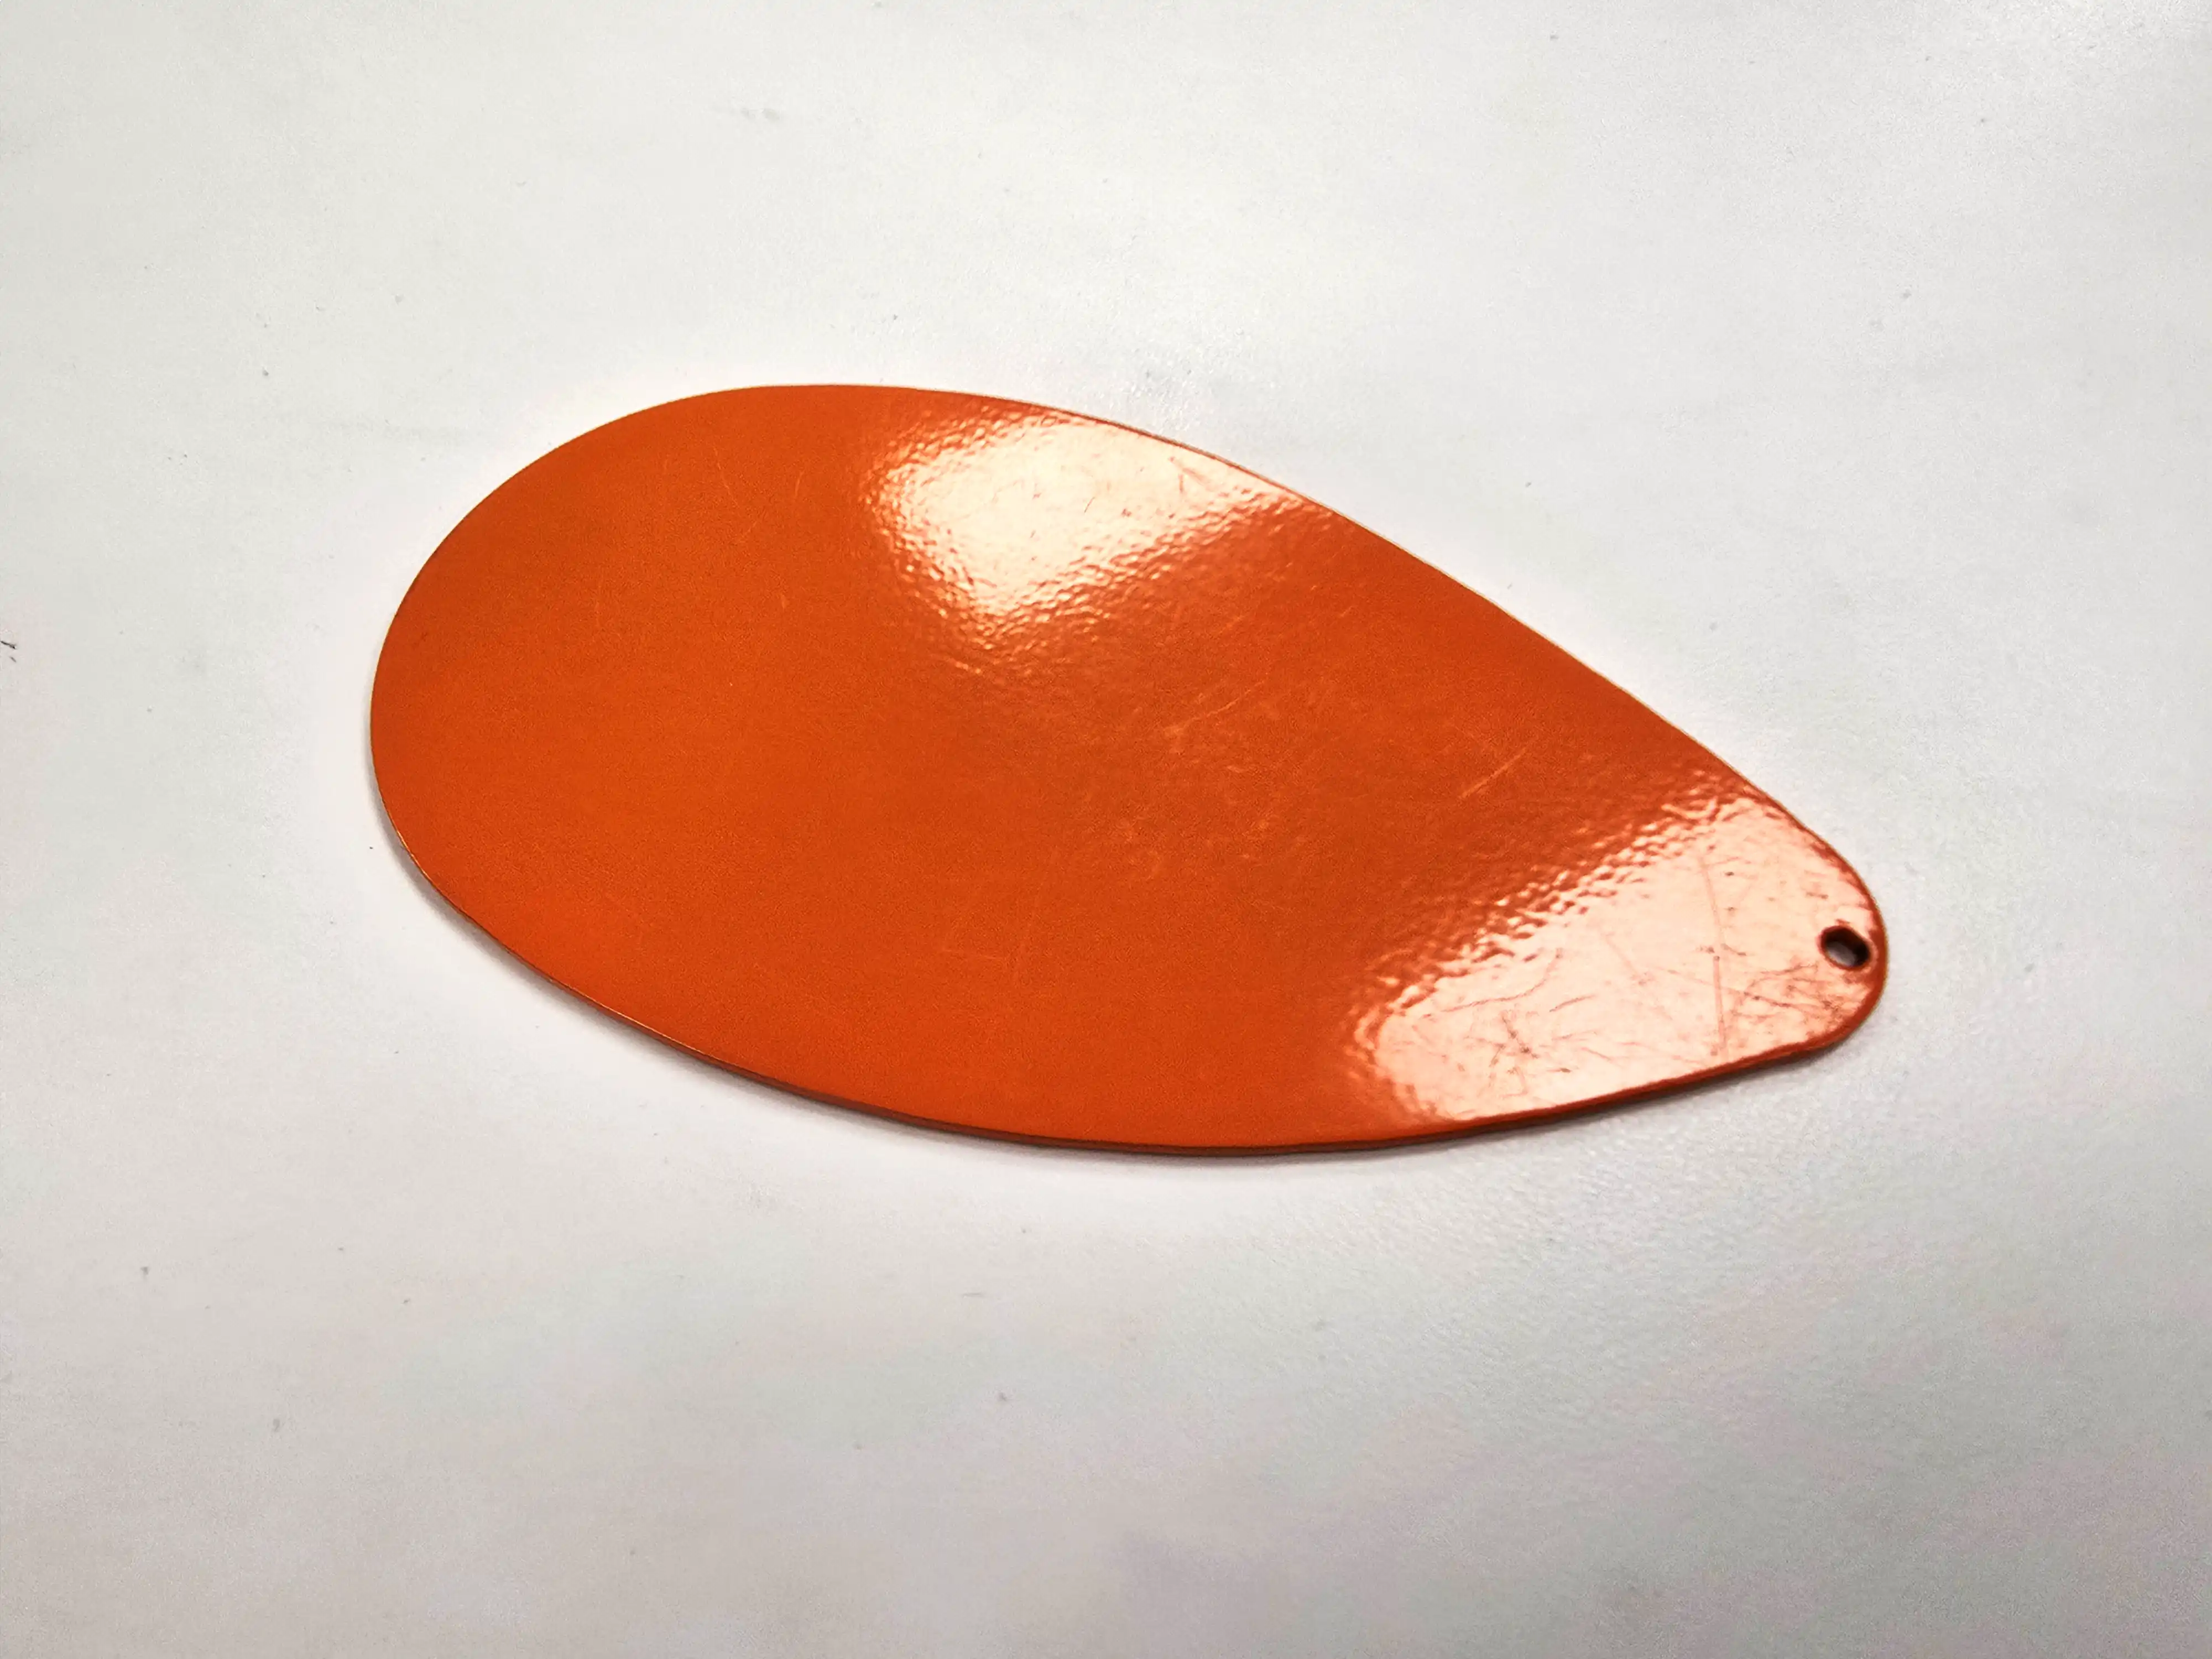
Bare steel teardrop part before powder coatingThe same part after powder coating in glossy orange

Best Practices for Success

Powder coating adds a thin layer of material to the surface of the part, typically around 2–4 mils in thickness. Designs should account for this added thickness in tight tolerances, threaded areas, or mating surfaces. Hanging points or contact areas may be required during coating, and deep recesses may experience reduced coating coverage.
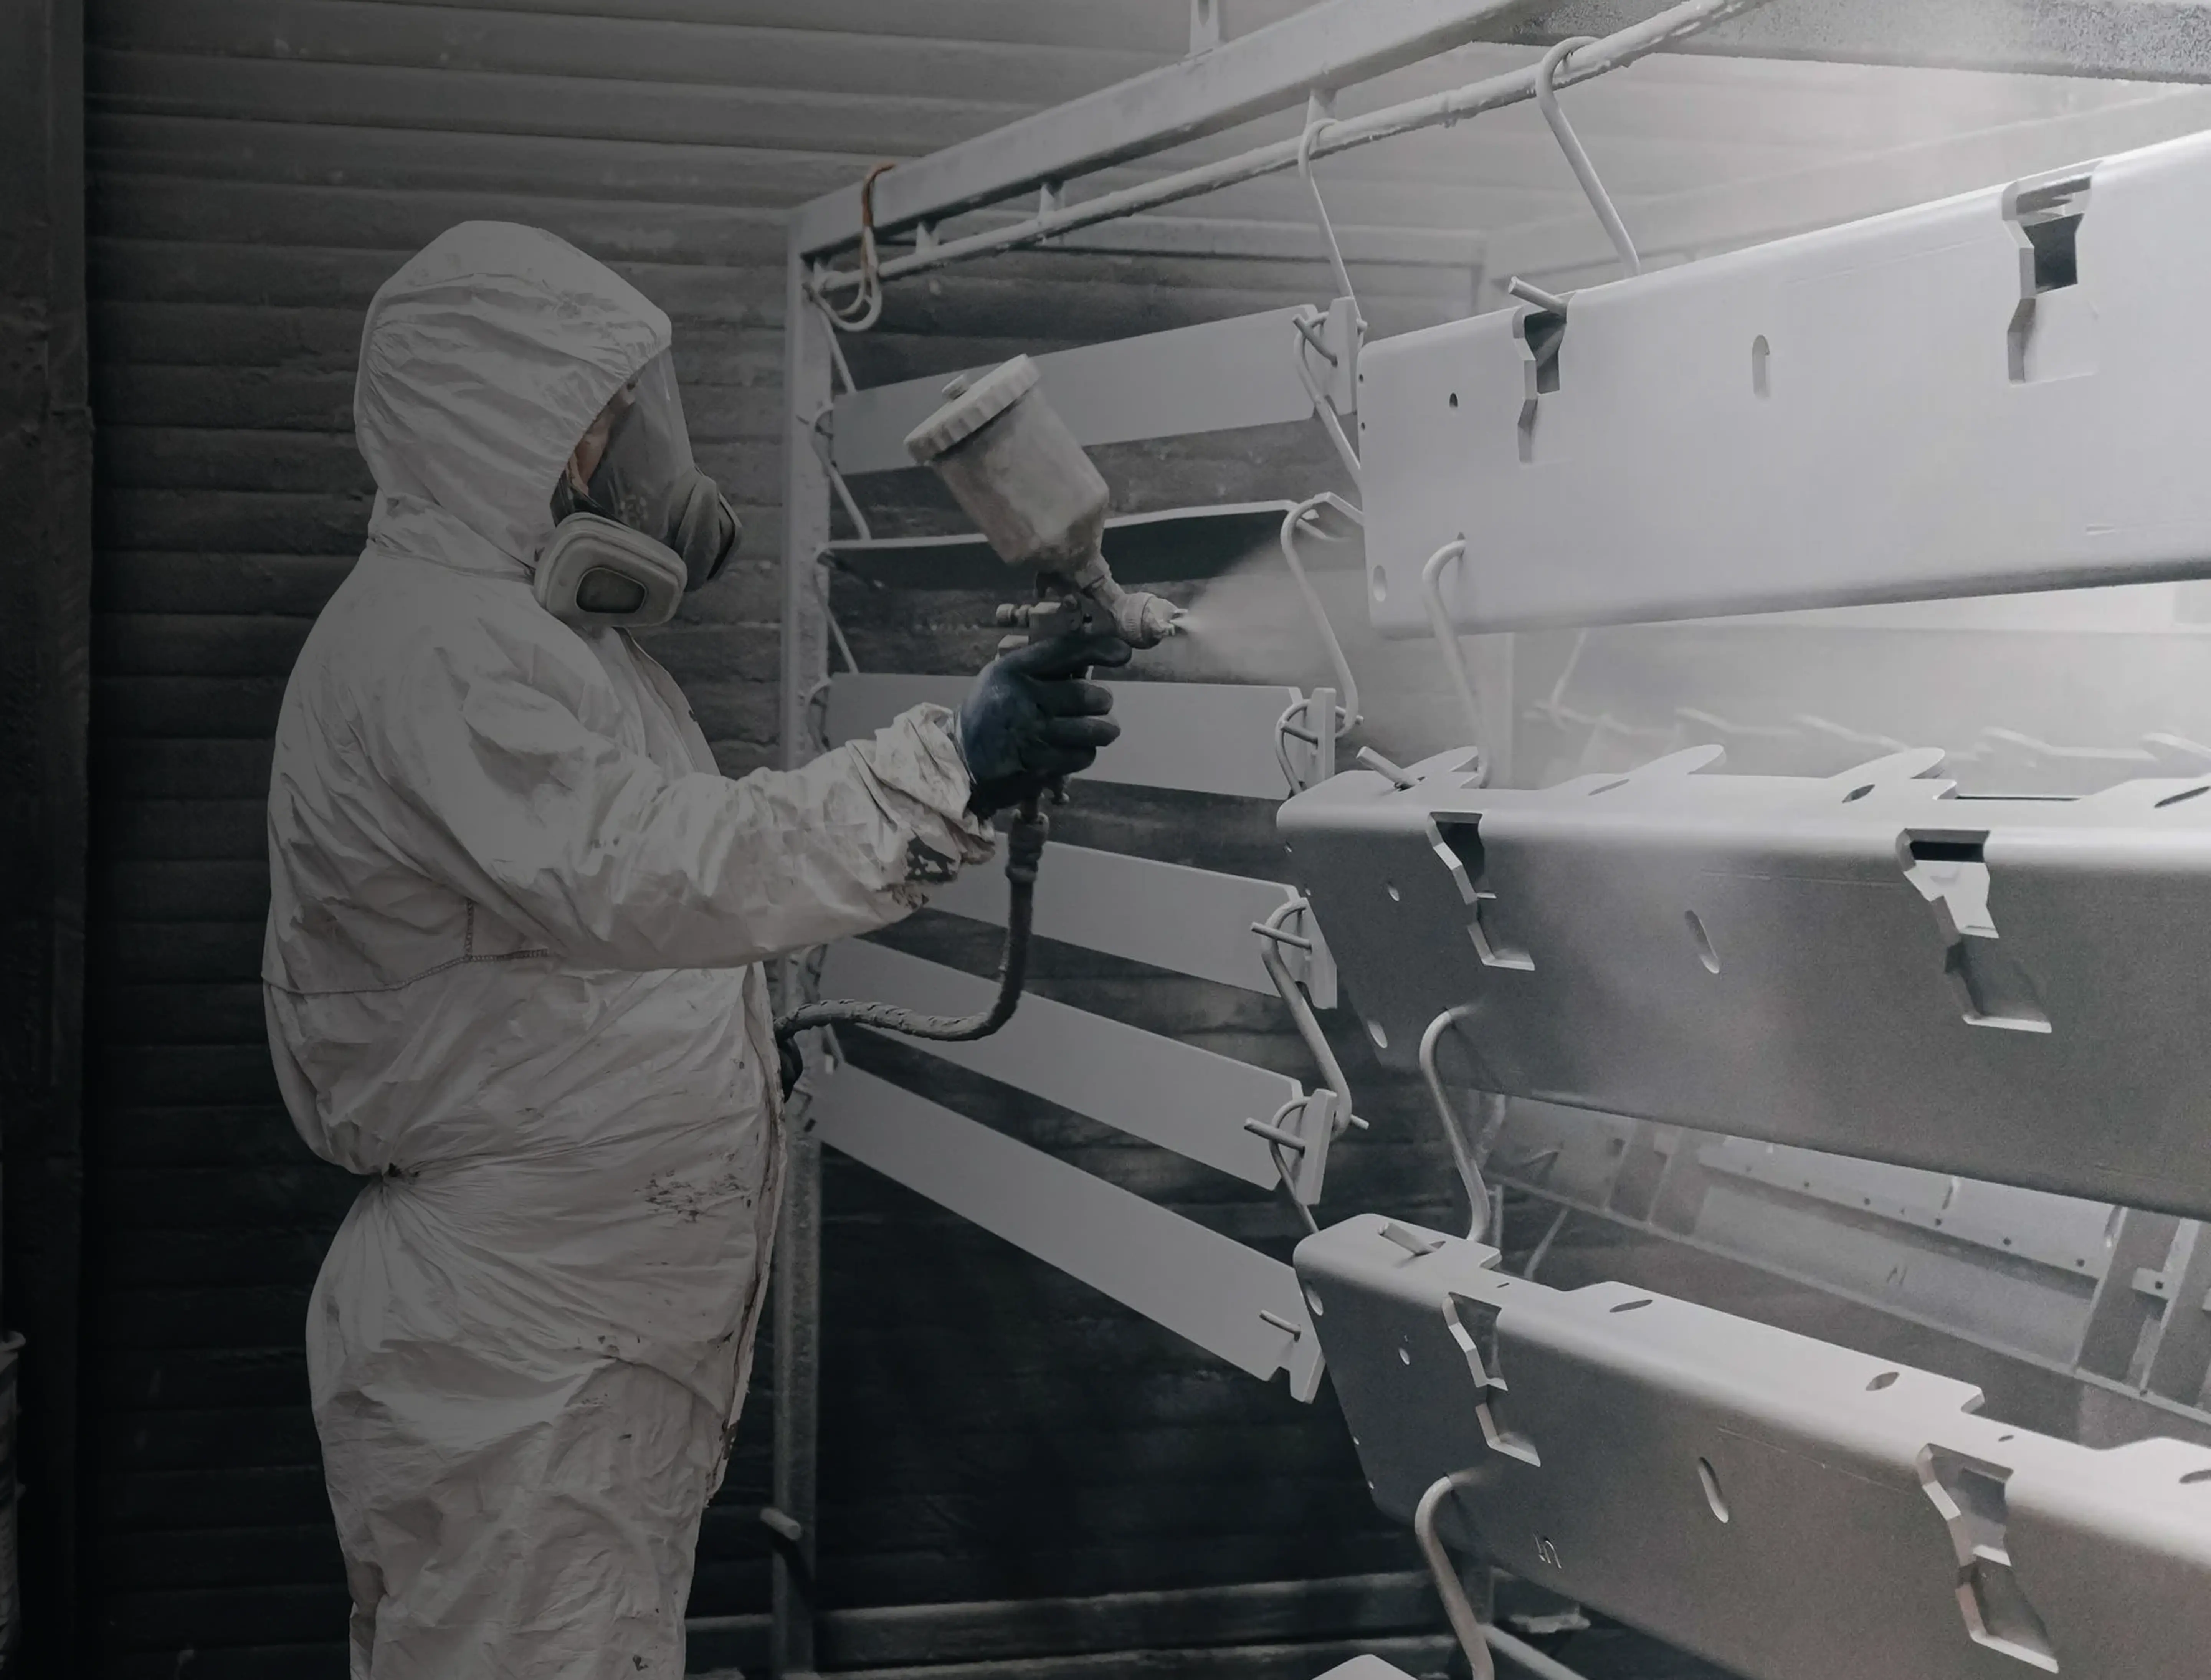
Worker in a protective suit spraying powder onto hanging metal parts

Centrifugal Tumbling

Tumbling places parts into a centrifugal barrel machine with abrasive media that smooths edges and refines the surface. This process reduces sharpness from cutting while giving parts a more uniform finish.
Tumbling, also known as centrifugal barrel finishing, uses abrasive media and high-speed rotation to smooth edges and lightly polish the surfaces of metal parts. As parts move against the media, small imperfections and rough edges from cutting are gradually softened. This process improves part feel, removes minor burrs, and creates a more consistent overall texture. Tumbling is commonly used for small to medium sized parts where improved edge quality and surface consistency are desired.
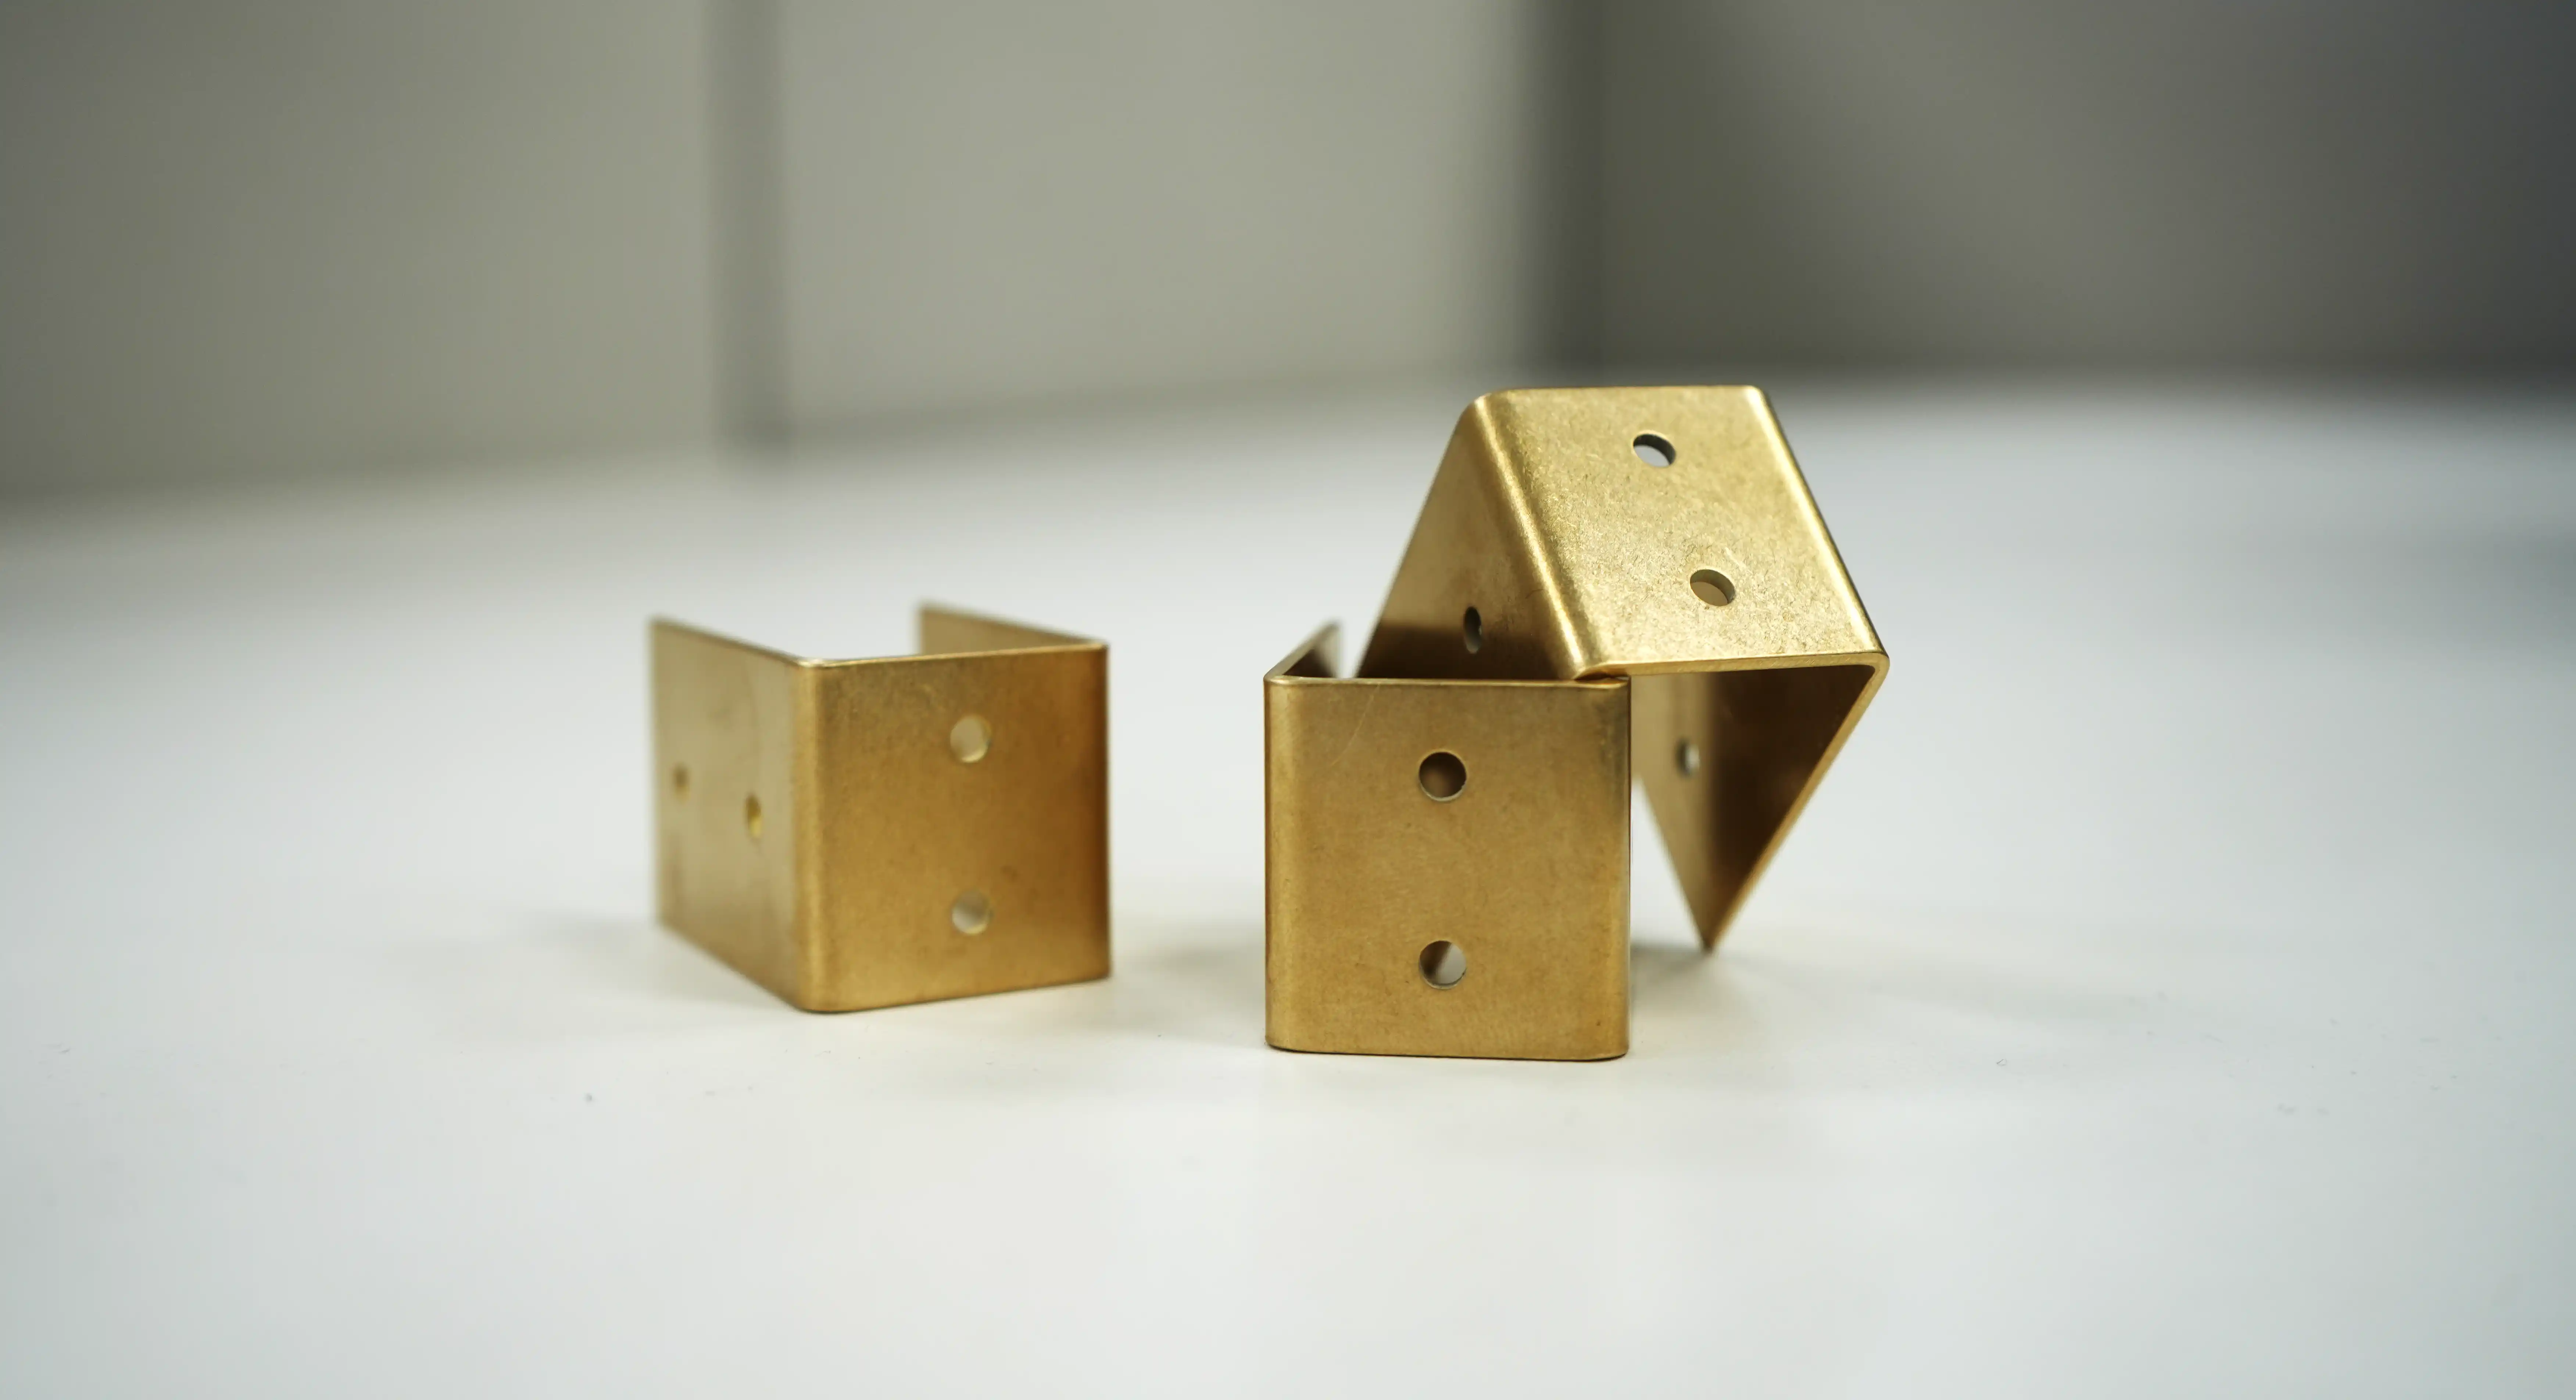
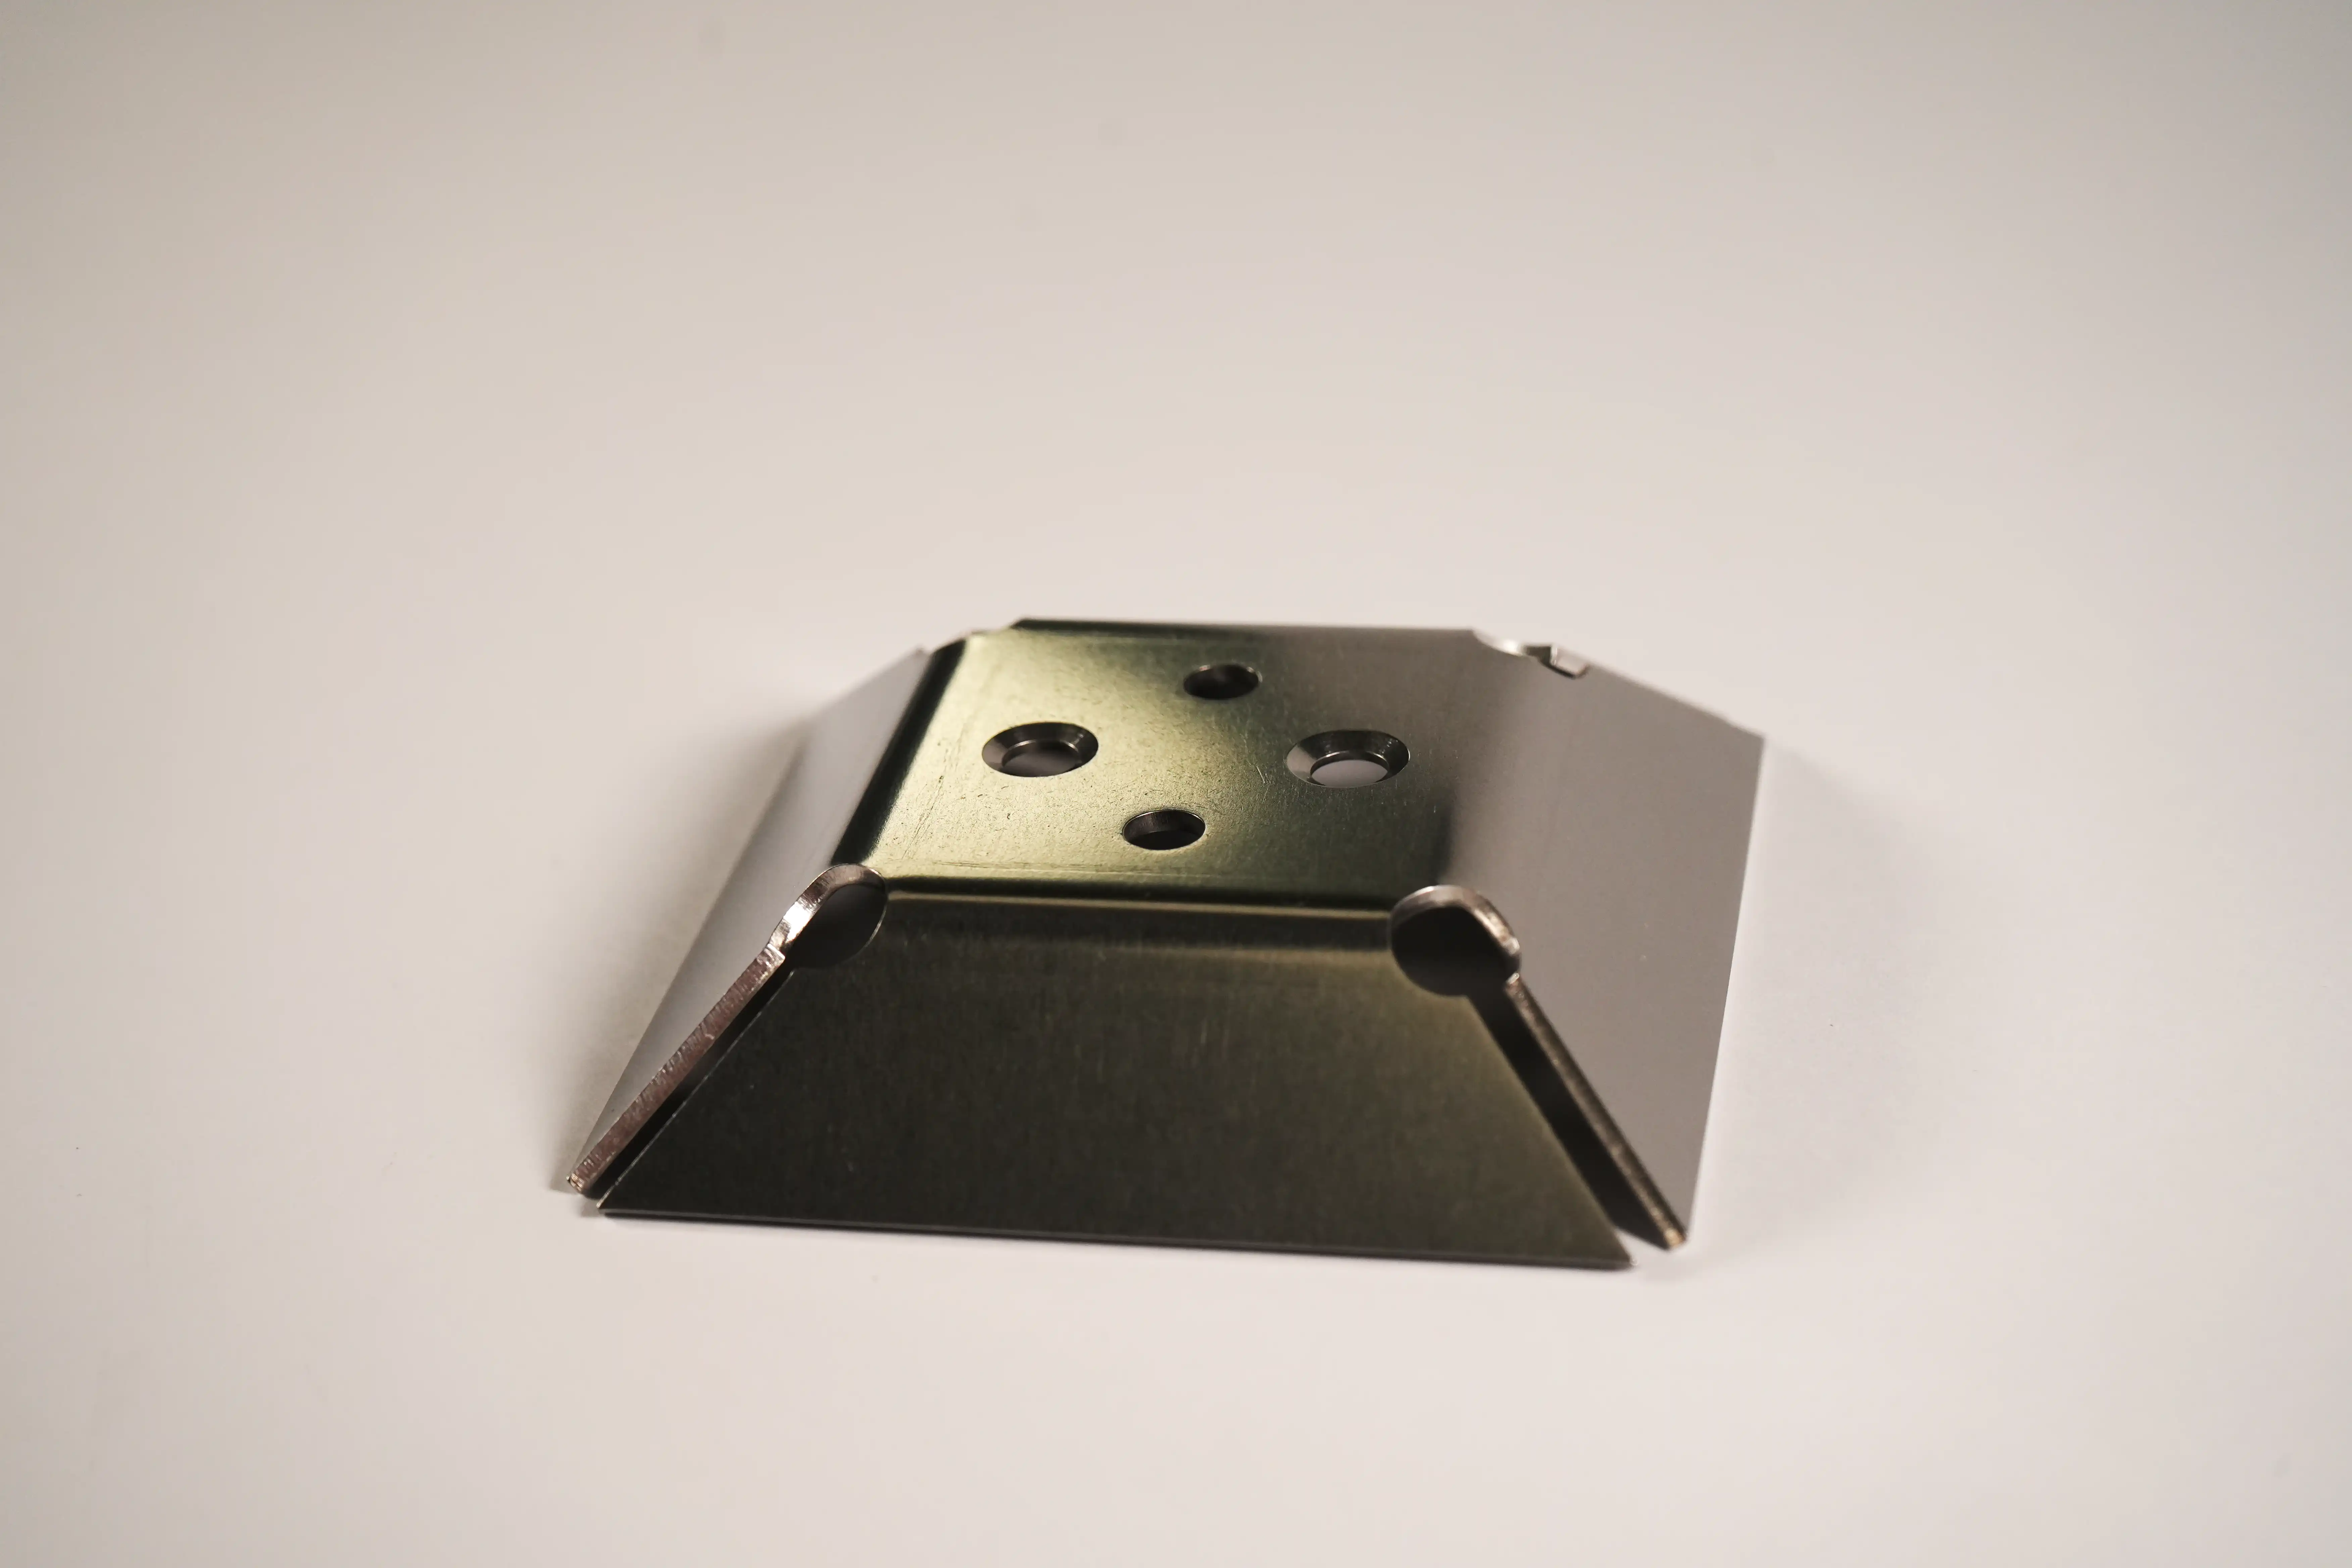
Tumbled sheet metal tray with countersunk holesTwo tumbled brass bracketsTeardrop-shaped part with a tumbled satin finish

Before and After

Before tumbling, laser cut parts typically have crisp edges and visible cutting marks along the surface. These edges can feel sharp and the surface may have slight discoloration from the cutting process. After tumbling, edges become smoother and slightly rounded while the surface texture appears more uniform. The result is a cleaner, more refined part that is easier and safer to handle.

Bent steel bracket before tumblingThe same bracket after tumbling, with smoother edges

Best Practices for Success

Tumbling works best for small to medium sized parts that can move freely within the finishing media. Very large parts or parts with extremely thin features may not be suitable. Deep pockets, tight internal corners, or very small holes may experience less finishing since the media cannot easily reach those areas.

Brass brackets in a bin of tumbling media